- 7 leading manufacturers
- 75 additional suppliers
- 32 states and provinces
- 16 related categories
- 3 guide sections
Overhead Conveyors Manufacturers and Companies
IQS Directory is a top industrial directory listing of leading industrial overhead conveyor manufacturers and suppliers. Access our comprehensive index to review and source overhead conveyor manufacturers with preview ads and detailed product descriptions. These overhead conveyor companies can design, engineer and manufacture overhead conveyors to your specifications and application need. A quick and easy to use request for quote form is provided for you to contact these overhead conveyor manufacturers and suppliers. Each company has detailed profile information, locations, phone number, website links, product videos and product information defined. We are the right resource for your information requirement whether its for a manufacturer of overhead conveyor systems, overhead chain conveyors, overhead track systems.
Suppliers located in MI, OH, ON +29 more states
Contents (5 sections)
Leading Overhead Conveyors Manufacturers
Showing all 7
| Placement No. | Manufacturer | Location | Contact | Actions | |
|---|---|---|---|---|---|
| 1 | Pack Air Inc.At Pack Air Inc., we help manufacturers design and build innovative custom conveyors in the United States and Canada. Our specialty resides in creating custom conveyor solutions and product handling devices that help solve conveying problems. We don’t try to force fit pre-made conveyors into a box. Rather, we let the box define the solution, and we design your conveyor to fit right the first time. | Neenah, WI | |||
| 2 | NED Conveyor DesignWe are NED Conveyor Design, and we specialize in designing, manufacturing, and supporting conveyor systems that keep materials moving efficiently through demanding industrial environments. Our work centers on building conveyor solutions that are engineered for reliability, accuracy, and long-term performance, whether the application involves bulk materials, unit handling, or process-driven production lines. | Newark, NJ | |||
| 3 | Dynamic Air Inc.Dynamic Air custom designs and manufactures a complete line of pneumatic conveying systems for dry bulk granular materials. Dynamic Air offers 16 different pneumatic conveying concepts, utilizing both pressure and vacuum, for handling a wide variety of dry bulk solids to provide a conveying solution that fits the process perfectly. Each system has its own unique set of operating characteristics for pressure, conveying line velocity, efficiency and performance. | St. Paul, MN | |||
| 4 | Whirl-Air-Flow CorporationWhirl-Air-Flow has been specializing in the design, development and fabrication of pneumatic conveying systems since 1946. Our vast experience in dense and dilute phase conveying systems spans across a broad range of industries. Whirl-Air-Flow has over 55 years of specializing in dense and dilute phase conveying systems, blending systems, bag unloading systems, central vacuum systems, process controls and air slides to name a few. | Princeton, MN | |||
| 5 | Vecoplan, LLCVecoplan leads the charge with cutting-edge technologies that revolutionize waste and recycling. From versatile shredders and granulators to efficient conveying and sorting systems, Vecoplan offers a wide array of solutions for handling wood, paper, plastics, textiles, and more. Our tailored equipment sets new industry standards, meeting the demands of even the most challenging applications. | Greensboro, NC | |||
| 6 | Conveyor Engineering & Mfg. Co.Since 1977, Conveyor Eng. & Mfg. has been a leader in the manufacture of stainless steel screw conveyors and conveyor components (bearings, flighting, hangers, screws, troughs, etc.). We serve a wide variety of industries including wet corn milling, food, sugar, ethanol and chemical. Contact us to learn more about our conveyor systems. We are available to answer any of your questions, feel free to call us today! | Cedar Rapids, IA | |||
| 7 | Akona Process SolutionsAt Akona Process Solutions, we take pride in designing and manufacturing conveyor systems that bring efficiency, reliability, and innovation to material handling. Our team understands the importance of precision, durability, and streamlined operation, so we engineer our conveyors to meet the diverse needs of industries ranging from manufacturing and processing to packaging and distribution. | Monroe, NC |
Claim your Page One Spot
Leading overhead conveyors manufacturers are listed first on this page, each with a website preview and a Request a Quote button on its row.
Additional Overhead Conveyors Companies
The category’s other overhead conveyors companies are listed on their own page, with location, phone and website where each supplier provides them.
View 75 Additional Overhead Conveyors CompaniesDo not see your company listed in Overhead Conveyors?
Engineers and buyers use this page to find overhead conveyors suppliers. Add your company to the Overhead Conveyors listings so they can find you too.
List Your Company- Listed in the Overhead Conveyors directory
- A profile page for your company
- Buyers contact you directly
Overhead Conveyors Industrial Manufacturing Guides
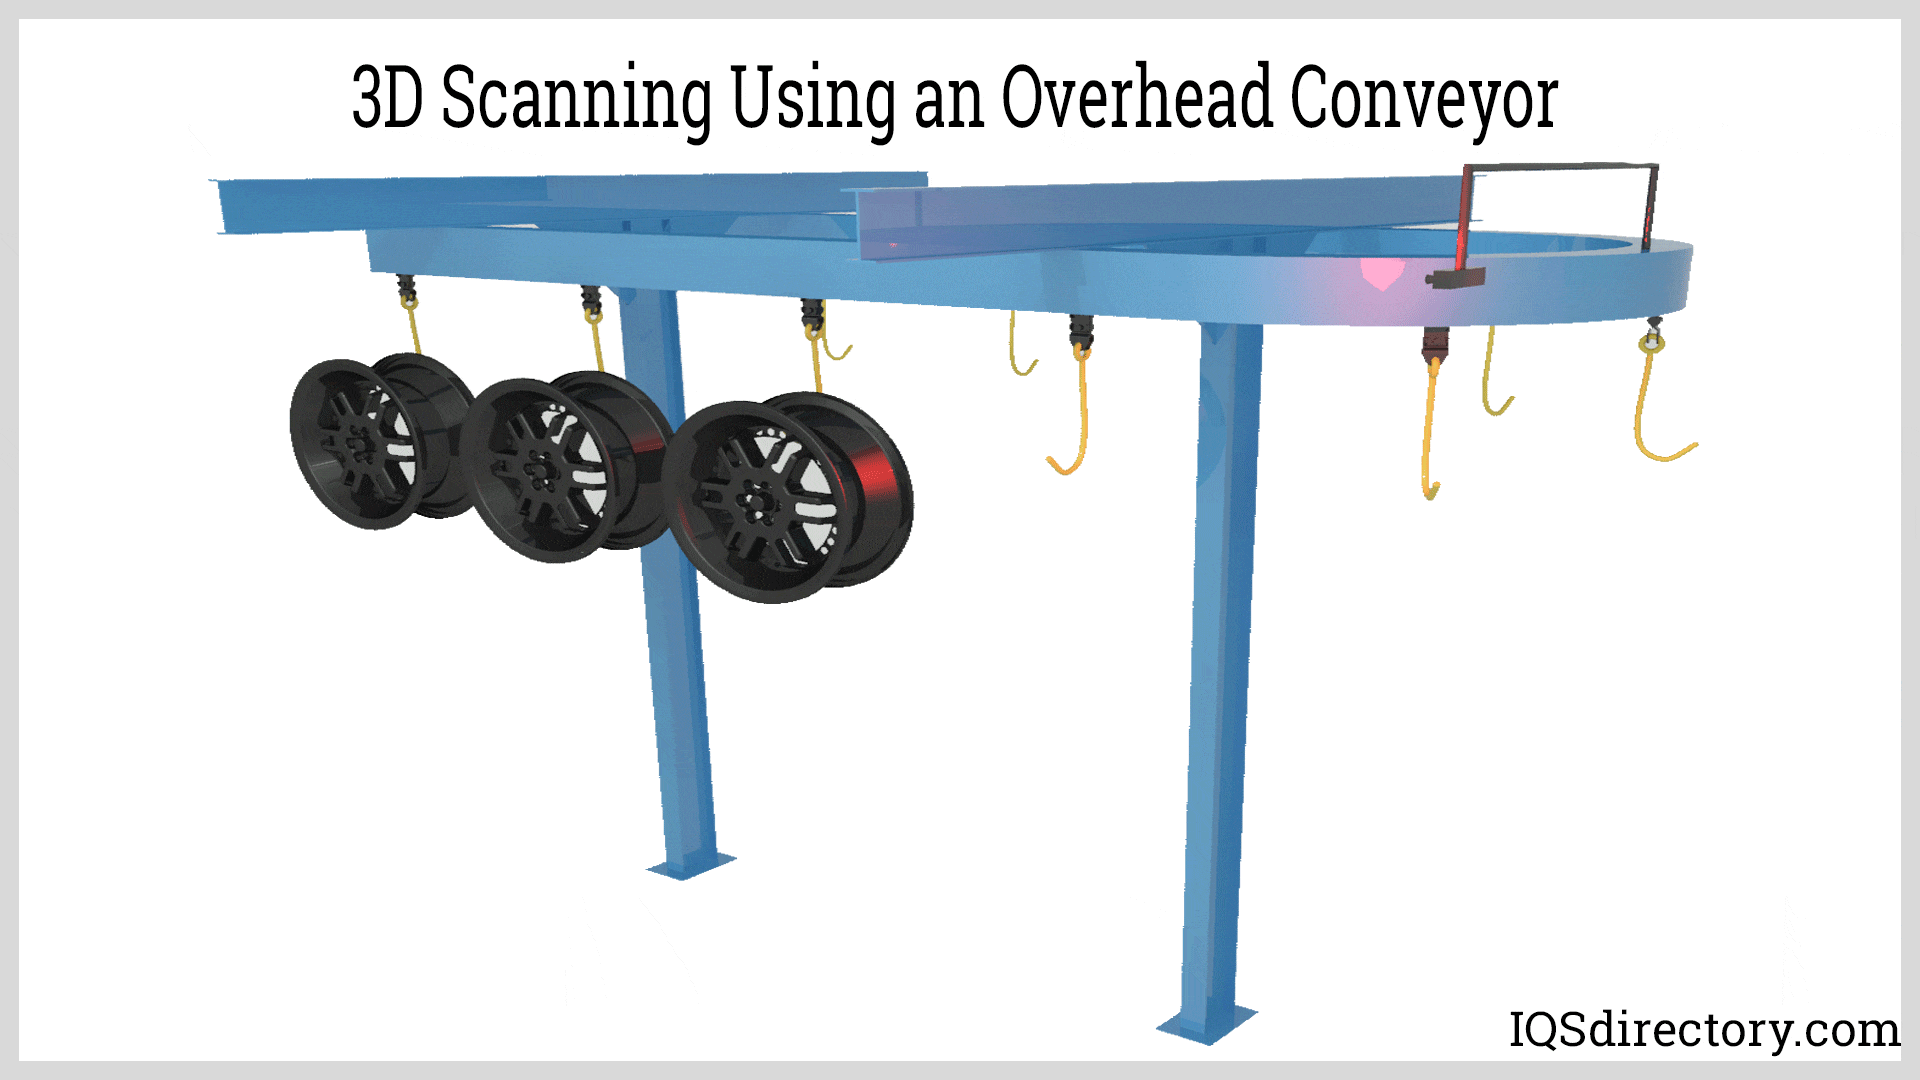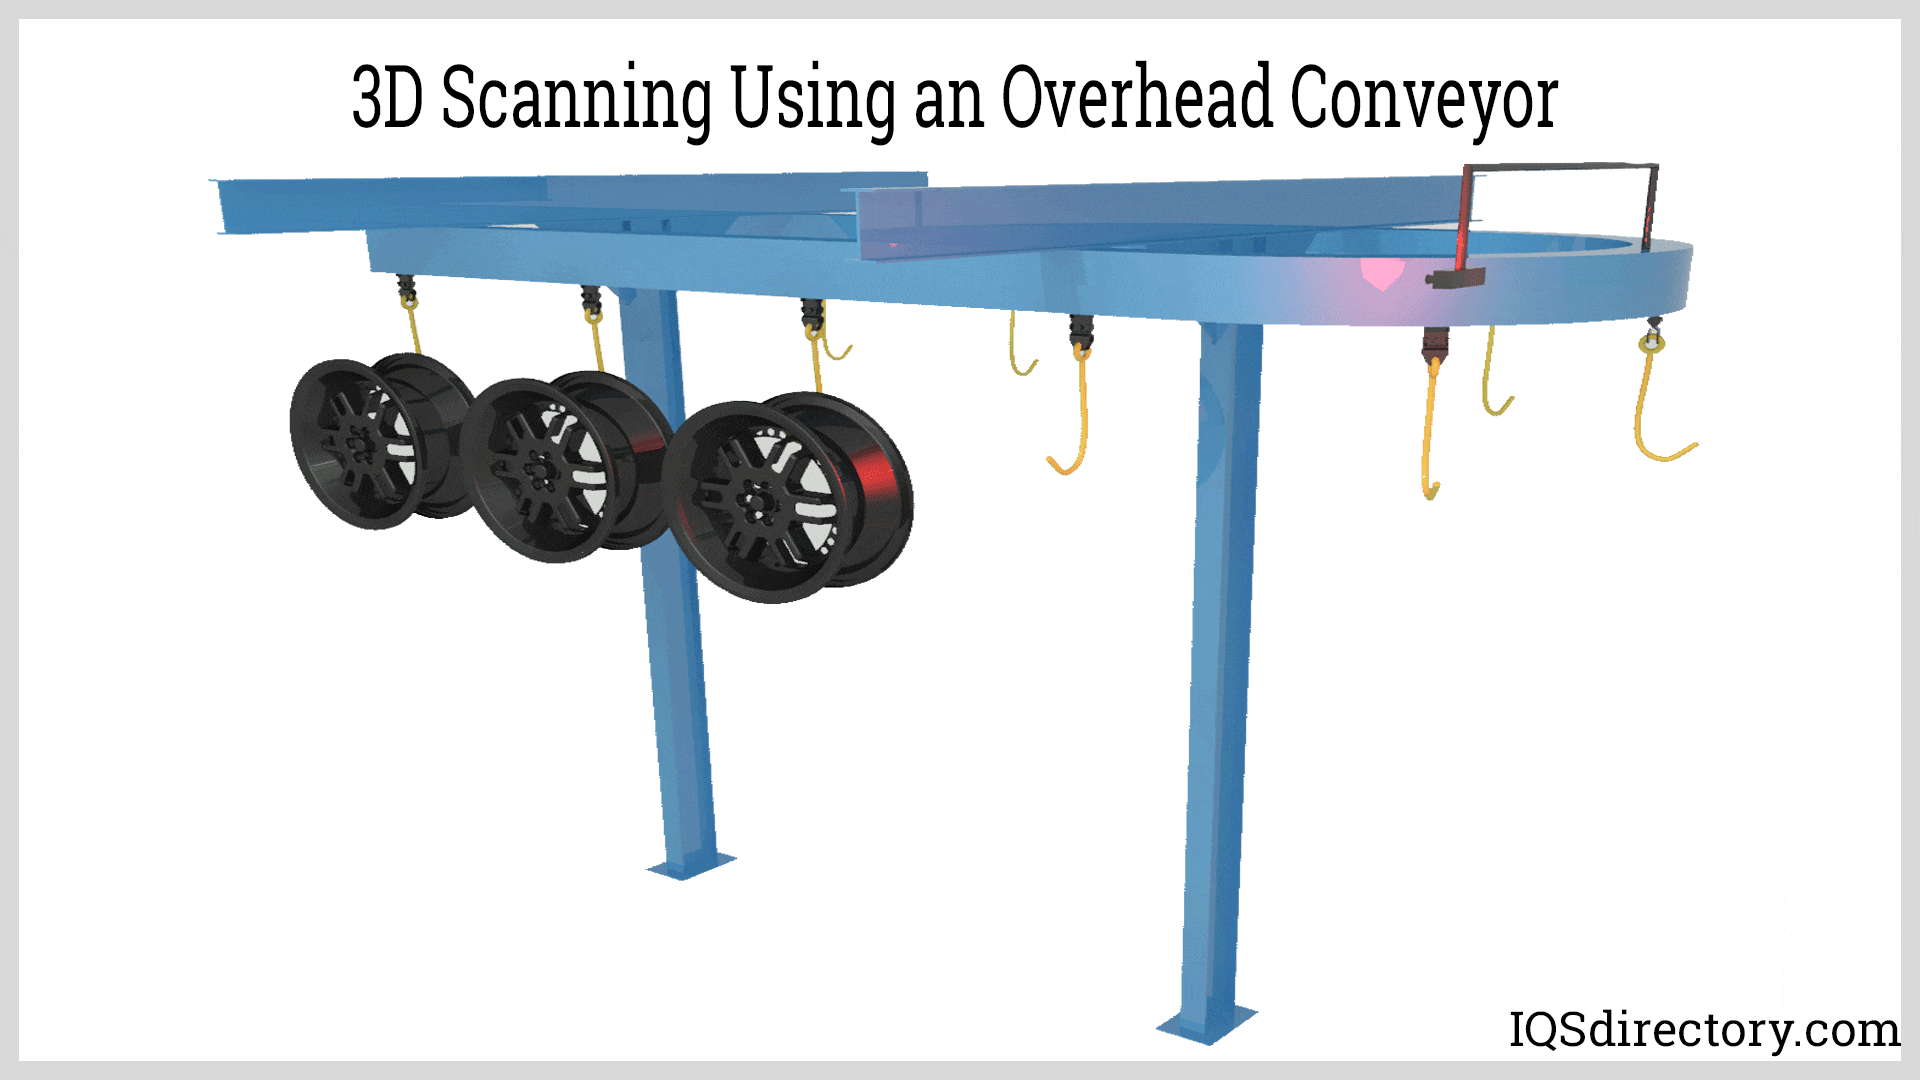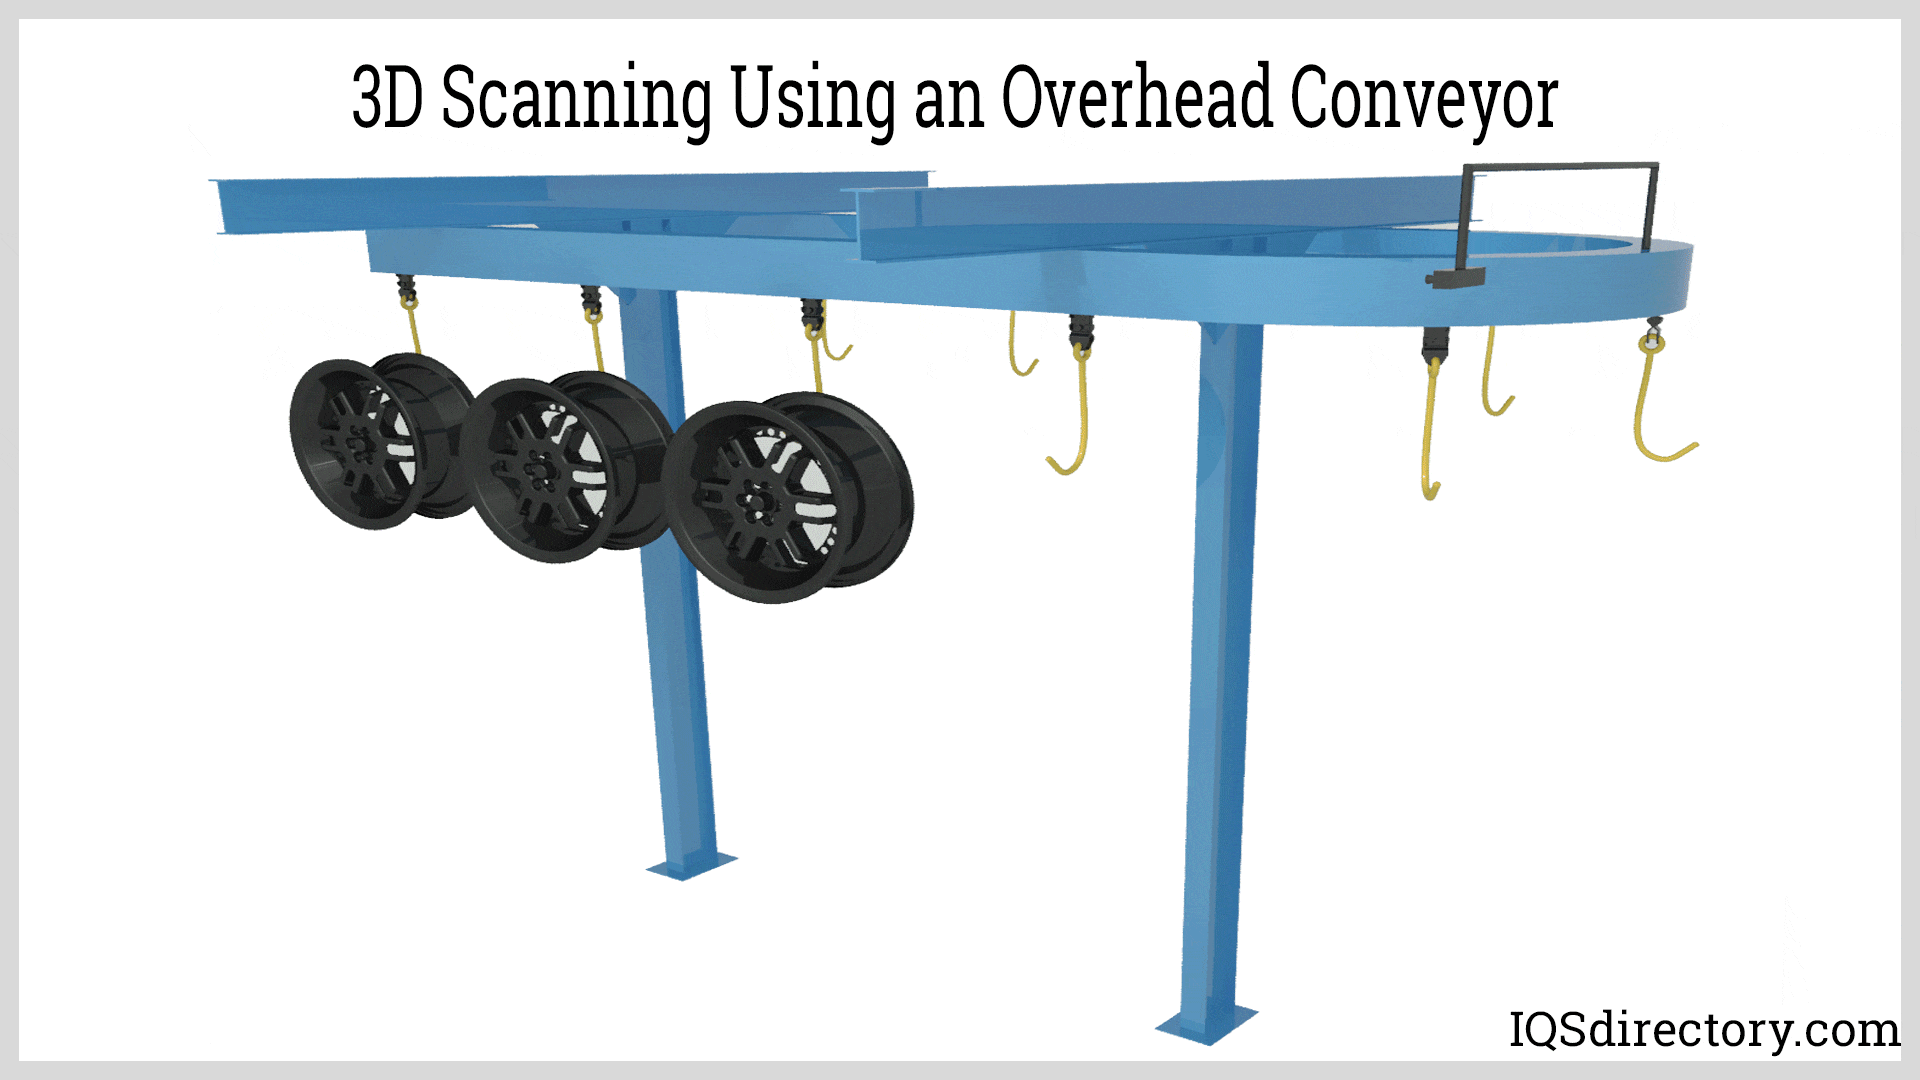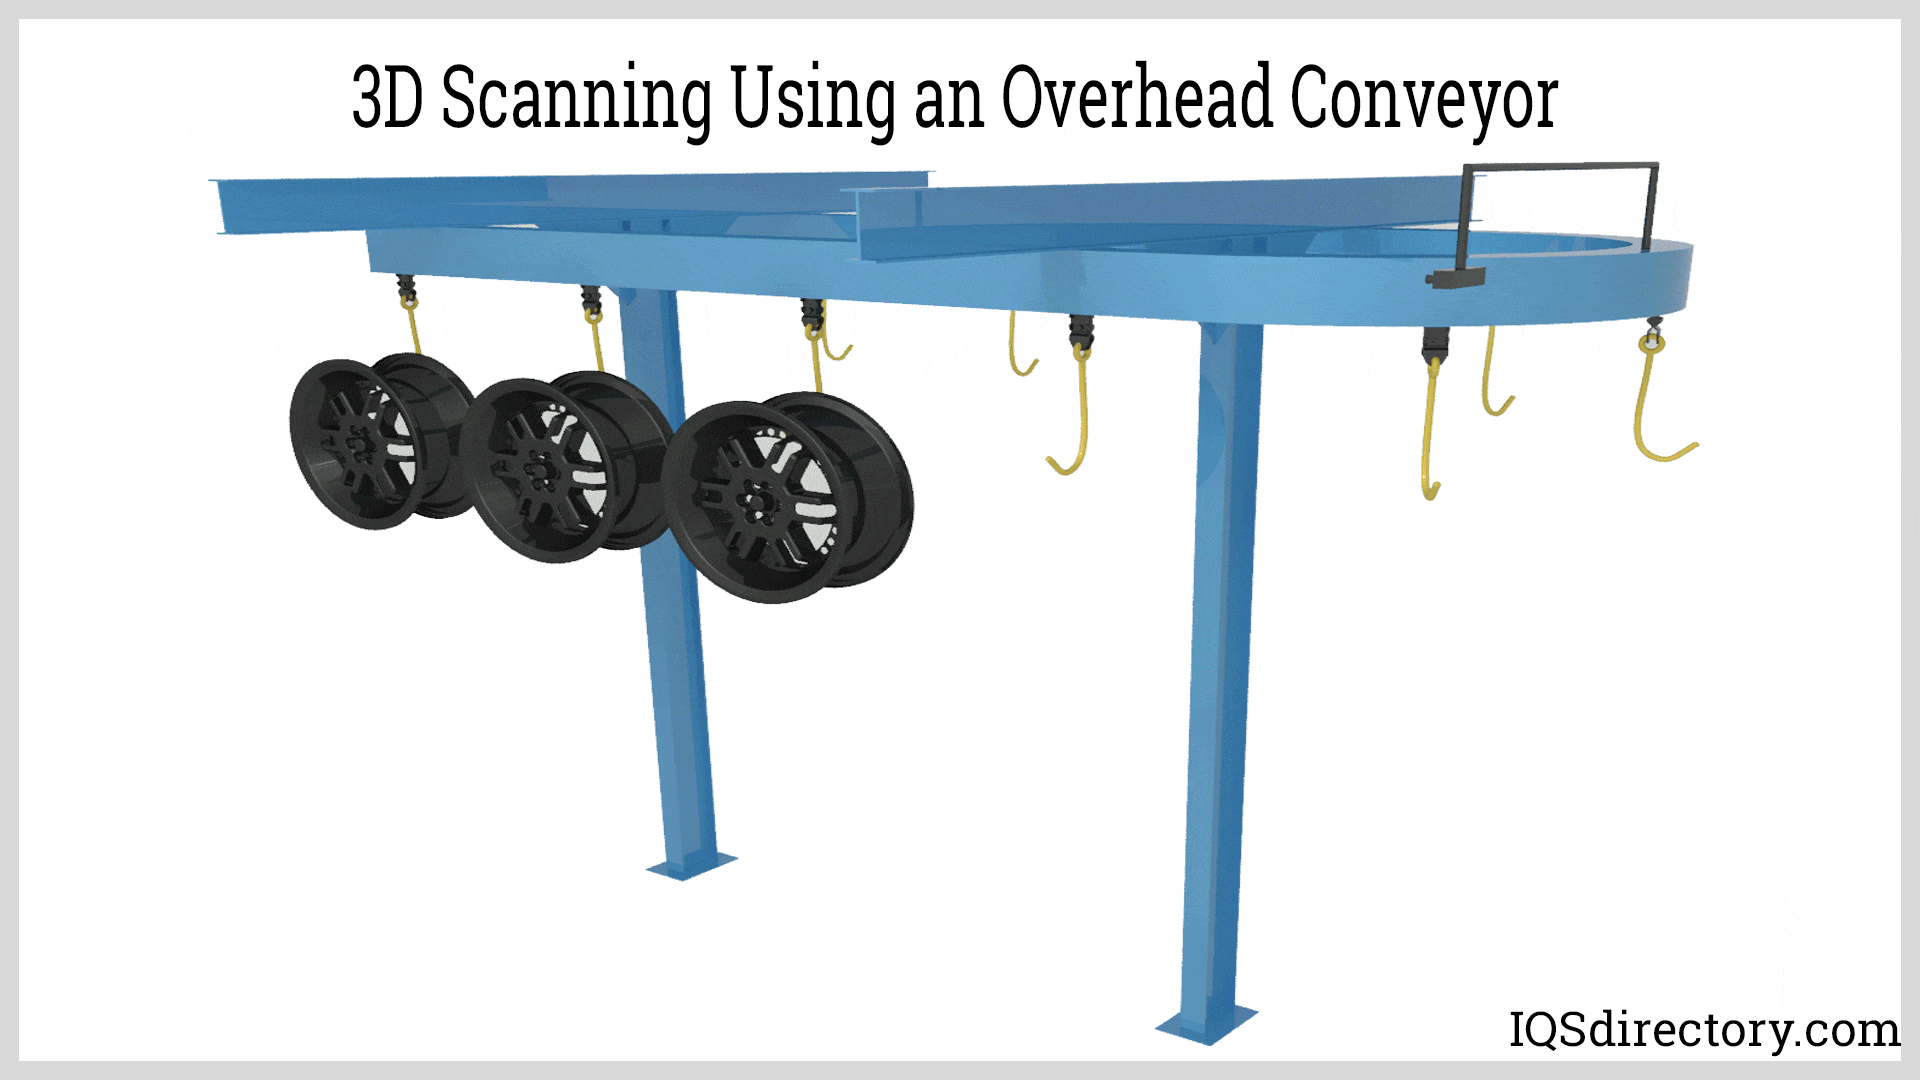
Overhead Conveyors: Types, Applications and Benefits
The content of this article contains everything you need to know about overhead conveyors and their use. You will learn: What is an Overhead Conveyor? Types of…
6 chapters
Quick Answers
- How many overhead conveyors manufacturers are listed on IQS Directory?
- 7 leading manufacturers and 75 additional suppliers.
- Where are overhead conveyors manufacturers located?
- The listed suppliers are in 32 states and provinces: Michigan (9), Ohio (6), Ontario (5), Georgia (4), Illinois (4), North Carolina (4), Texas (4), Virginia (4), and 24 more.
- How do I get quotes from overhead conveyors suppliers?
- Select suppliers in the table and choose Request Quotes. IQS reviews your request and forwards it to every supplier you select.
Overhead Conveyors
Overhead conveyors are material handling equipment used in moving products, parts, packages, foods or equipment from one place inside a facility to another, or through various stages of automated manufacturing or finishing. Used to maximize floor space and save labor expense, overhead conveyors have three main types that are commonly used in manufacturing and distribution: automated electric monorail conveyors, enclosed track overhead conveyors and overhead chain conveyors.
Overhead Conveyor Design
Overhead chain conveyors have a conveyor frame that can have an enclosed tubular track, I-beam monorail, I-beam twin rail with trolleys or load bars with carriers. These can be powered manually or electrically. Most overhead conveyors have hooks in order to suspend the items being transported and operate on an endless loop for continuous product or material movement. Modern overhead conveyor systems are equipped not only to move parts across horizontal and vertical distances, but also to curve, divert, lift and sort products and packages as part of complete automated systems. These types of advanced conveying processes are done by brushes, magnets, automated levers, rails and even simple gravity.
Types of Overhead Conveyors
Overhead conveyor system tracks can be supported by ceilings, walls or floors using floor stands or racks. Overhead conveyors can be non-powered and driven by either manual or gravitational forces or they can be powered and driven by a load-carrying mechanism such as an electric motor, center drive, air pressure or vacuum. Monorail conveyors have a conveyor frame consisting of an I-beam monorail and trolleys with load bars or carriers that are powered by a power driven chain and are used to move products or materials along the rail. Enclosed track overhead conveyors have a conveyor frame consisting of a tubular enclosed track or "load bars", on which trolleys move products or materials along.
Applications for Overhead Conveyors
Overhead conveyor manufacturers are creating innovative solutions to new manufacturing challenges every day. For instance, packaging industries have designed overhead conveyor systems pre-programmed to sort specific boxes into separate chutes, and in the retail industry, sophisticated, computer-controlled overhead conveyor systems are now being put to use for garment movement. Used for applications such as assembly automation, warehousing, distribution, paint finishing, creative retail designs and complex production, overhead conveyors ensure that the product or material is less likely to get damaged than conventional floor conveyors. Industries that benefit from overhead conveyors include automotive, leather, paper, food processing, garment, pharmaceutical, material handling and industrial manufacturing.
Overhead Conveyor Informational Video