- 5 leading manufacturers
- 38 additional suppliers
- 25 states and provinces
- 10 related categories
- 10 guide sections
Machine Vision Manufacturers and Suppliers

IQS Directory implements a thorough list of industrial machine vision manufacturers and suppliers. Utilize our listing to examine and sort top industrial machine vision manufacturers with previews of ads and detailed descriptions of each product. Any industrial machine vision company can design, engineer, and manufacture industrial machine vision systems to meet your companies specific qualifications. An easy connection to reach industrial machine vision companies through our fast request for quote form is provided on our website. The company information includes website links, company profile, locations, phone, product videos and product information. This source is right for you whether it's for a manufacturer of industrial machine visions, machine vision inspections, and machine vision systems.
Suppliers located in MI, OH, CA +22 more states
Contents (6 sections)
Leading Machine Vision Manufacturers
Showing all 5
| Placement No. | Manufacturer | Location | Contact | Actions | |
|---|---|---|---|---|---|
| 1 | Cincinnati Automation Ltd.When it comes to machine vision systems, we have the tools to get the job done right. We work hard to provide the best solutions and products to meet our customers’ demand. It is our goal to work with you from start to finish on all aspects of design and production. We will do our best to provide the solution to even your most challenging requirements. Find out more by contacting us today! | Florence, KY | |||
| 2 | XIMEA GmbHWe are XIMEA, a machine vision technology company focused on developing advanced camera solutions for industrial imaging, automation, scientific research, and inspection environments. Our company provides high-performance machine vision cameras designed to capture accurate image data at high speeds while supporting compact system integration. | Not listed | |||
| 3 | Mitutoyo CorporationAt Mitutoyo Corporation, we provide precision measurement technologies designed to support dimensional inspection, quality control, and automated manufacturing environments. Our company offers advanced machine vision systems that enable fast, accurate, non-contact measurement of components with complex geometries, small features, and demanding tolerances. | Aurora, IL | |||
| 4 | Hexagon Manufacturing IntelligenceAt Hexagon Manufacturing Intelligence, we provide advanced machine vision systems and precision manufacturing technologies designed to help manufacturers improve quality, productivity, and process control. Our company develops solutions that support automated inspection, dimensional measurement, defect detection, part verification, and production monitoring. | North Kingstown, RI | |||
| 5 | ISRA Vision Systems Inc.ISRA manufactures machine vision systems — robot vision, surface vision and quality-control vision inspection systems. Robot vision can be 2D-6D; surface vision inspects complex surfaces; quality vision will perform bead application, assembly, code ID and completeness inspections. We also produce software modules. | Plymouth, MI |
Claim your Page One Spot
Leading machine vision manufacturers are listed first on this page, each with a website preview and a Request a Quote button on its row.
Additional Machine Vision Companies
The category’s other machine vision companies are listed on their own page, with location, phone and website where each supplier provides them.
View 38 Additional Machine Vision CompaniesDo not see your company listed in Machine Vision?
Engineers and buyers use this page to find machine vision suppliers. Add your company to the Machine Vision listings so they can find you too.
List Your Company- Listed in the Machine Vision directory
- A profile page for your company
- Buyers contact you directly
Machine Vision Industrial Manufacturing Guides

Machine Vision Systems: Types, Functions and Applications
This article takes an in-depth look at machine vision systems. Read further and learn more about: What are machine vision systems? Components of machine vision…
7 chapters, the longest in this category
Quick Answers
- How many machine vision manufacturers are listed on IQS Directory?
- 5 leading manufacturers and 38 additional suppliers.
- Where are machine vision manufacturers located?
- The listed suppliers are in 25 states and provinces: Michigan (6), Ohio (4), California (3), Illinois (3), Florida (2), Massachusetts (2), Minnesota (2), New York (2), and 17 more. 1 supplier does not list a location.
- How do I get quotes from machine vision suppliers?
- Select suppliers in the table and choose Request Quotes. IQS reviews your request and forwards it to every supplier you select.
Machine Vision
Machine vision systems are advanced industrial imaging solutions designed to simulate selected functions of human sight with far greater speed and consistency in repetitive environments. In manufacturing, packaging, robotics, and automated inspection settings, machine vision (MV) refers to computer-based visual inspection, identification, measurement, and process control used to monitor production quality and guide equipment. Within systems engineering, machine vision is usually treated as a practical automation technology, while computer vision is more often discussed as a broader computer science field focused on image interpretation.
The History of Machine Vision Systems
The evolution of machine vision systems reaches back to the 1950s, when psychologist James J. Gibson introduced the concept of optical flow and helped shape the way motion and visual information could be analyzed. Building on that foundation, early researchers developed two-dimensional imaging methods that relied on statistical pattern recognition. In 1960, Larry Roberts at MIT completed a PhD thesis focused on extracting 3D geometric information from 2D images, helping inspire broader research into automated image analysis and 3D machine imaging.
During the 1970s, MIT continued to influence the field by offering a machine vision course within its Artificial Intelligence Lab, where attention was given to practical image interpretation tasks such as edge detection and object analysis. In 1978, David Marr introduced an influential framework for computer vision that moved from a 2D sketch toward a 3D understanding of a scene. That work helped define how vision systems could interpret shapes, surfaces, and spatial relationships in more useful ways.
By the 1980s, machine vision moved beyond laboratories and into industrial manufacturing, where vision systems were used to read numbers, letters, symbols, and barcodes on products and packaging. The decade also brought the first smart cameras, making it easier to combine image capture and processing in one compact unit. In the 1990s, digital signal processing expanded those capabilities further, opening the door to faster image analysis, lower system costs, and wider adoption across quality control, assembly verification, and automated inspection applications.
Today, machine vision systems are used worldwide in factories, warehouses, laboratories, and logistics operations, and the market continues to expand as automation investments increase. Earlier industry forecasts placed the global machine vision market at roughly $15.46 billion by 2022, with Asia Pacific holding a large share, followed by Europe and North America. That growth reflects ongoing demand for automated inspection, robotic guidance, product traceability, and tighter manufacturing consistency.
Benefits of Machine Vision Systems
Machine vision systems offer a wide range of advantages for manufacturers, processors, and automated equipment users. They reduce the variation associated with manual inspection, identify flaws or subtle details that operators may overlook, and sort products far faster than labor-intensive methods. Their flexibility also allows one platform to support inspection, identification, measurement, and verification tasks. In addition, machine vision systems generate usable digital data that can be stored, reviewed, trended, and transferred for deeper analysis, process improvement, and documentation.
How Machine Vision Works
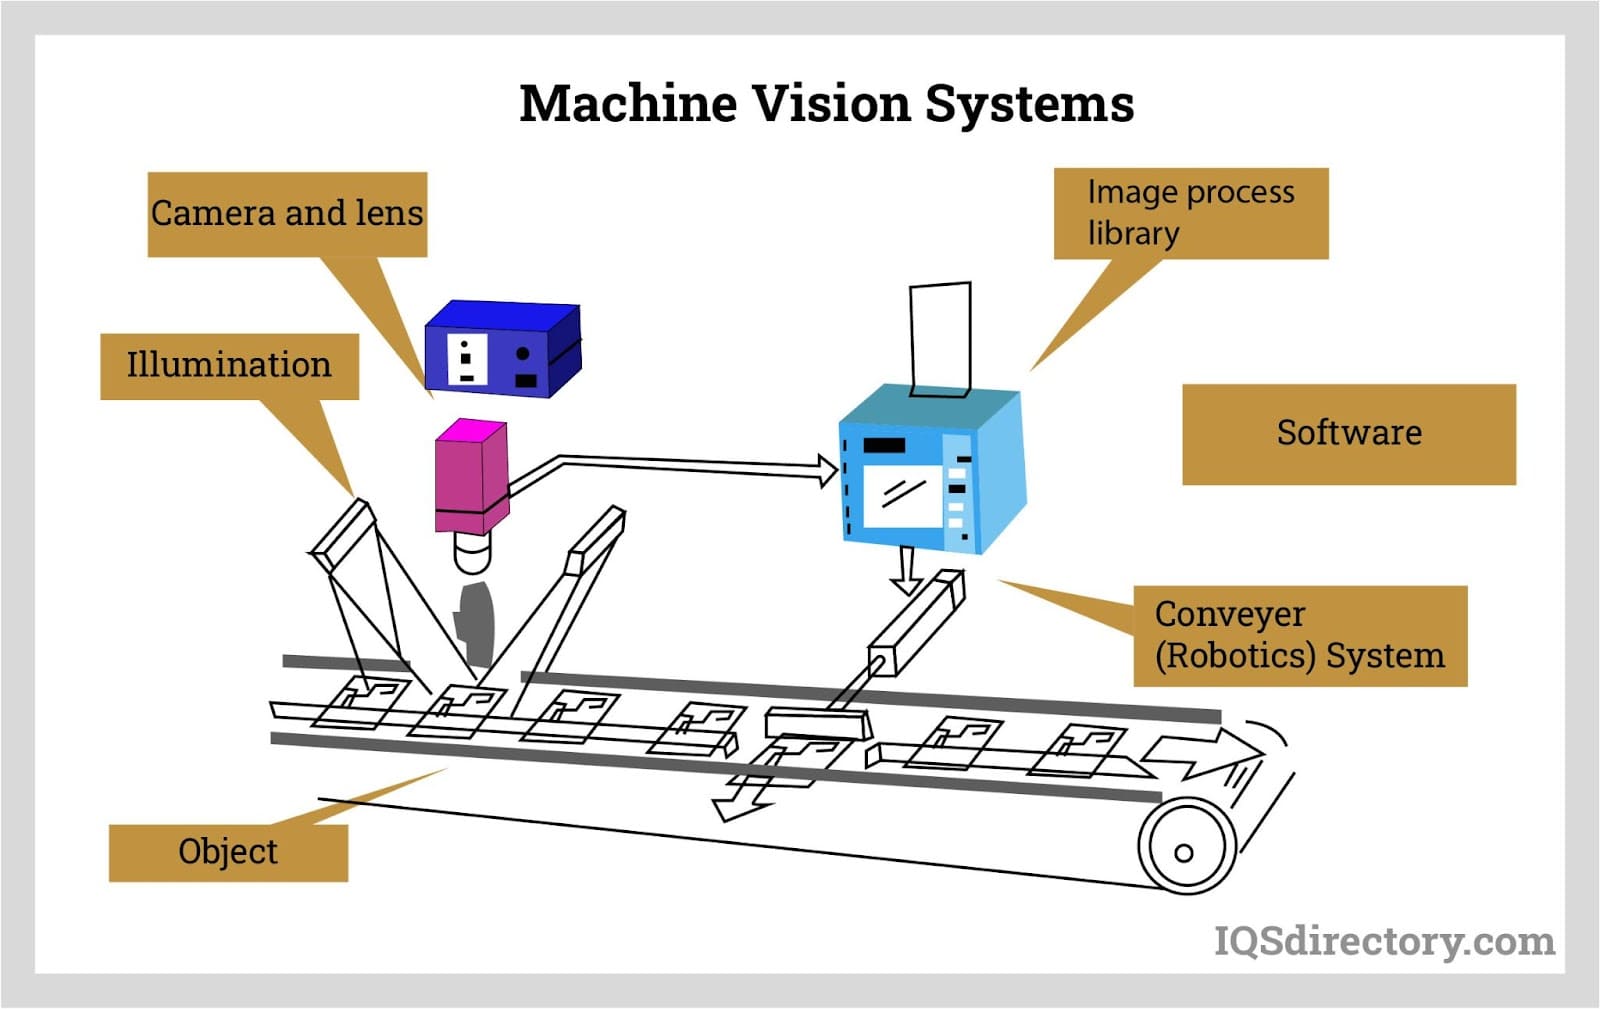
Machine vision works by combining controlled lighting, optics, digital cameras, triggering, and pattern recognition software to capture images and turn them into decisions. Although machine vision technology has advanced dramatically, most systems are still designed around repeatable inspection or guidance tasks where the viewing conditions, part orientation, and decision rules can be defined in advance. That is why machine vision performs so well in industrial automation, in-line inspection, and quality assurance environments.
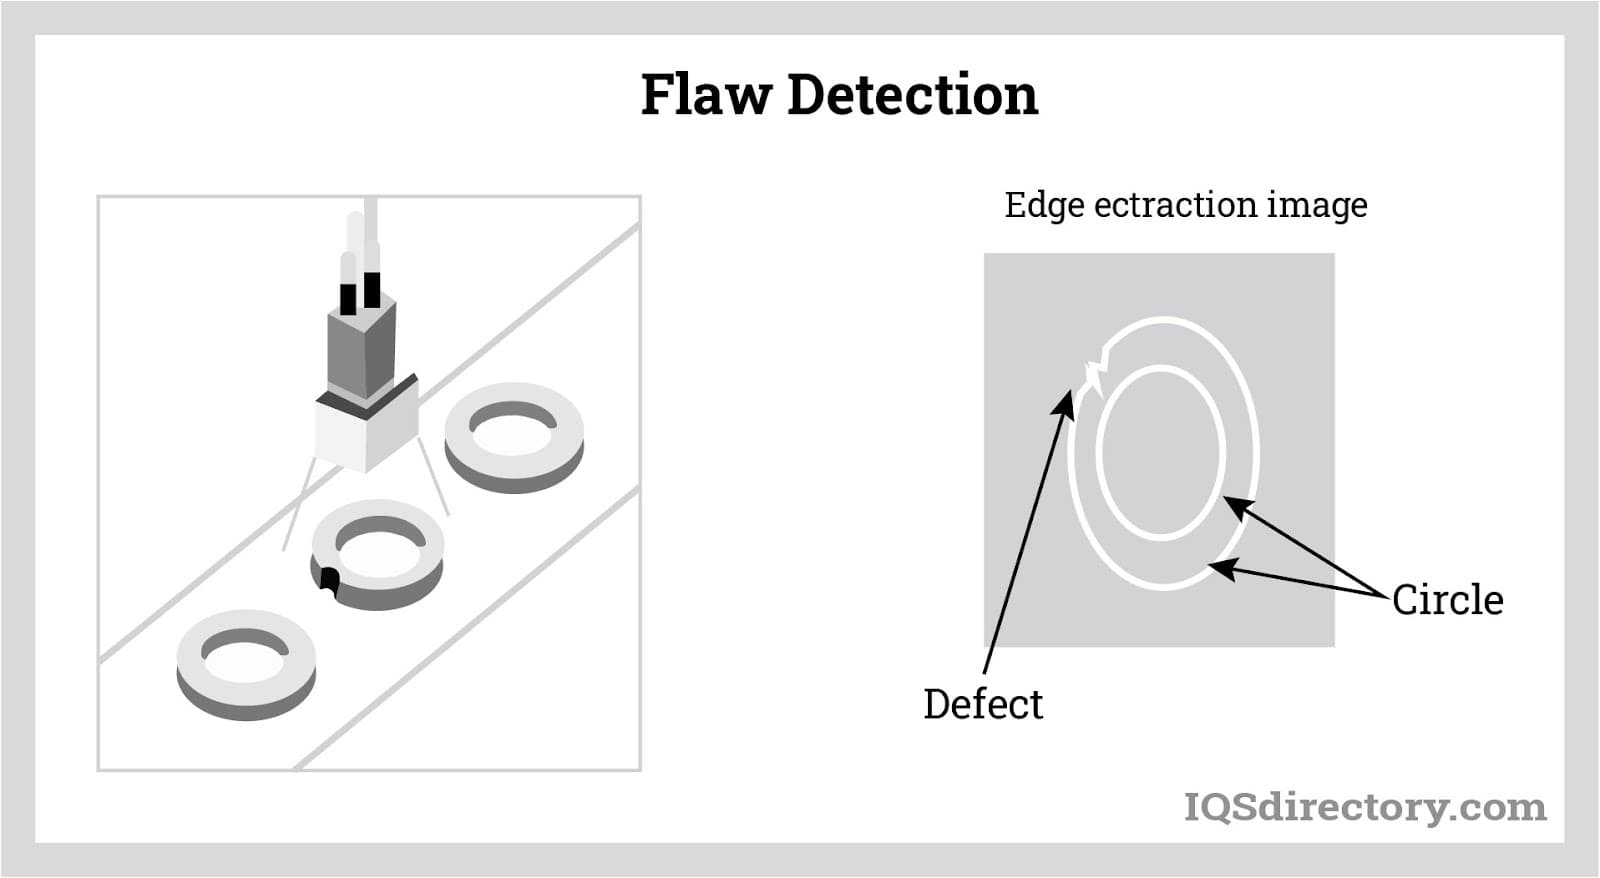
These systems process images through methods such as thresholding, stitching, pixel counting, filtering, color analysis, segmentation, blob detection and extraction, edge detection, pattern recognition, barcode reading, neural network or deep learning, optical character recognition, and metrology or gauging. In many applications, several of these tools are used in sequence so the system can isolate a feature, inspect it, compare it to a reference, and return a reliable result that supports sorting, measurement, or pass-fail inspection.
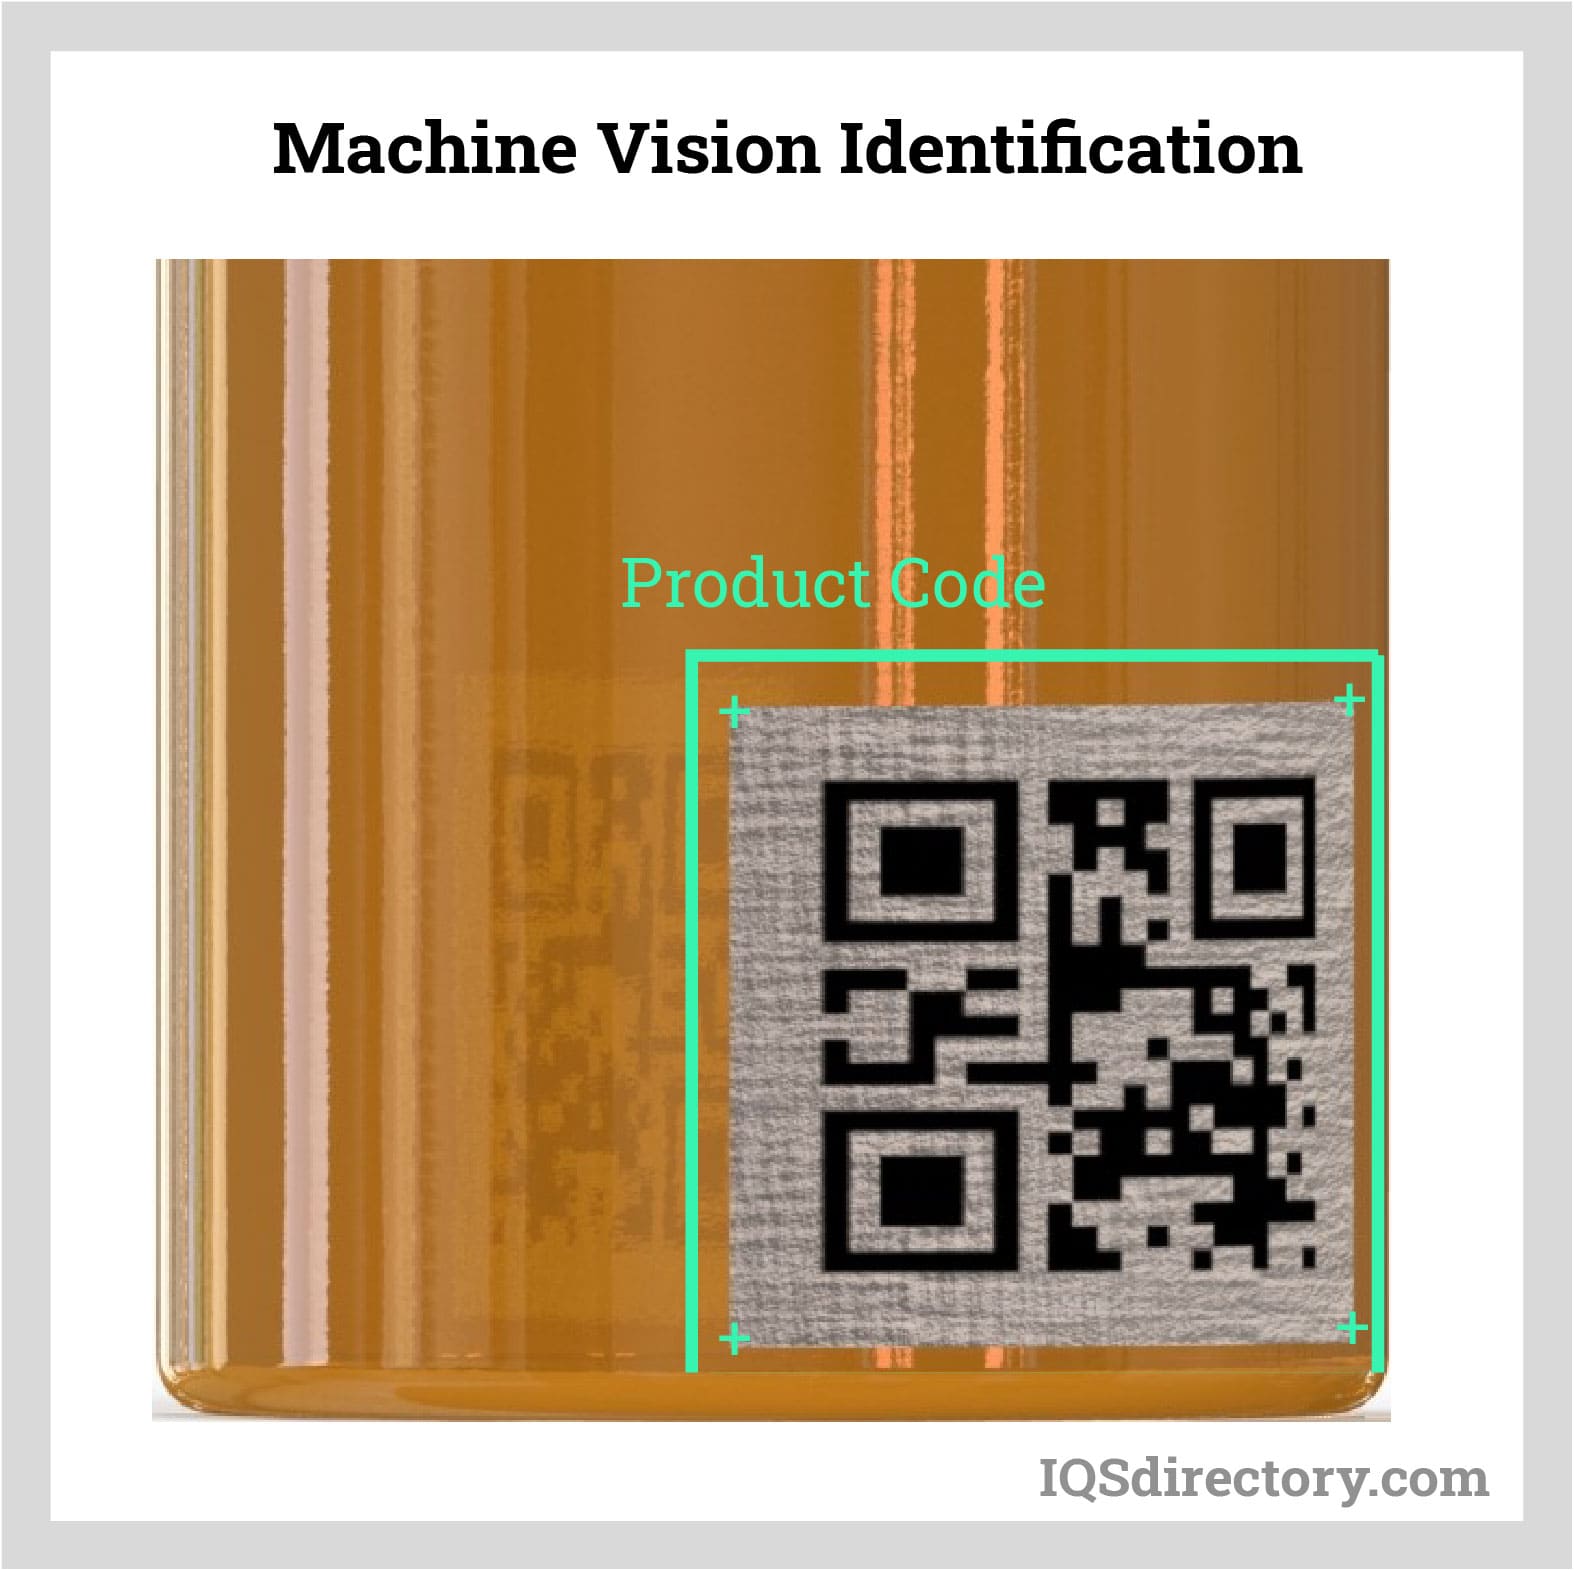
Thresholding A technique that applies a selected gray value to separate one region of an image from another. Thresholding is often used to convert portions of an image to black or white so edges, marks, holes, labels, or part features can be isolated for inspection. Stitching Also called registration, this method combines adjacent 2D or 3D images into one composite image. It is useful when a field of view is too large for a single capture or when detailed inspection requires several overlapping images. Pixel Counting A process in which the system counts dark or light pixels within a defined area. Because pixels are the smallest units in a digital image, counting them can help determine fill level, surface coverage, presence or absence, or the size of a selected feature. Morphological Filtering Morphological filtering uses lattice-based image operations to clean up and analyze digital images. It can remove noise, close gaps, emphasize shapes, and improve feature extraction before the system moves on to measurement, comparison, or defect detection. Color Analysis This process uses color information to isolate features, assess quality, and identify specific items, products, coatings, or parts within an image. Color analysis is often used when grayscale inspection alone cannot separate a target from its background. Segmentation Process Segmentation divides a digital image into multiple regions or segments, making it easier to analyze objects, boundaries, textures, or surfaces. It is a common step in machine vision workflows that require object identification, counting, or dimensional analysis. Blob Detection Blob detection and extraction identify connected regions in an image that differ from their surroundings, such as a dark flaw on a lighter surface. These regions, called blobs, are useful for presence-absence checks, particle inspection, contamination screening, and shape analysis. Edge Detection A method that locates and defines object boundaries within an image. Edge detection helps a machine vision system outline shapes, measure distances, verify alignment, and determine whether a component matches the required profile. Pattern Recognition Pattern recognition software identifies, matches, or counts known shapes or image features, even when they are rotated, partially hidden, or presented at varying sizes. This method is widely used in assembly verification, part location, and automated inspection. Barcode Reading The machine vision system scans barcodes or 2D codes and compares the captured information to stored reference values or expected formats. This supports traceability, inventory movement, product authentication, and code verification on high-speed production lines. Neural Net Neural networks and deep learning systems learn to identify visual patterns and make more complex classification decisions as they process new data. These tools are especially helpful when a rule-based approach is too rigid for natural variation in parts, surfaces, or image conditions. Optical Character Recognition An automated method for reading printed or marked text within images, such as serial numbers, lot codes, expiration dates, and product identifiers. OCR improves traceability and supports verification without requiring manual data entry. Metrology or Gauging The accurate measurement of object dimensions, such as length, width, diameter, gap, or height, in units like millimeters, inches, or pixels. Gauging is widely used when manufacturers need non-contact measurement for tolerance checks and dimensional verification.Machine Vision Images, Diagrams and Visual Concepts
Machine Vision Types
Machine Vision Applications
The main purpose of machine vision is to deliver image-based information that can be used to analyze products, surfaces, assemblies, or production conditions. Machine vision applications include automation process control, quality screening, automated inspection, robotic guidance, integrated systems, and the manufacture of both hardware and software used along assembly lines. Buyers often search for machine vision when they need faster inspection, tighter tolerances, better traceability, or a more repeatable way to verify product quality.
Machine vision is used throughout assembly lines for measurement, counting, inspection, and reading serial numbers on items such as die casted products. It has taken over many repetitive and error-prone visual tasks once handled manually and plays a major role in automation environments where a robot arm or AGV needs dependable visual guidance. It is also widely used in packaging, food processing, electronics, medical device manufacturing, and automotive production.
Machine Vision Equipment Components
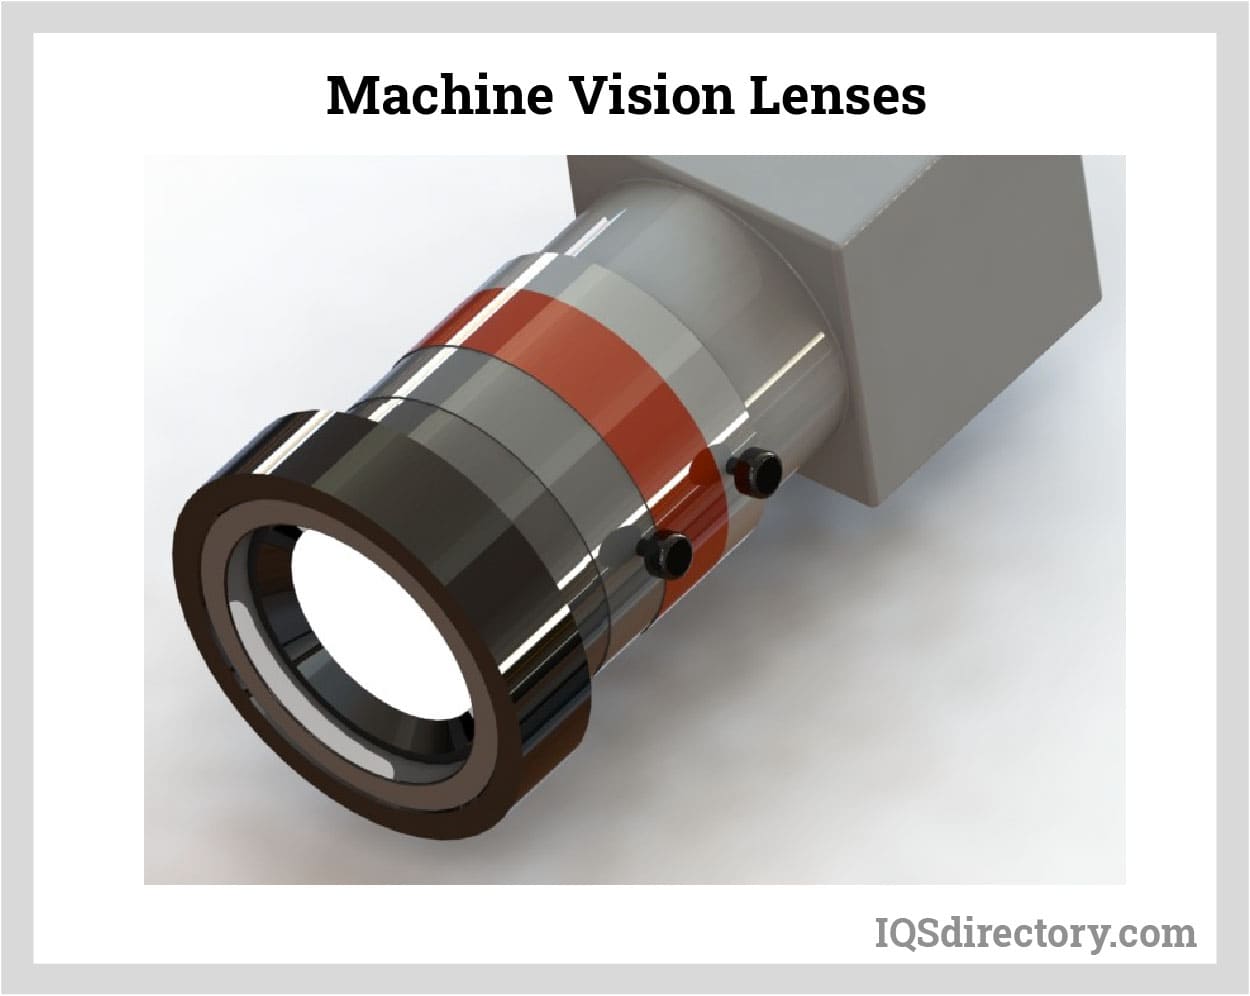
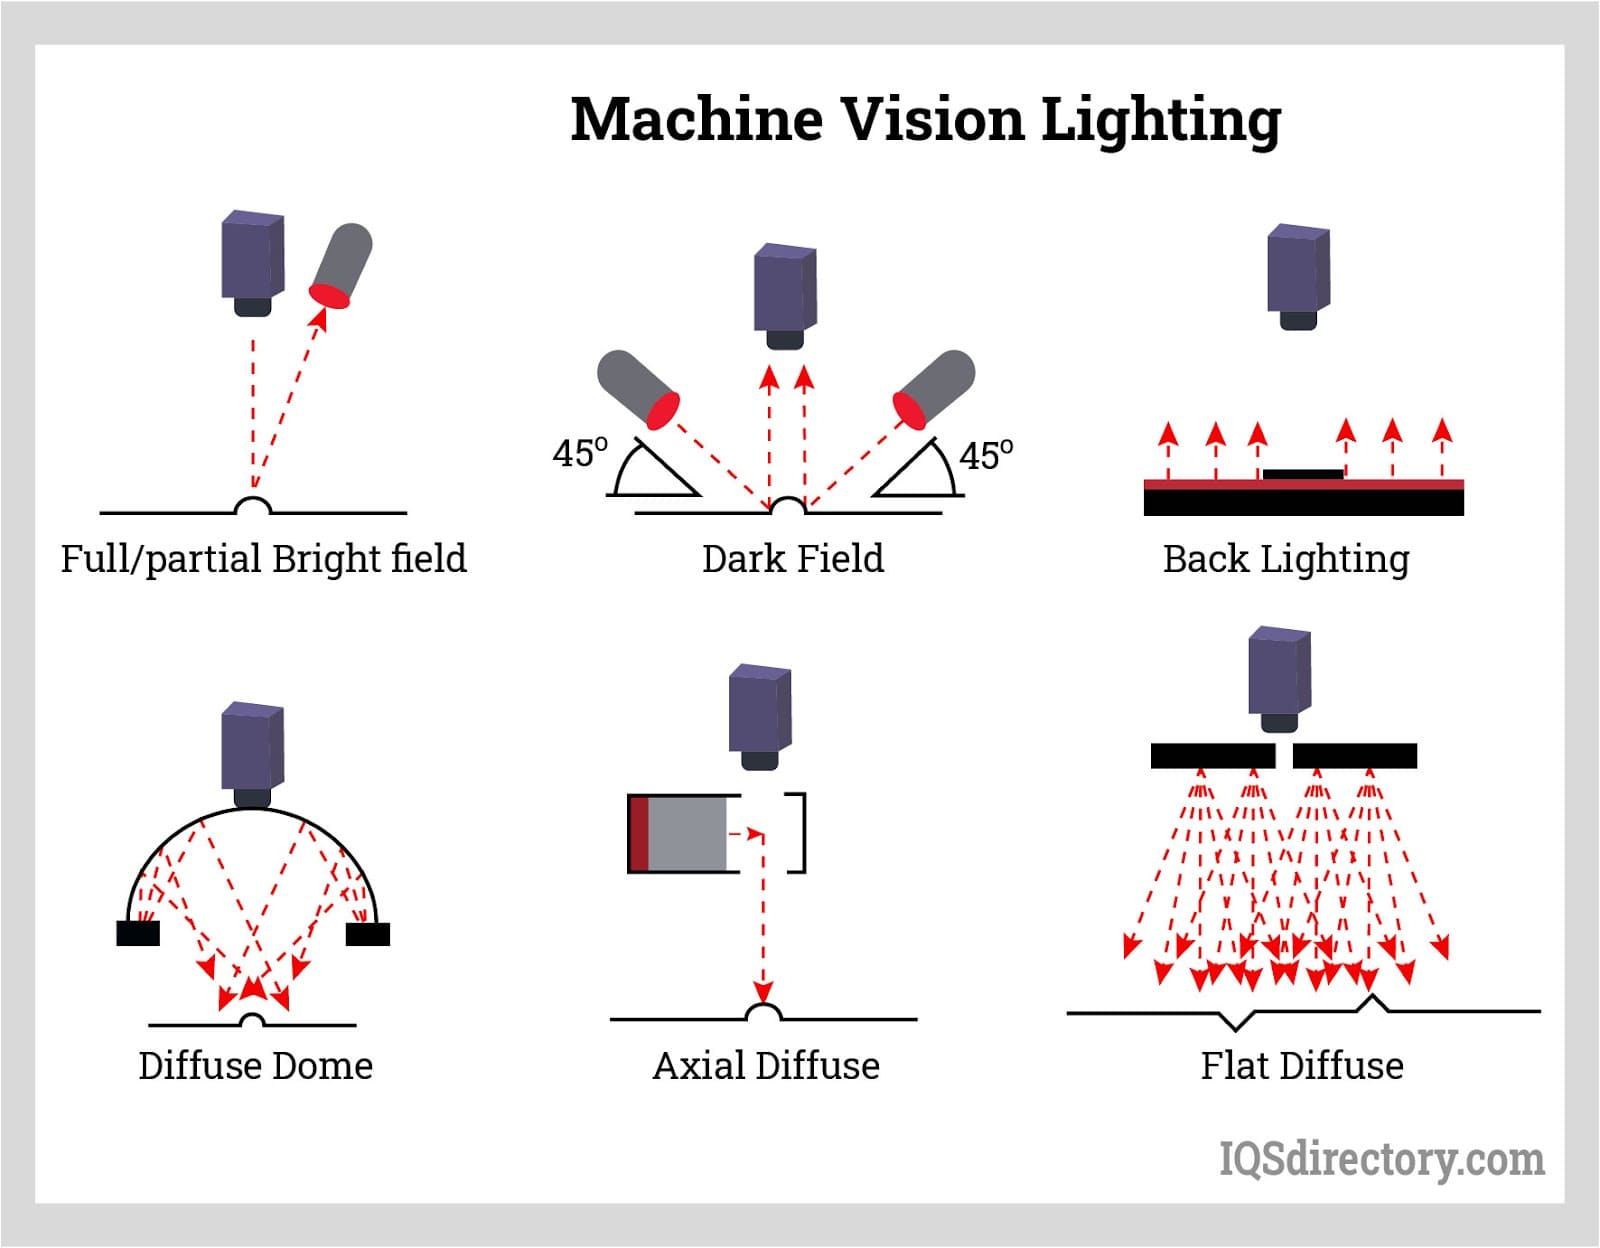
Although machine vision systems can vary widely by design, most share three core components: purpose-built lighting, an imaging device such as a digital camera or vision sensor, and dedicated image processing software. Together, these elements allow the system to capture a usable image, isolate the required features, and turn visual data into measurements, inspections, or control signals.
Imager Component For digital cameras, manufacturers may integrate the imager within the main machine vision unit or keep it separate. When separate, the camera can connect through specialized hardware, a frame grabber in a computer, or direct interfaces such as USB, FireWire, or Gigabit Ethernet. Integrated cameras are often called smart sensors or smart cameras and are used when compact, high-precision image capture is needed close to the production process. Image Processing Software Also called vision software, this programming extracts and interprets raw image data from cameras or sensors and converts it into actionable output. It supports tasks such as counting, measuring, inspecting, sorting, OCR, code reading, and pass-fail verification for operators and automated equipment.Standards and Specifications of Machine Vision
Machine vision systems must align with a range of industry standards based on geography, application, and system design. One of the best-known organizations in this area is EMVA (European Machine Vision Association), which promotes consistent measurement methods, transparent image data reporting, and broader compatibility across products. EMVA also supports programming and evaluation practices that make it easier to compare equipment and share data across flexible automation platforms. The group works with organizations such as AIA in North America, JIIA in Japan, VDMA in Germany, and CMVU in China.
The GigE Vision standard, developed by AIA, is another widely used interface standard for cost-effective Gigabit Ethernet communication between cameras and host systems. For buyers comparing machine vision cameras, inspection software, and system integration options, standards like these can simplify selection, reduce integration issues, and support stronger long-term interoperability.
Choosing the Right Machine Vision System Manufacturer
When searching for a machine vision product or turnkey system, it helps to work with an experienced supplier that can recommend the most suitable technology for your application. The list of machine vision system manufacturers on this page provides a starting point for comparing providers with different specialties, service models, and solution capabilities. Before reviewing profiles, prepare a detailed list of your requirements so discussions stay focused and productive. Include information such as the primary application, inspection goals, barcode or OCR needs, quality targets, budget, timeline, required standards, delivery expectations, and support needs. After outlining your criteria, compare the listed suppliers, narrow the field to three or four candidates, and discuss your project in more detail. If you are asking, “Which machine vision system fits my line?” or “How do I compare machine vision manufacturers?”, that preparation will make the selection process much easier.
Machine Vision Terms
Common Questions
7 questions
What Is a Machine Vision System?
A machine vision system uses cameras, optics, lighting, sensors, and software to capture and analyze images for inspection, measurement, verification, and process control. In industrial automation, these systems handle fast, repeatable visual tasks with a high level of accuracy, making them well suited for manufacturing lines where consistency and throughput matter.
How Does Machine Vision Work in Manufacturing?
Machine vision in manufacturing uses cameras, controlled lighting, and image processing software to inspect parts, verify assembly, measure dimensions, and read barcodes or characters. It applies tools such as edge detection, segmentation, OCR, and pattern recognition to support quality assurance, reduce scrap, and improve production efficiency.
What Are the Main Components of a Machine Vision System?
The main components are lighting, an imaging device such as a camera or sensor, and image processing software. Many systems also rely on optics, communication interfaces, and control hardware that translate captured visual data into measurement, pass-fail, guidance, or sorting decisions on automated equipment.
What Are Common Applications of Machine Vision?
Common machine vision applications include automated inspection, defect detection, barcode and 2D code reading, OCR, robot guidance, presence-absence verification, gauging, and product sorting. These uses improve traceability, throughput, and repeatability across industrial production lines in sectors ranging from electronics to packaging and automotive manufacturing.
What Are the Benefits of Using Machine Vision Systems?
Machine vision systems reduce manual inspection errors, detect fine surface flaws, verify tolerances, and improve repeatability in high-volume operations. They also help manufacturers gather production data, strengthen quality control programs, and make faster, better-informed decisions that support uptime, yield, and customer satisfaction.
What Types of Cameras Are Used in Machine Vision?
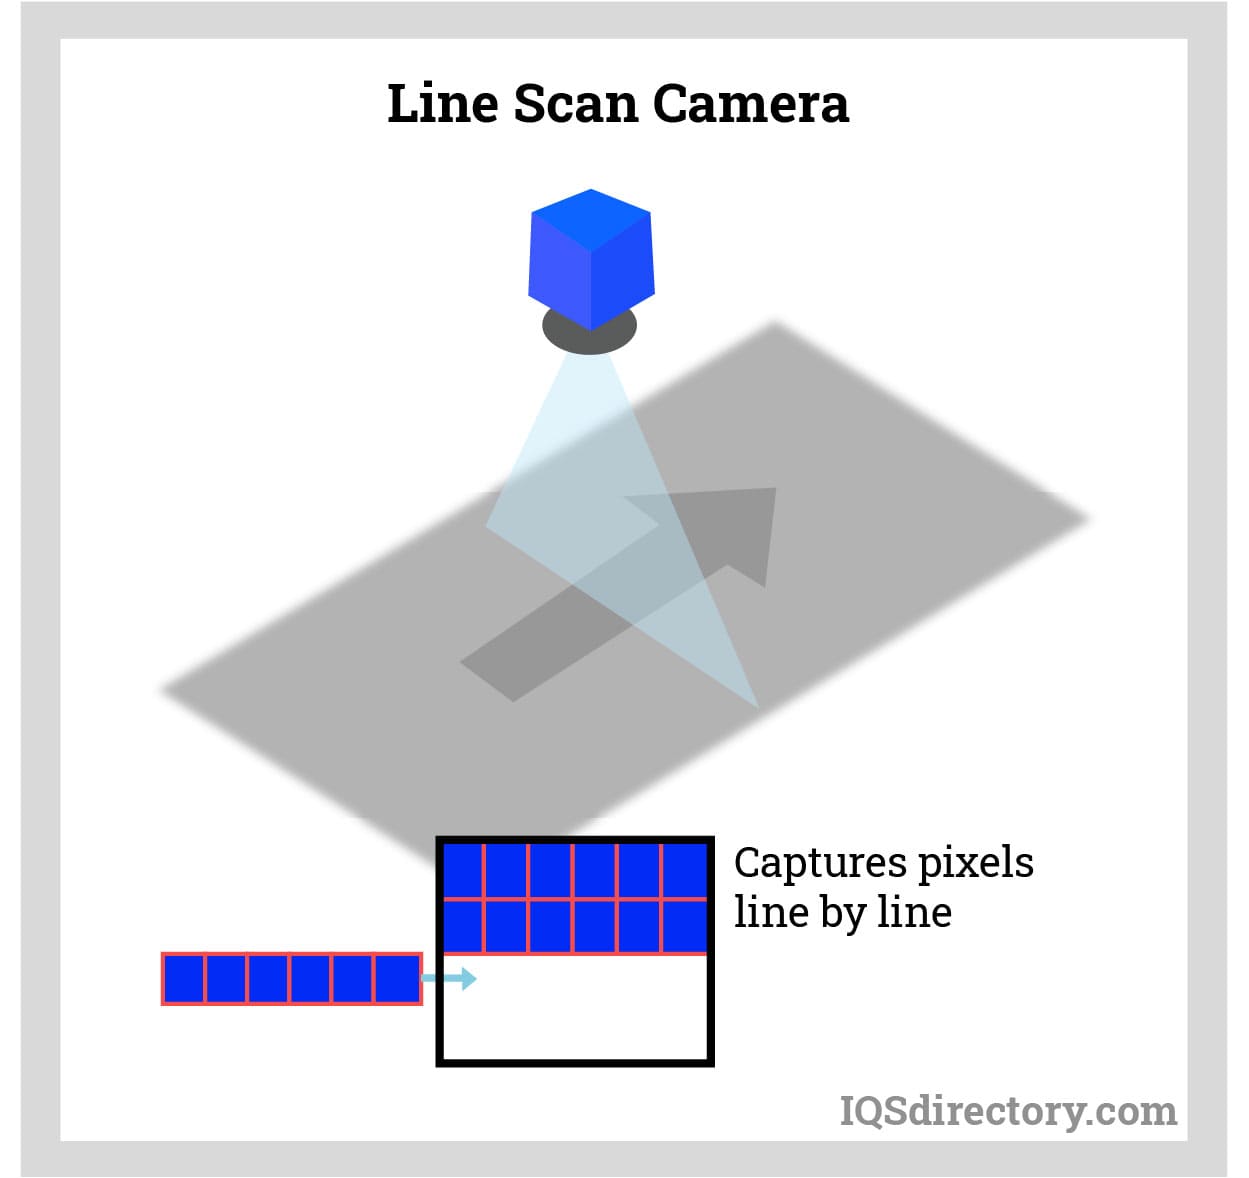
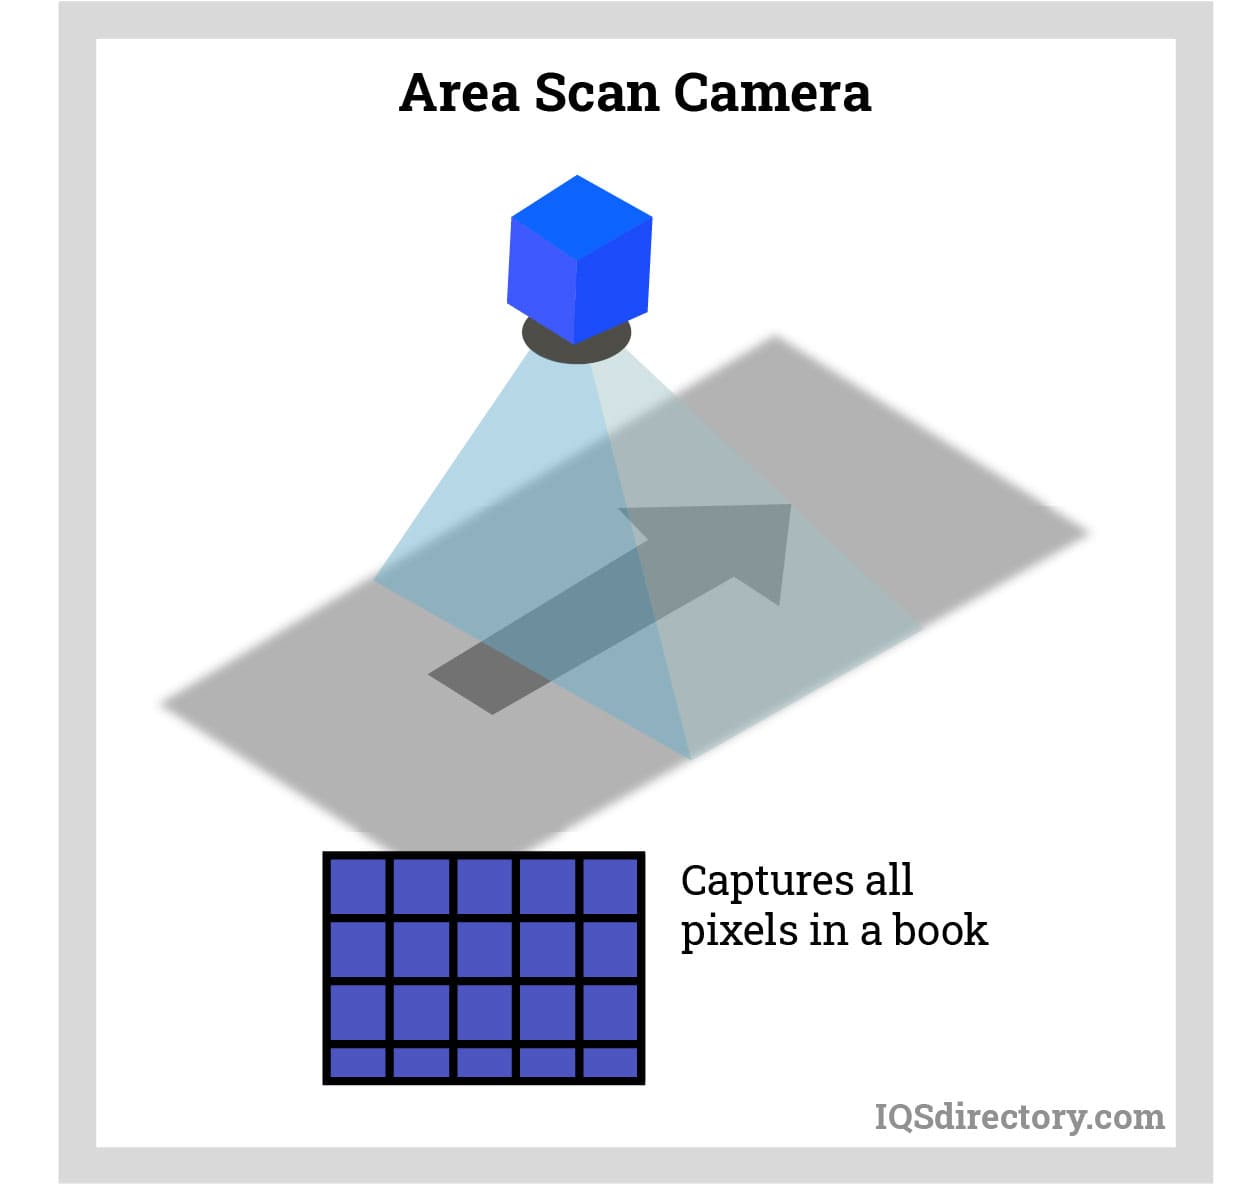
Common machine vision camera types include line-scan cameras, area-scan cameras, CCD cameras, and smart cameras. Line-scan models build an image one row of pixels at a time, area-scan cameras capture a complete frame instantly, and smart cameras combine imaging with onboard processing for space-saving inspection tasks.
How Do Machine Vision Standards Improve System Performance?
Standards such as GigE Vision and EMVA support compatibility, integration, and consistent measurement practices across machine vision hardware and software. They help buyers compare equipment with more confidence and make it easier to connect cameras, software, controls, and industrial networks in demanding production environments.