

Rotational Molding: Types, Processes and Materials
IQS Directory EditorialUpdated 8 chapters
5 leading suppliers listed with this guide
Browse rotational molding suppliersContents (8 chapters)
This article presents all the information you need to know about rotational molding. Read further and learn more about the following:
- Overview of rotational molding and its history
- Types of rotational molding machines
- Rotational molding processes
- Thermoplastic vs Thermoset Plastic
- Materials used in rotational molding
- And much more...
Chapter 1: Rotational Molding
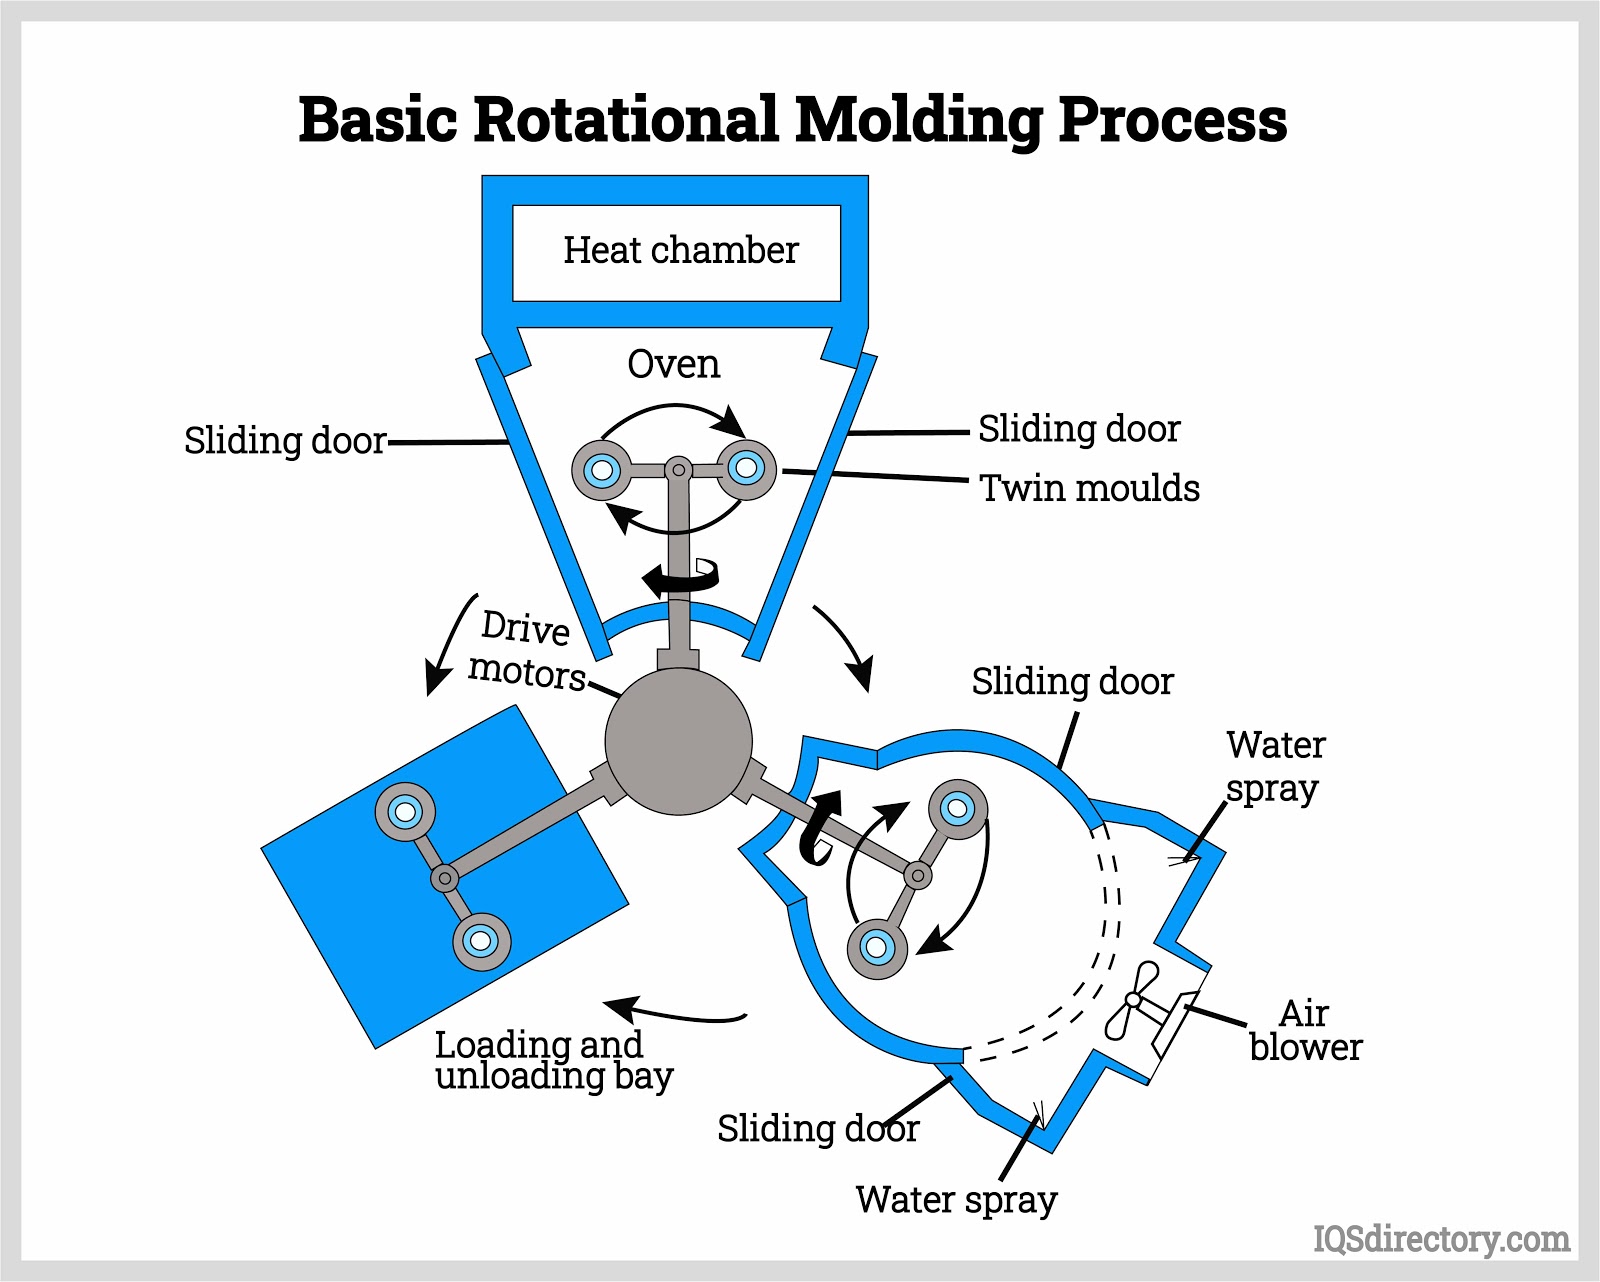
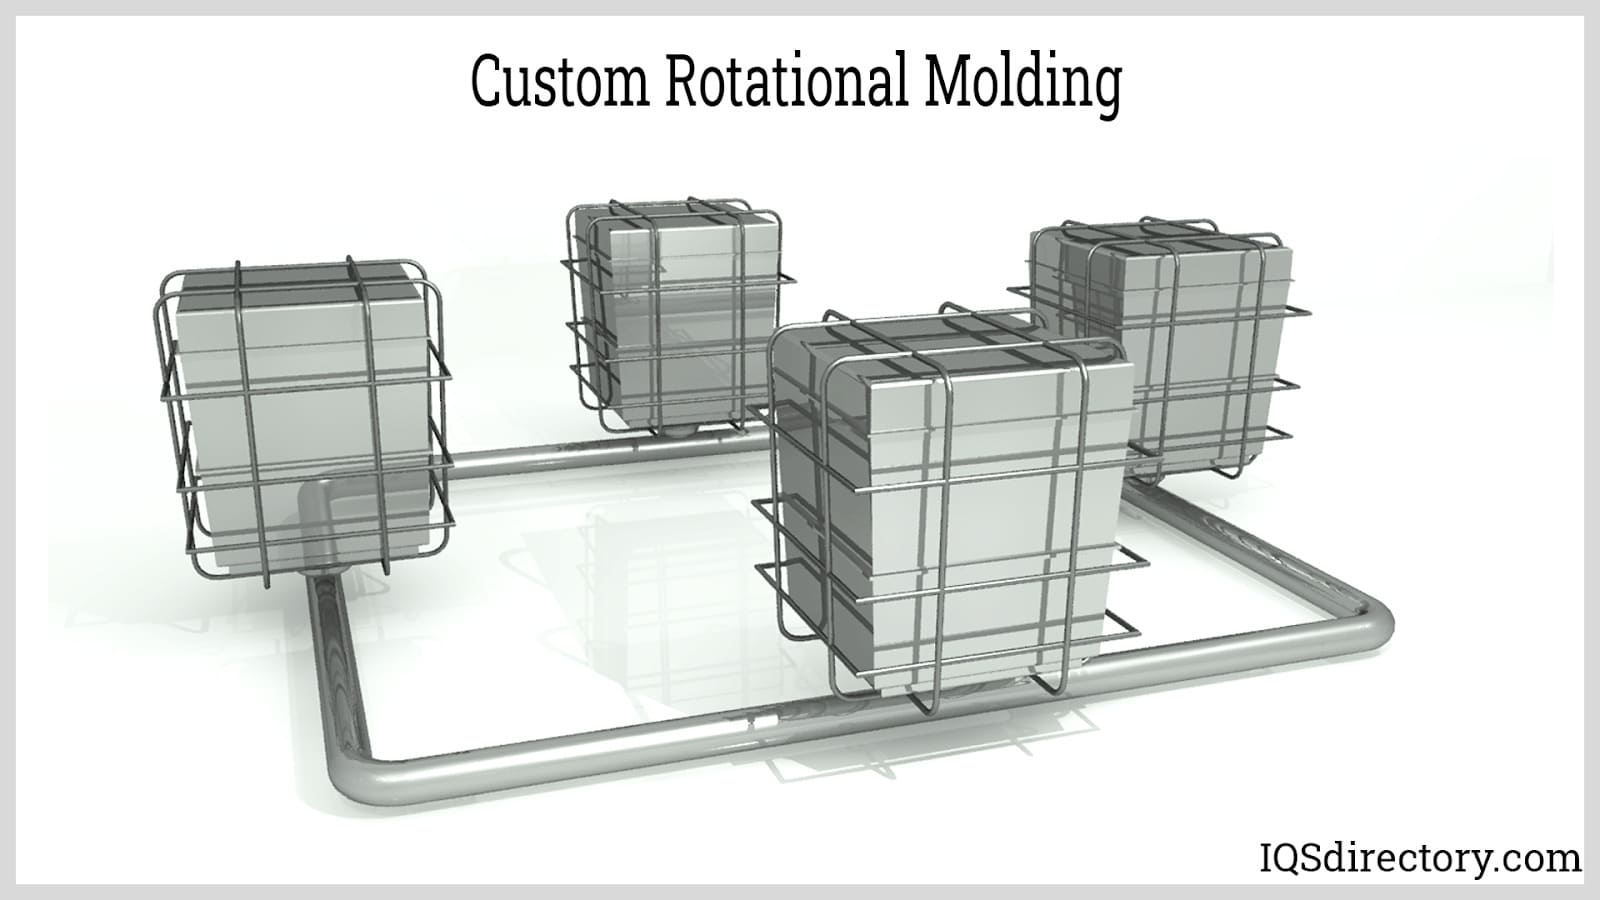
Rotational molding, commonly known as rotomolding or rotational molding plastic manufacturing, is a specialized plastic manufacturing process used to produce large, hollow, and seamless plastic components, often with uniform wall thickness and optional double-wall construction. This plastic molding process is especially valued for creating durable, stress-free parts with consistent material distribution and excellent design flexibility. The process consists of three core stages. First, a precisely engineered mold is mounted onto a rotating arm. The mold is then heated inside an oven while rotating on multiple axes, allowing powdered plastic resin to melt and evenly coat the interior surfaces. Finally, the mold is transferred to a cooling chamber where continued rotation ensures controlled solidification into the finished part.
Rotomolding primarily uses polyethylene resins, including linear low-density polyethylene (LLDPE), high-density polyethylene (HDPE), and other specialty compounds selected for impact resistance, chemical resistance, UV stability, and overall performance. These materials are placed directly into the mold at the start of the cycle, making the process ideal for custom plastic parts and low-volume to medium-volume production. As the mold rotates biaxially within the heating chamber, the resin disperses evenly across the mold cavity, producing parts with consistent wall thickness, excellent structural integrity, and high surface quality. This even material distribution eliminates internal stresses and weak points commonly found in other molding methods, improving durability in demanding environments.
Once the heating cycle is complete, the mold is moved into a cooling station where air or water cooling gradually solidifies the molten plastic. After cooling, the mold is opened and the finished rotomolded product is removed. Components produced through rotational molding are known for their durability, impact resistance, weatherability, and long service life, making them suitable for demanding industrial, commercial, and outdoor applications. Because the process supports custom rotational molding, manufacturers can also incorporate inserts, molded-in threads, ribbing, textured finishes, and secondary fabrication features to better match end-use requirements.
As a low-pressure molding process, rotational molding significantly reduces tooling costs because molds do not need to withstand high internal pressures. This advantage enables manufacturers to economically produce parts in a wide range of sizes, from small containers to extremely large tanks, while also accommodating complex geometries, molded-in features, intricate surface details, and thick-wall or multi-wall configurations. For buyers comparing manufacturing options, rotomolding is often evaluated alongside injection molding and blow molding because it offers excellent design freedom, low tooling investment, and efficient production of hollow plastic products.
Rotational molding supports the production of a diverse array of products, including water storage tanks, chemical storage tanks, kayaks, playground equipment, traffic barriers, medical housings, infant cribs, and industrial containers. Its ability to deliver strong, lightweight, and cost-effective plastic parts makes rotomolding a preferred solution for large-scale hollow components in agriculture, transportation, material handling, marine, and safety product markets. Many manufacturers also choose rotational molding for custom plastic enclosures and OEM plastic components because the process can balance performance, scalability, and affordability.
The origins of rotational molding date back to ancient civilizations, where early rotational techniques were used for shaping ceramics. More refined applications appeared in the mid-19th century with the molding of artillery shells and later in the early 1900s with the production of hollow chocolate molds. Despite early innovation, slow cycle times and limited process control initially restricted widespread adoption, especially compared with faster high-volume plastic manufacturing methods.
By the 1940s, advancements in materials and machinery enabled rotational molding to produce consumer products such as doll heads and toys using polyvinyl chloride plastisol resins. These developments spurred industrial interest, leading to broader adoption across automotive, marine, and safety product manufacturing. As demand grew, manufacturers increasingly recognized the value of rotomolding services for producing custom, large-format parts with repeatable quality and relatively low setup costs.
Modern rotational molding technology has evolved to support larger, more complex designs with improved energy efficiency, automation, and process control. While extended heating and cooling cycles remain a consideration, ongoing innovations in machine design, material science, and quality control continue to enhance productivity, consistency, and scalability. Today, advanced rotational molding systems are used to meet tight product specifications, improve cycle optimization, and support sustainable manufacturing goals through reduced scrap and efficient resin utilization.
Chapter 2: Types of Rotational Molding Machines
A typical rotational molding operation consists of a mold-holding arm or cradle, one or more heating ovens, and dedicated cooling stations. Rotational molding machines are essential industrial systems used to manufacture hollow plastic parts, tanks, containers, and custom components through controlled heating, rotation, and cooling of thermoplastic resins. The primary distinction among machine types lies in how molds travel between stations and how rotation is managed during each phase of the process.
Understanding the capabilities and advantages of different rotomolding machine configurations allows manufacturers to select equipment best suited to their production volume, part complexity, material requirements, and floor space constraints. The most common types of rotational molding machines include:
-
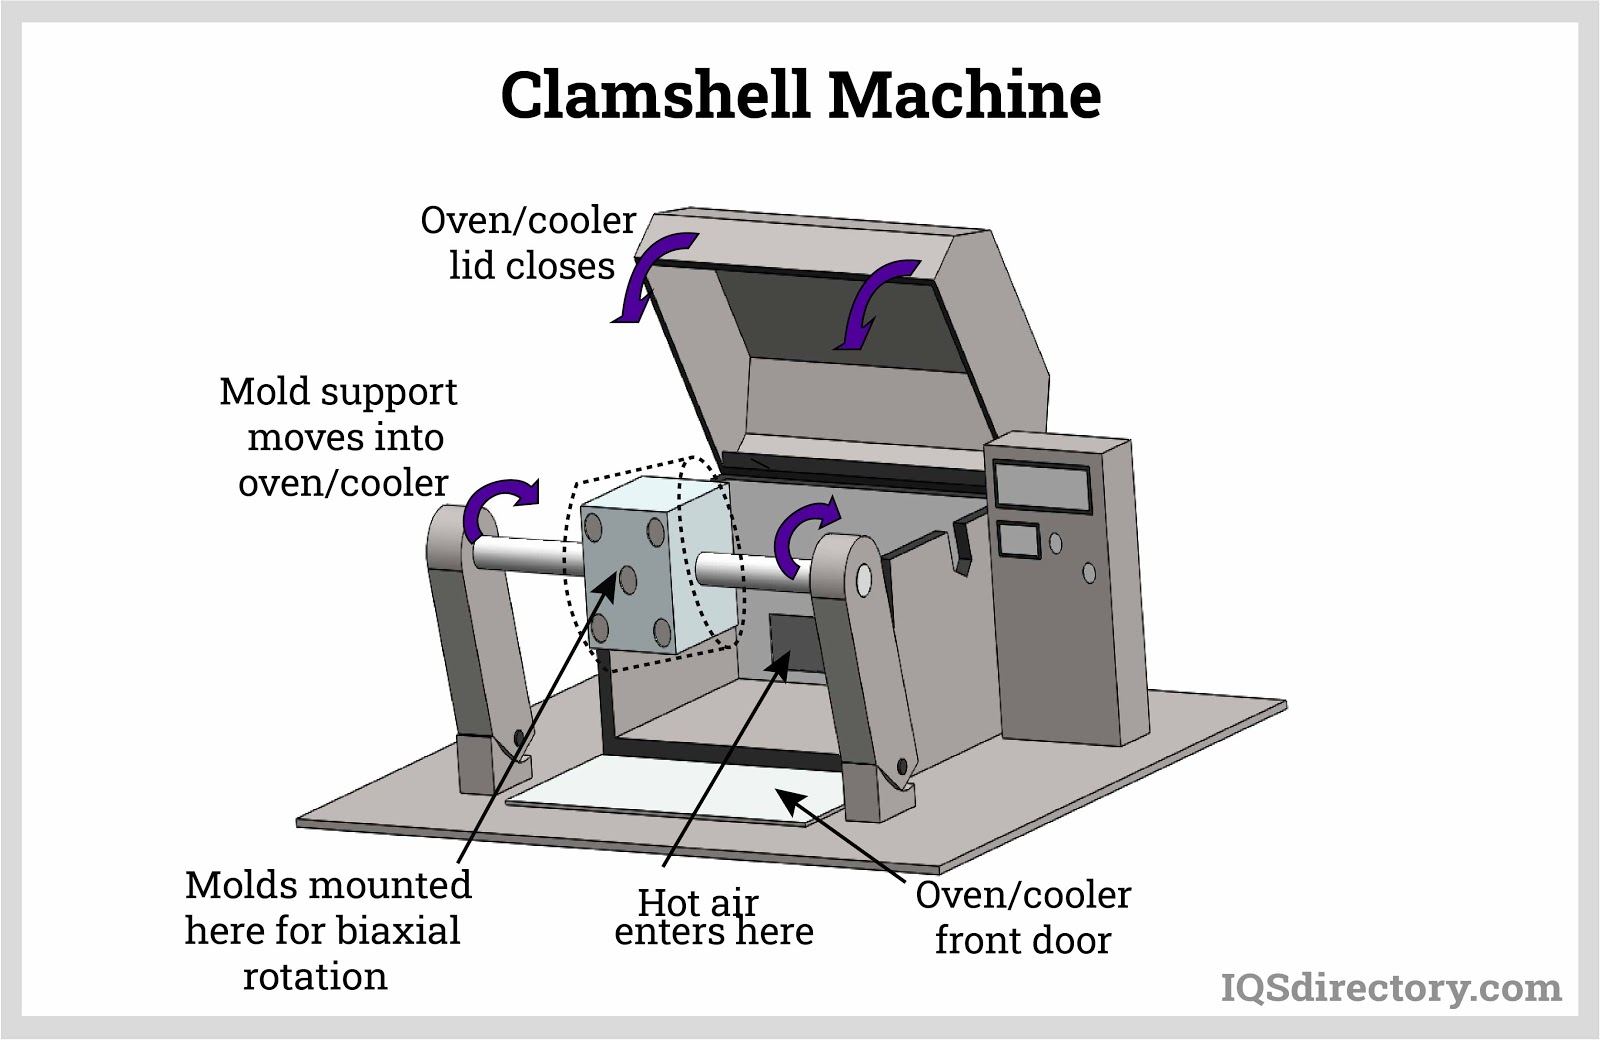
Clamshell Machine: Clamshell rotational molding machines are single-station systems where heating and cooling occur within the same chamber. These machines are ideal for low-volume production, prototyping, and custom plastic parts. The mold is loaded from the front and securely sealed during heating to ensure uniform temperature exposure. Once molding is complete, the chamber opens to allow rapid cooling and easy demolding, making clamshell machines simple, flexible, and cost-effective.
-
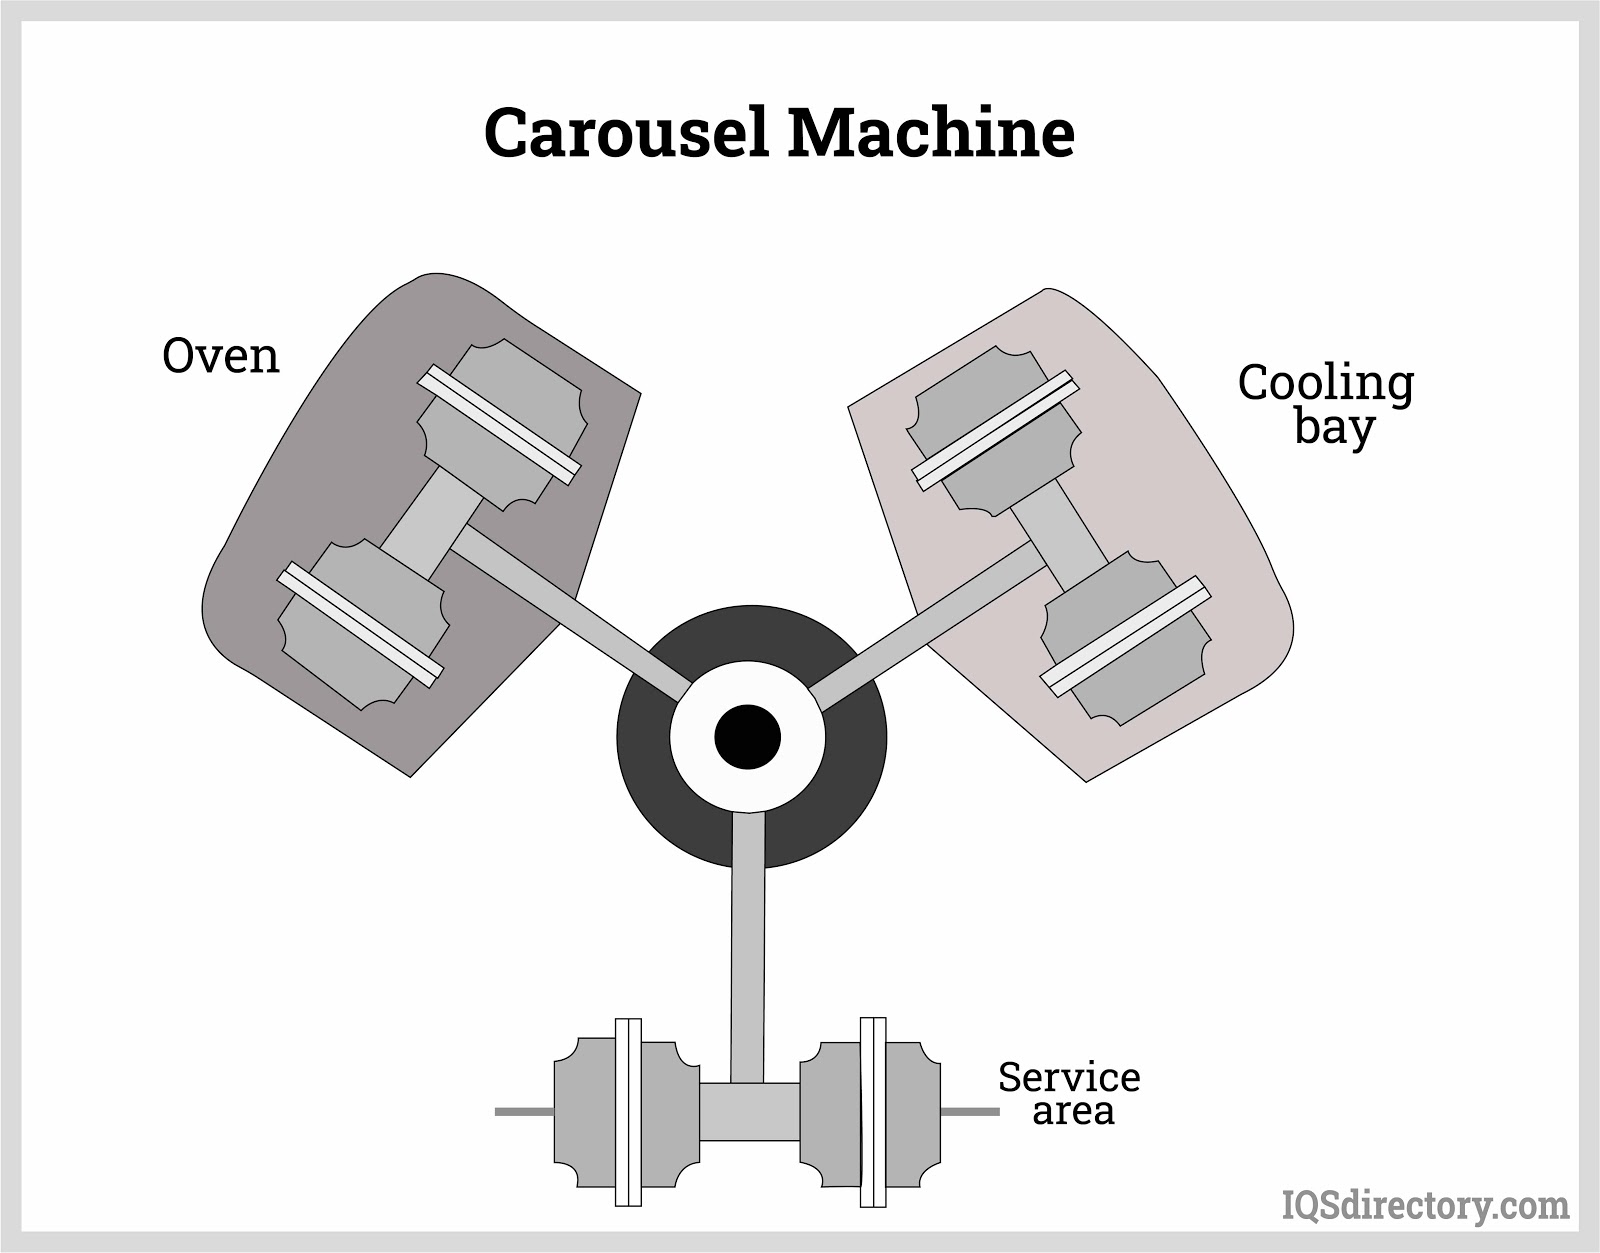
Turret or Carousel Machine: Carousel rotational molding machines are among the most widely used systems for high-volume production. Featuring three to six arms mounted around a central hub, these machines move molds through loading, heating, cooling, and unloading stations in a continuous cycle. Advanced controls such as PLCs and HMIs enable precise temperature management, automation, and repeatability.
Independent-arm carousel machines allow each mold arm to operate with unique cycle times and thickness requirements, enabling manufacturers to produce different parts simultaneously. This configuration maximizes throughput and flexibility but may involve higher capital and maintenance costs.
-
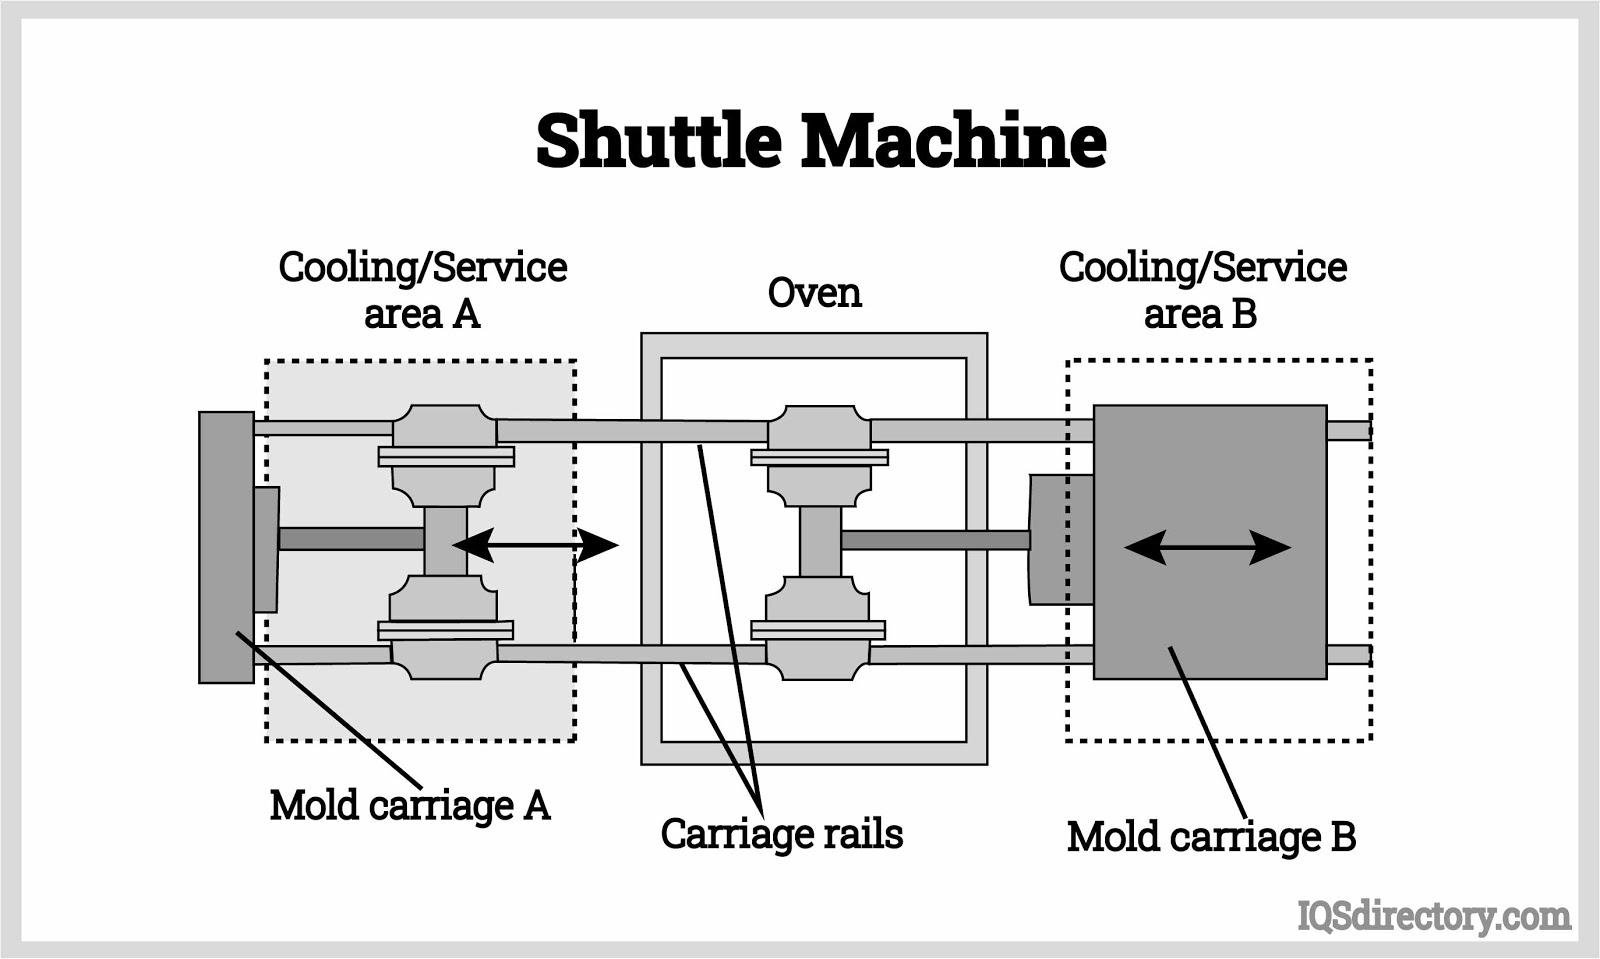
Shuttle Machine: Shuttle rotational molding machines are designed for efficient use of space and high productivity. Independent arms move molds between a central oven and separate loading and cooling stations along a track system. This overlapping cycle design minimizes idle time and significantly improves throughput, particularly for medium to large molded parts.
By allowing one mold to heat while another cools, shuttle machines address one of the primary bottlenecks in rotomolding—extended cooling times. Their efficiency, scalability, and lower overall cost compared to large carousel systems make them attractive for growing operations.
-
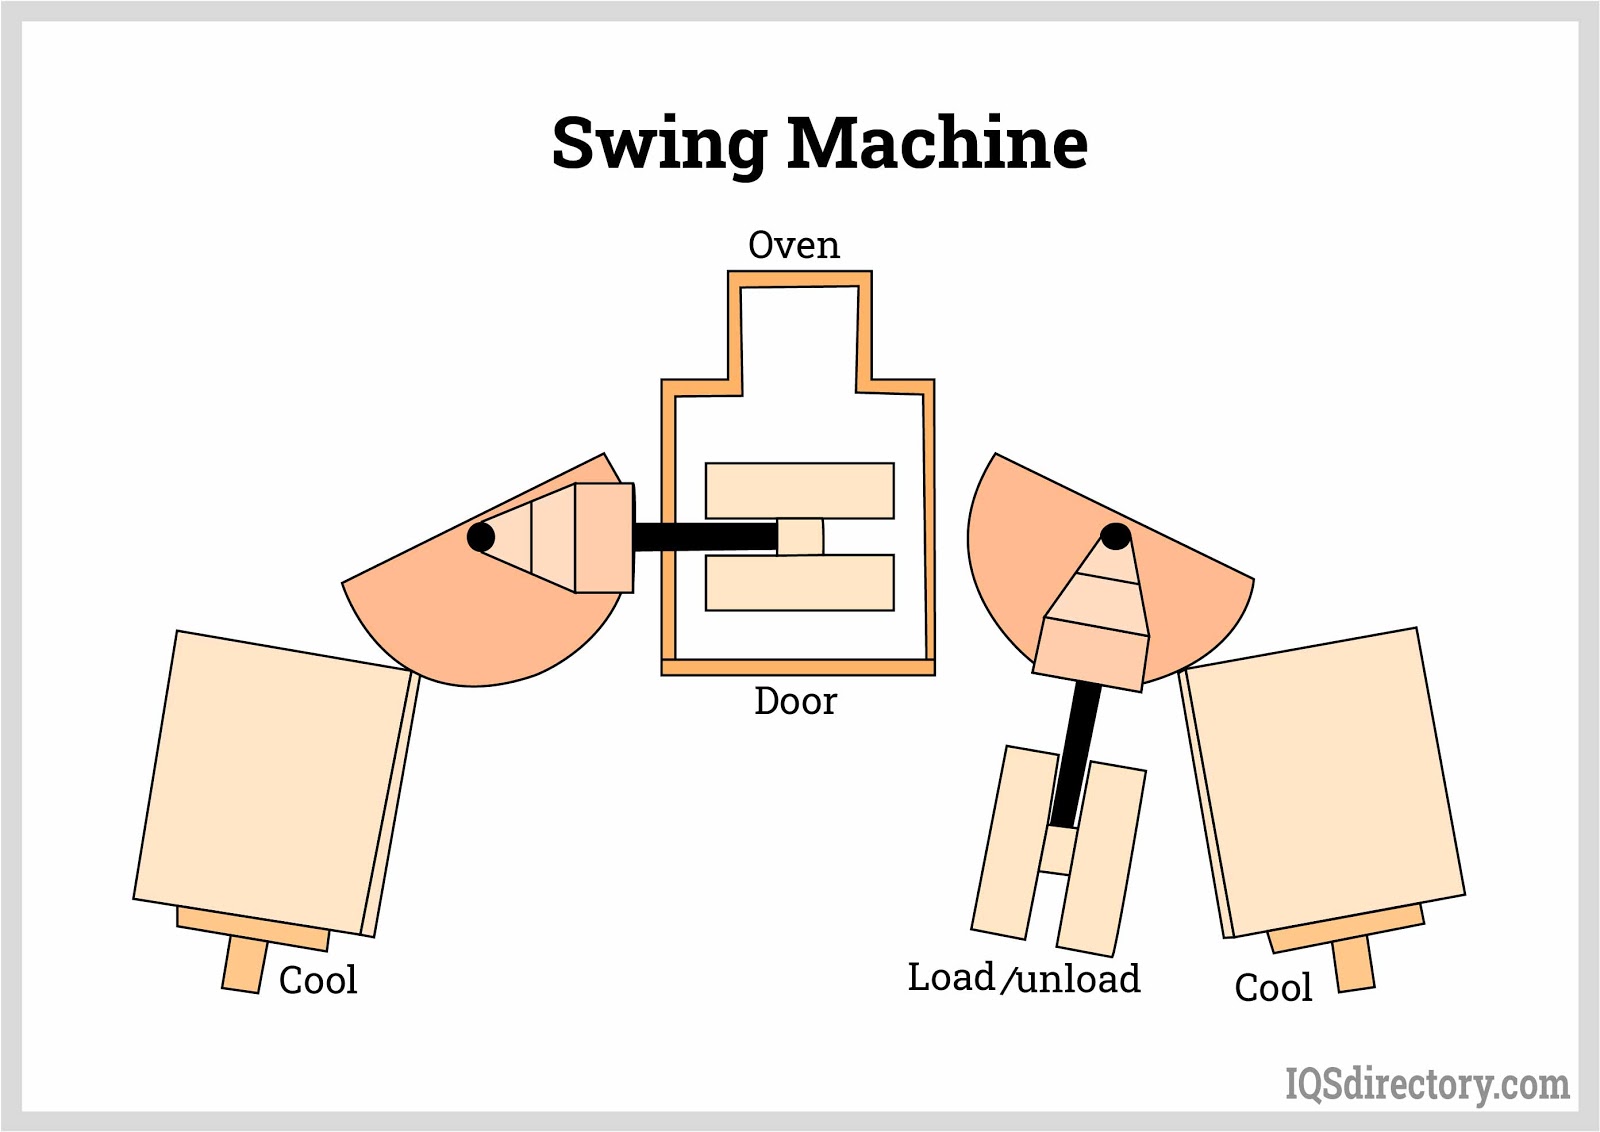
Swing Machine: Swing arm machines use independent rotating arms that pivot between heating and cooling chambers. This configuration is well suited for parts requiring longer cooling cycles or specialty materials. Some systems feature multiple arms per corner, enabling continuous operation and rapid mold turnaround for custom or engineered plastic components.
-
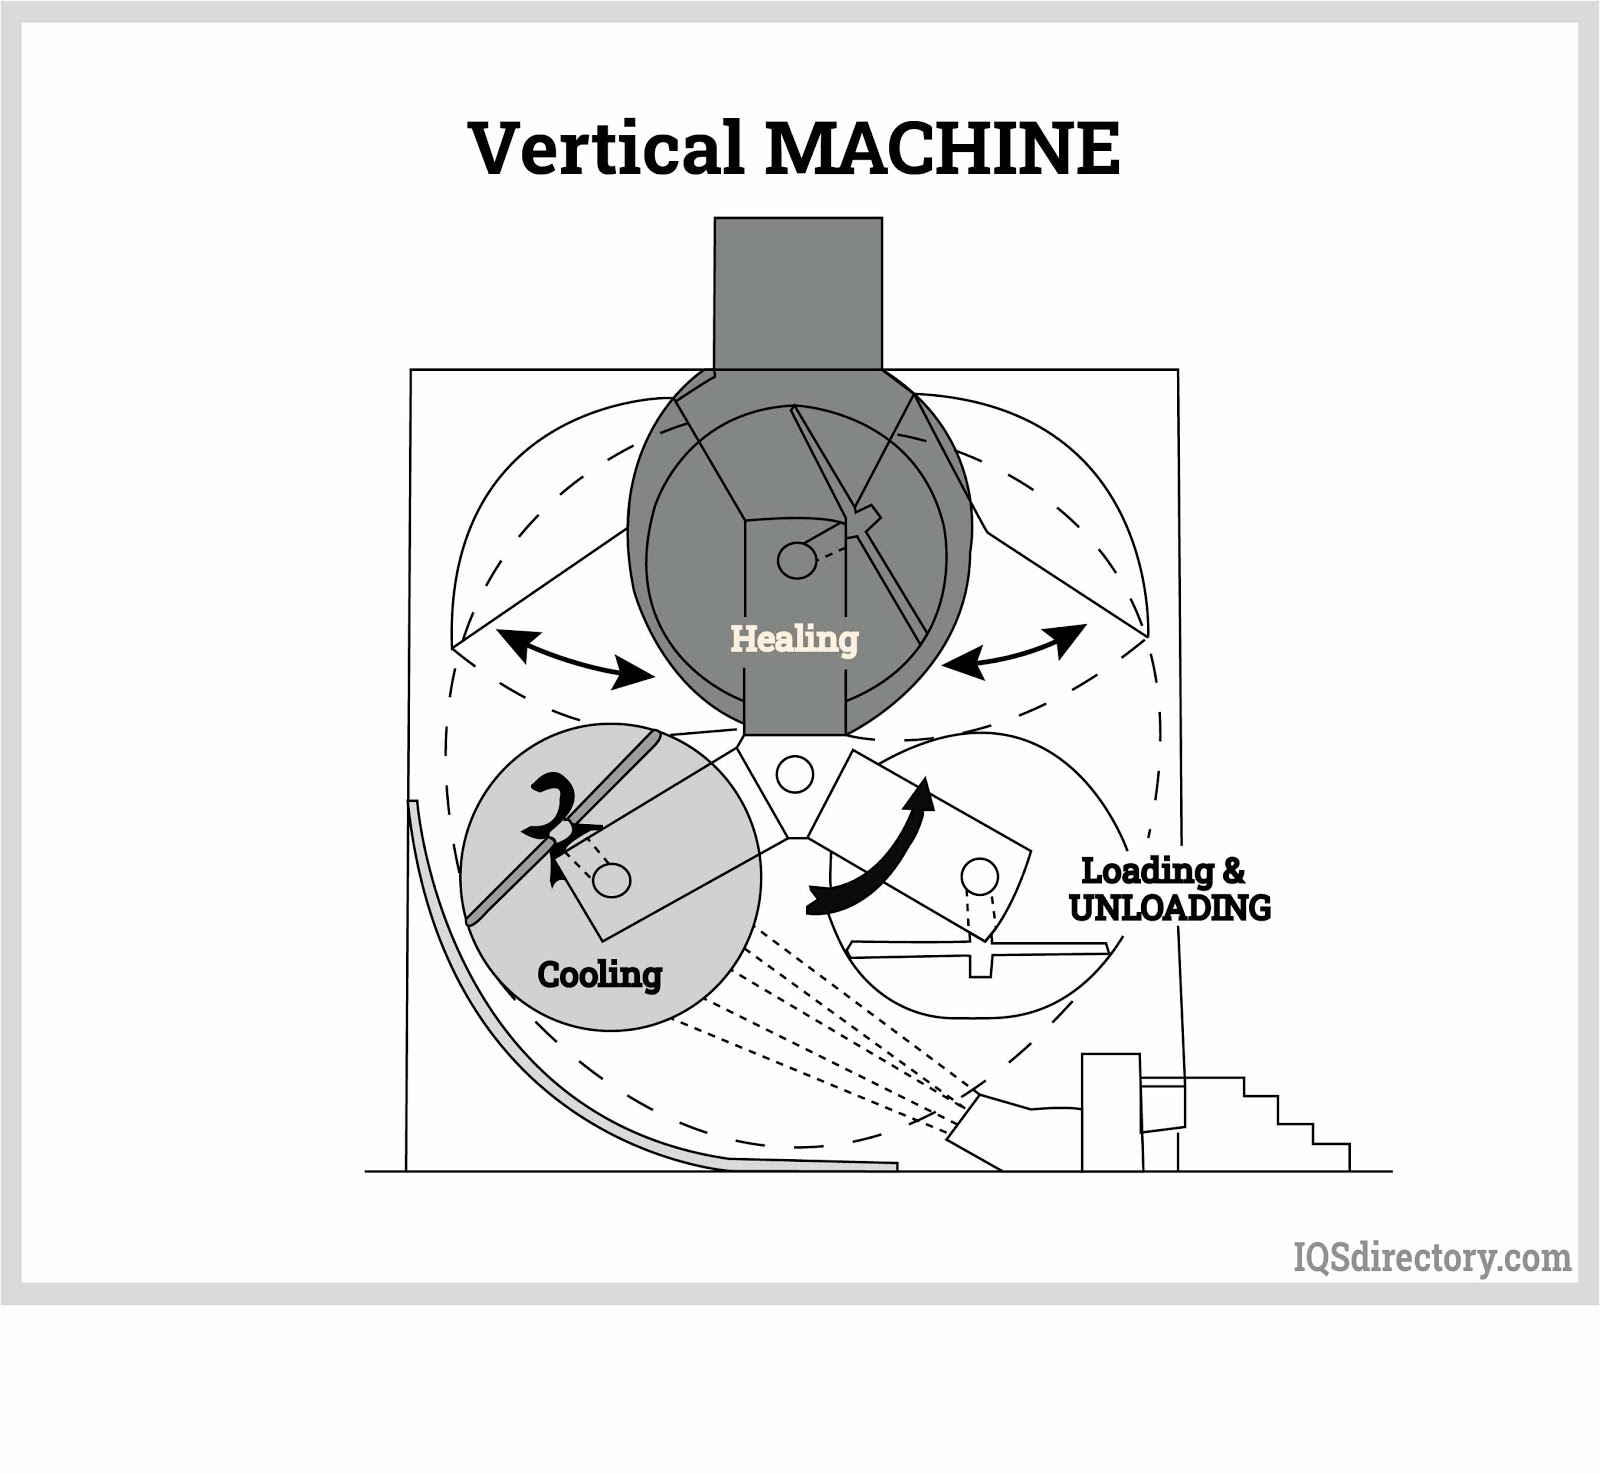
Vertical Wheel Machine: Vertical wheel rotational molding machines operate similarly to a Ferris wheel, cycling molds through each process stage in a vertical loop. These machines are best suited for small to medium-sized products requiring consistent quality and high-volume output, such as bins, containers, and standardized components.
-
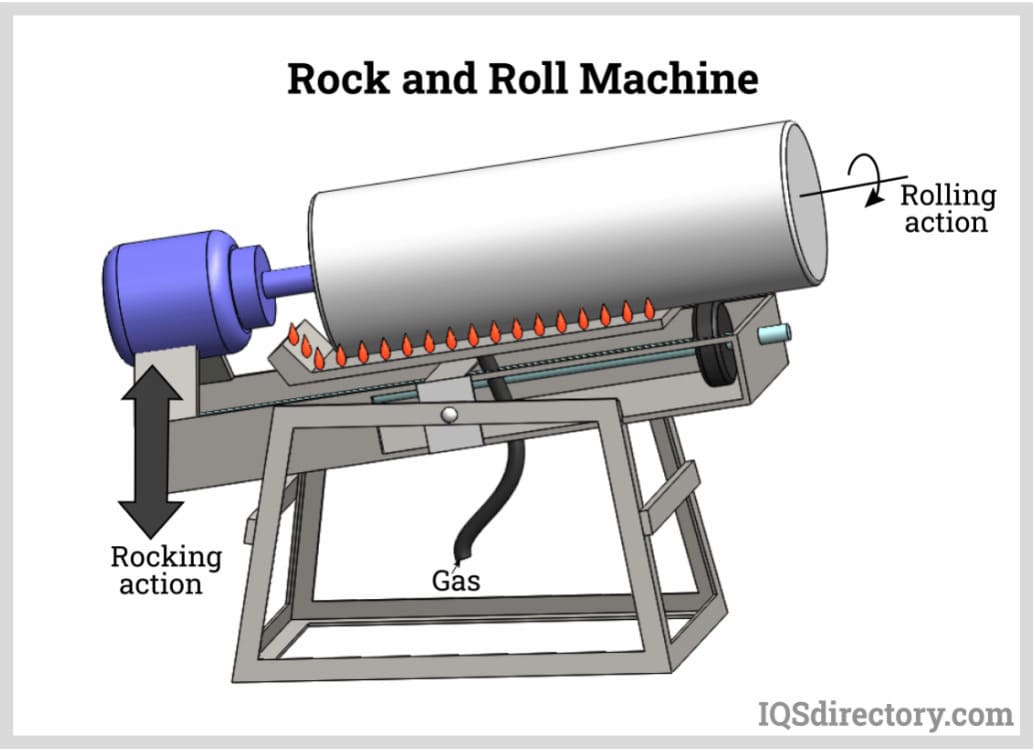
Rock and Roll Machine: Rock and roll machines combine rotational movement with a rocking motion, making them ideal for producing long, narrow parts such as kayaks, canoes, and pipes. The dual-axis motion ensures even resin distribution in elongated molds, delivering consistent wall thickness and structural strength.
- Open Flame Machine: Open flame rotational molding machines represent early rotomolding technology, using direct flame exposure to heat molds. While less common today, they remain useful for open-ended parts, simple hollow products, and low-volume or specialty applications.
Selecting the right rotational molding machine requires careful consideration of production volume, part size, cycle time, energy efficiency, and material compatibility. Whether manufacturing large storage tanks, automotive components, consumer goods, or custom industrial parts, the correct rotomolding equipment plays a critical role in product quality and operational efficiency.
As demand for customized plastic components continues to grow, advancements in automation, smart controls, and energy-efficient heating systems are shaping the future of rotational molding. Evaluating machine capabilities and aligning them with production goals ensures manufacturers remain competitive in the evolving plastics manufacturing landscape.
Chapter 3: Rotational Molding Process
The rotational molding process—commonly called rotomolding or rotational casting—is a highly adaptable plastic manufacturing method used to create hollow, seamless, and low-stress plastic products. It is especially well suited for large, complex shapes that require uniform wall thickness and long-term durability. Below is a detailed explanation of each step in a standard rotational molding operation.
-
Pulverized Resin: Pulverization, also known as milling, converts polymer pellets or coarse resin into fine or extra-fine powder. This step is critical for achieving consistent wall thickness, smooth surface finish, and reliable material flow during the molding cycle. Particle size requirements vary by machine and application, so resins are often processed through multiple pulverizers to reach the desired consistency.
Common pulverization methods include batch pulverization, dry grinding, and wet milling. The chosen method depends on the resin type and the performance requirements of the finished part. Polyethylene resins dominate rotational molding applications, including linear low-density polyethylene (LLDPE), medium-density polyethylene (MDPE), high-density polyethylene (HDPE), low-density polyethylene (LDPE), and cross-linked polyethylene (XLPE).
These materials are thermoplastics, valued for their impact resistance, flexibility, weatherability, and recyclability. Colorants, UV stabilizers, and performance additives are blended into the resin to meet mechanical, environmental, and aesthetic requirements for applications in agriculture, industrial storage, marine products, playground equipment, and infrastructure.
As sustainability becomes a growing priority, many rotomolding operations now focus on optimizing powder efficiency, recycled content usage, and energy-efficient processing.
-
Loading: A carefully measured quantity of polymer powder is placed into a hollow mold, which is then securely closed. The powder must be dry, clean, uniform in size, and free of contamination to ensure proper melting and coating. Resin quantity directly determines the final wall thickness and structural strength of the molded part, making precision loading essential.
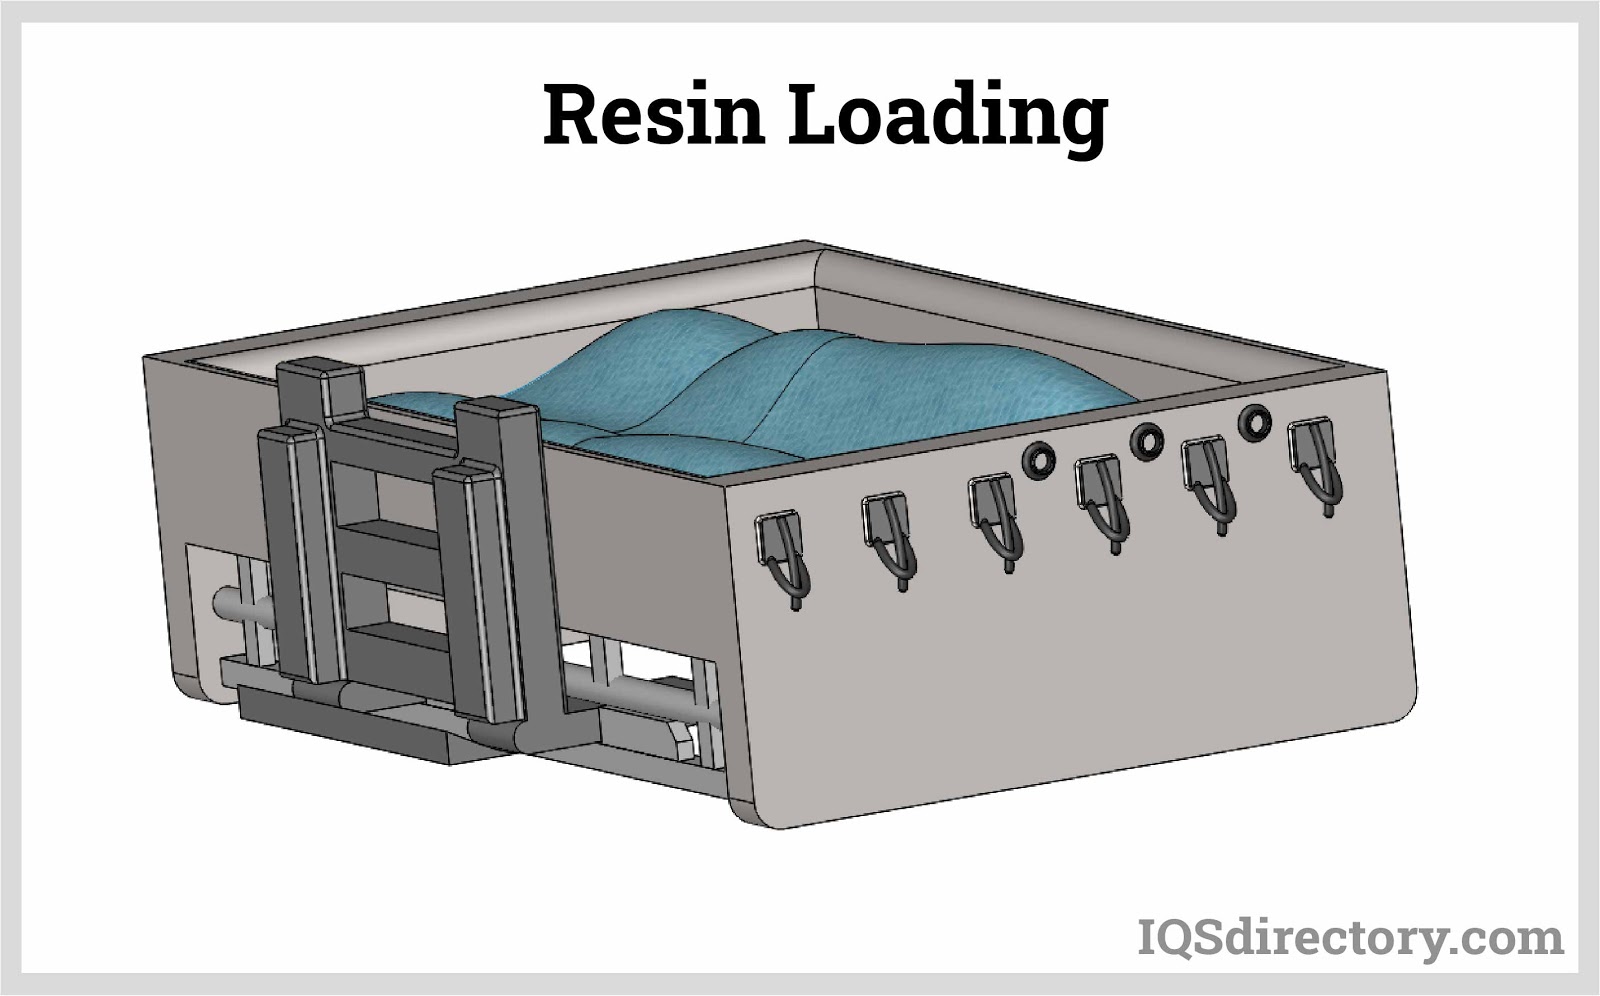
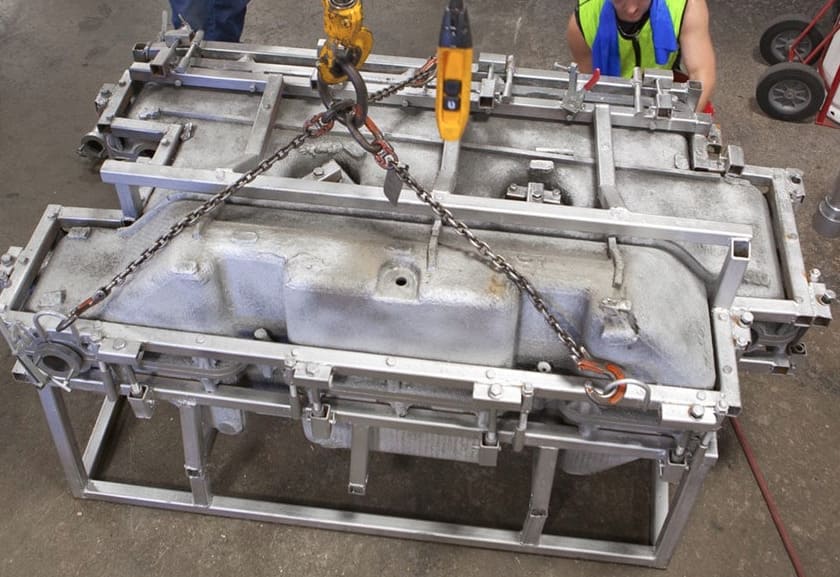
Molds are typically fabricated from cast aluminum or formed steel due to their excellent heat conductivity and durability. Modern mold designs may include CNC-machined details, multi-piece assemblies, and molded-in features that allow complex geometries and consistent surface quality.
To ensure easy part removal and protect mold surfaces, a mold release agent is applied. Common types include:
- Sacrificial coatings, usually silicone-based, applied every cycle and removed with the part
- Semi-permanent coatings, effective across multiple cycles and widely used in production environments
- Permanent coatings, such as PTFE-based treatments, offering long service life but subject to wear over time
-
Heating: The sealed mold is transferred into an oven where it is heated while rotating on two perpendicular axes. This biaxial rotation allows the polymer powder to melt and evenly coat the interior mold surface without the use of pressure. Rotation speeds are typically kept below 15 RPM to promote uniform coverage and prevent material pooling.
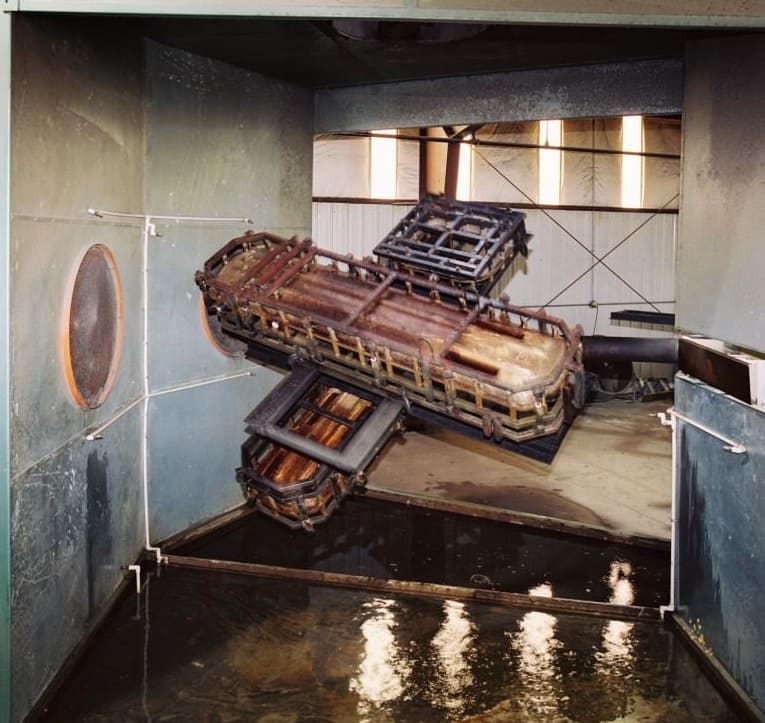
Rotation ratios are adjusted based on part geometry—commonly around 4:1 for symmetrical shapes—and carefully controlled to achieve consistent wall thickness. Accurate temperature management is critical: insufficient heat can cause unmelted resin and voids, while excessive heat may degrade the polymer, reducing impact strength and long-term performance.
Modern rotational molding systems use infrared sensors, real-time monitoring, and automated controls to optimize heat profiles, reduce cycle time, and minimize energy consumption.
-
Cooling: After heating, the mold is gradually cooled while continuing to rotate. Cooling is typically achieved using ambient or forced air, with optional water mist or spray for larger or thicker parts. Controlled cooling prevents warping, shrinkage, and internal stresses that could compromise dimensional accuracy or structural integrity.
Proper cooling preserves material properties and ensures the molded product maintains its intended shape. Although water-assisted cooling can reduce cycle times, excessive or uneven cooling may negatively impact surface appearance and mechanical strength.
-
Demolding or Unloading: Once fully cooled, the finished part is removed from the mold. Automated demolding systems, such as air ejection, help reduce handling damage and maintain consistent surface quality. At this stage, manufacturers inspect parts for wall thickness uniformity, surface finish, and overall quality to ensure compliance with specifications.
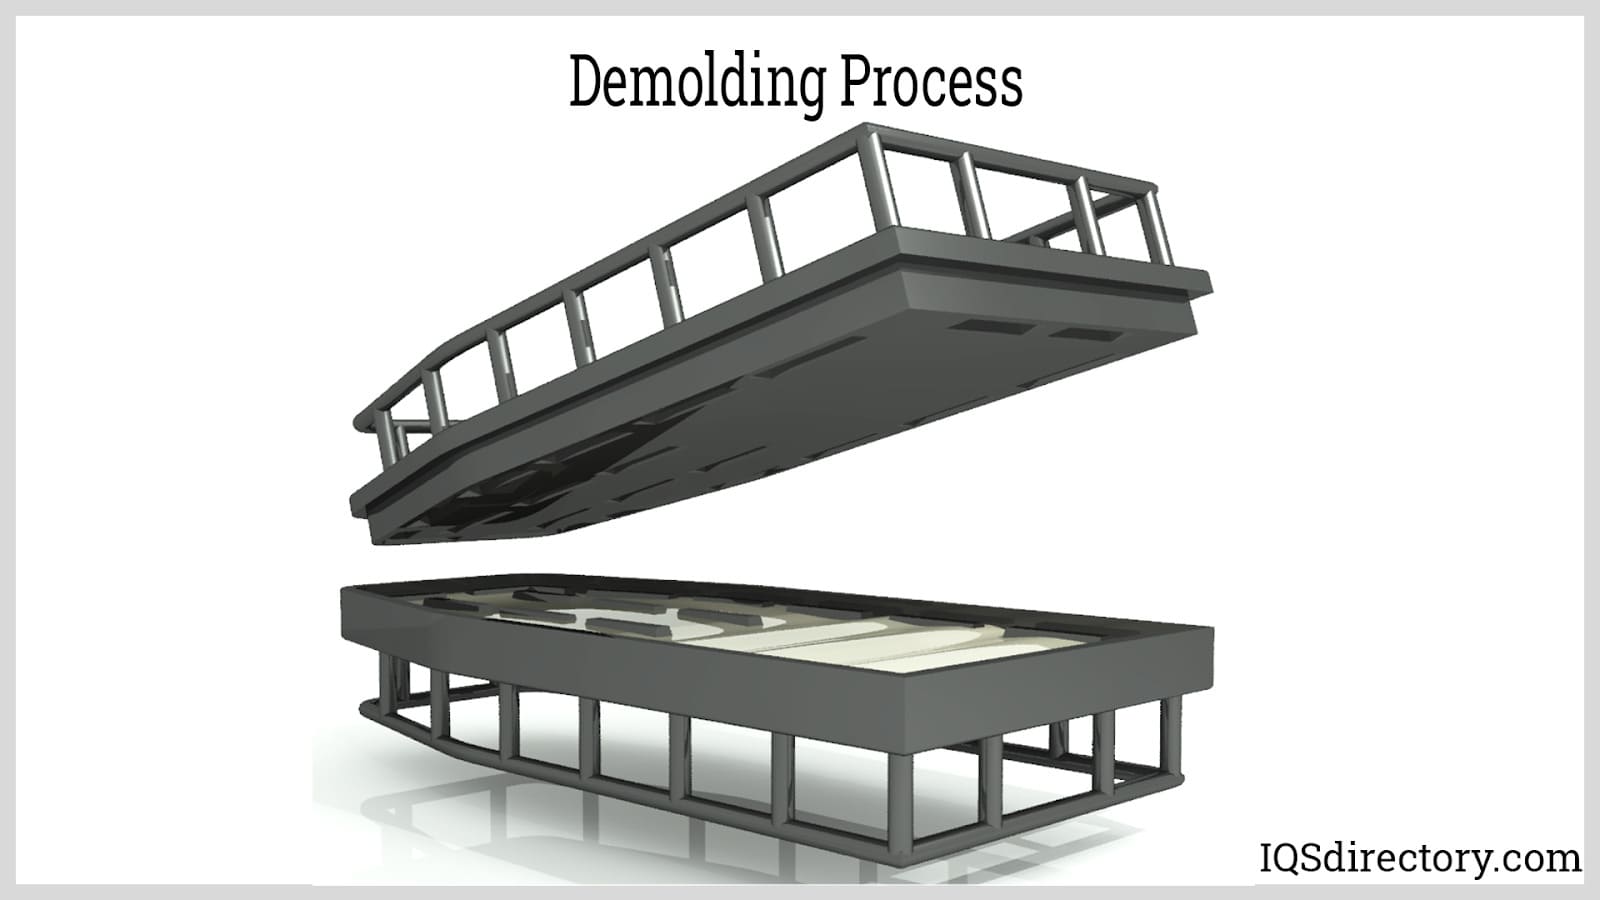
Trimming, deflashing, and edge finishing are often performed to prepare the part for final use or assembly.
-
Secondary Processes: Rotomolded products may undergo additional post-molding operations such as painting, coating, foam filling, welding, drilling, CNC machining, branding, and the installation of threaded inserts or fittings. These secondary processes enhance strength, insulation, appearance, and functionality.
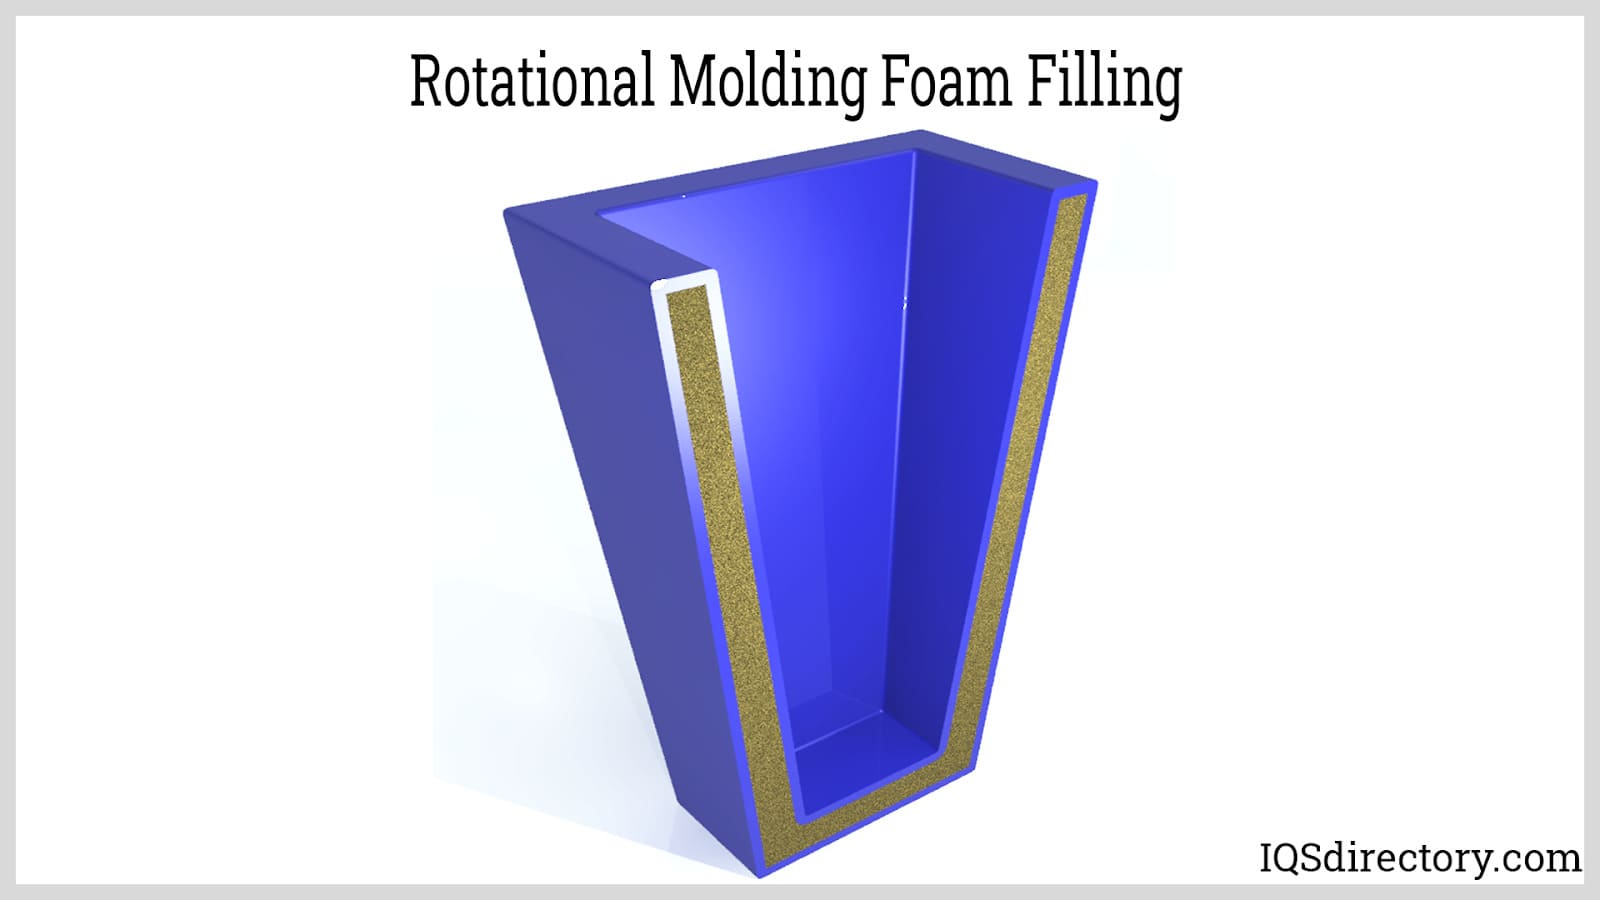
Advanced finishing options allow rotational molding to compete with other plastic manufacturing methods for complex, integrated assemblies used in medical, agricultural, consumer, and recreational markets.
By carefully controlling material selection, powder preparation, mold design, heating, cooling, demolding, and secondary finishing, manufacturers can produce durable, customizable, and cost-effective plastic components. A clear understanding of the rotational molding process supports better design decisions, improved production efficiency, and consistent product quality across a wide range of industries.
Chapter 4: Thermoplastic vs Thermoset Plastic
Thermoplastics and thermoset plastics differ fundamentally in how they respond to heat, and this distinction plays a critical role in determining their performance, lifespan, and application suitability. Thermoplastics soften and melt when reheated, allowing them to be reshaped, reprocessed, and recycled. Thermoset plastics, on the other hand, undergo a permanent chemical change during curing and retain their rigid form even when exposed to high temperatures.
Thermoplastics are widely used in applications where recyclability, repairability, and reshaping are important. Because they do not form irreversible chemical bonds during curing, they can be reheated and remolded multiple times without significant degradation. This property makes thermoplastics—such as polyethylene, polypropylene, and PVC—ideal for processes like rotational molding, extrusion, and injection molding.
Thermoset plastics cure through a chemical reaction that creates a three-dimensional network of cross-linked molecules. Once cured, this structure cannot be melted or reformed. The result is a material with exceptional heat resistance, dimensional stability, chemical resistance, and mechanical strength. These characteristics make thermosets well suited for high-temperature, high-load, or chemically aggressive environments.
The curing process is the defining factor between these two material classes. Thermoplastics remain physically changeable after curing, while thermosets become permanently “set.” The dense cross-linking found in thermoset plastics explains their superior thermal and structural performance, but it also limits recyclability. Understanding these differences helps manufacturers and designers select the appropriate material for performance, sustainability, and manufacturing efficiency.
Advantages of Thermosets
- High-temperature resistance
- Good chemical resistance
- Excellent dimensional stability
- High strength, toughness, and rigidity
Advantages of Thermoplastics
- Eco-friendly and recyclable
- Excellent impact resistance
- Better aesthetic finishing
- Good adhesion to metals
Disadvantages of Thermosets
- Non-recyclable (cannot be remolded)
- Poor thermal conductivity (for electrical housings)
- Brittle
Disadvantages of Thermoplastics
- Can degrade when exposed to UV
- May soften when exposed to heat
- Can be more expensive than a thermoset
| Thermosets | Thermoplastics |
|---|---|
| The material is injected into a hot mold in a cold state | The plastic is melted and injected into a mold |
| Non-remoldable and non-recyclable | Remoldable and recyclable |
| Creates a permanent chemical bond | Fully reversible as there's no chemical bonding |
| Surface finishing is relatively challenging | Provides accurate and aesthetically pleasing surfaces |
| Less heat and pressure requirements | Requires significant heat and pressure |
| Produced through condensation polymerization | Formed by additional polymerization |
| Includes compression, transfer, and casting processes | Involves injection, extrusion, and blow molding processes |
| Common products: tool handles, billiard balls, insulation, computer and TV parts, various electronic and gardening equipment, sprockets, and cooking tools | Common products: vacuum cleaners, toys, machine screws, gear wheels, kettles, packaging films, sacks, power tool housings, toasters, gas lines, and connections |
| Drawbacks include inability to recycle and emission of VOCs | Drawbacks are costliness, ease of melting, and difficulty in prototyping |
Recyclability
As can be determined from the characteristics of the two plastics, thermoplastics are easy to recycle and can be melted and reused multiple times. Existing parts and components can be ground to granules and melted to make new parts. Thermoplastics can be manipulated in several ways, such as adding new thermoplastic resin to old ground up resin to produce new components. The reuse of thermoplastics is a necessity since it takes several decades for the plastic to decompose. Many sustainability programs emphasize the need to reuse and repurpose thermoplastics.
The crosslinked bonds of thermoset plastics prevent the plastics from being melted, reformed, and reused. The molecular structure of thermoset plastics gives them a long useful life but prevents them from being restructured and reused. The solid structure of thermoset plastics enhances their damage to the environment. Like thermoplastics, it takes many decades for thermoset plastics to decompose. They can languish in a trash dump and never change their form or shape.
Cost
The cost factor for the plastics relates to their recyclability. The manufacture of thermosets requires special tooling as well as fillers and additives that are necessary to complete the crosslinking. This aspect of the process affects the cost of thermosets and makes them more expensive. Although this can also be true of thermoplastics, the recyclability of thermoplastics has a distinctive effect on their cost.
As with many aspects of manufacturing, the cost factors for thermosets and thermoplastics are not necessarily black and white. Although the thermoset process is slow and time consuming, the material difference between the plastics can range from $0.90 per pound up to $10 per pound. This contrast is generated by the different properties of the plastics. In most cases, engineers choose between the plastics based on their properties, appropriateness for an application, and their functionality without regard to cost.
Chapter 5: Leading Rotational Molding Machines
In the United States and Canada, there are many machines available for rotational molding. These machines play a crucial role in modern manufacturing, allowing for the cost-effective and efficient production of a wide range of plastic products. This capability supports industries such as automotive, furniture, medical devices, and toys. Below, we discuss several leading machines used in rotational molding.
Manufacturer: Ferry Industries, Inc.
Model: ARM PR-8
Features: The ARM PR-8 is a versatile rotational molding machine featuring multiple arms, which provides precise and efficient molding. It comes with advanced controls and energy-efficient heating systems, ensuring consistent production of high-quality plastic parts.
Manufacturer: Rotoline
Model: RL-3200 Carousel Machine
Features: The RL-3200 Carousel Machine is renowned for its large production capacity and flexibility. It is capable of producing large, complex parts with excellent control over the molding process. Additionally, its user-friendly interface simplifies operation and management.
Manufacturer: Rotomachinery Group
Model: CARROUSEL ROTO Series
Features: The CARROUSEL ROTO series by Rotomachinery Group features independent arm controls, making it well-suited for producing a diverse range of plastic products with varying shapes and sizes. These machines offer customizable molds and efficient heating systems.
Manufacturer: Persico
Model: ROTO2000
Features: The ROTO2000 by Persico is a rotational molding machine renowned for its ability to produce seamless, hollow products such as tanks and containers. It is celebrated for its reliability and consistent performance in large-scale production.
Manufacturer: Caccia Engineering
Model: Caccia BI-AX
Features: The Caccia BI-AX model is a bi-axial rotational molding machine that enables the production of double-walled and multi-layered plastic parts. This capability enhances structural integrity and offers versatile design possibilities for various applications.
Please note that the rotational molding machine market is dynamic, and newer models may have emerged since this update. Therefore, it's advisable to conduct further research to ensure you have the latest and most accurate information.
Chapter 6: Materials Used in Rotational Molding
The polymers most commonly used in rotational molding are outlined below. The majority are thermoplastics, meaning they can be reheated and reshaped without losing their fundamental properties. This characteristic makes them well suited for the low-pressure, high-temperature conditions required in the rotational molding process.
-
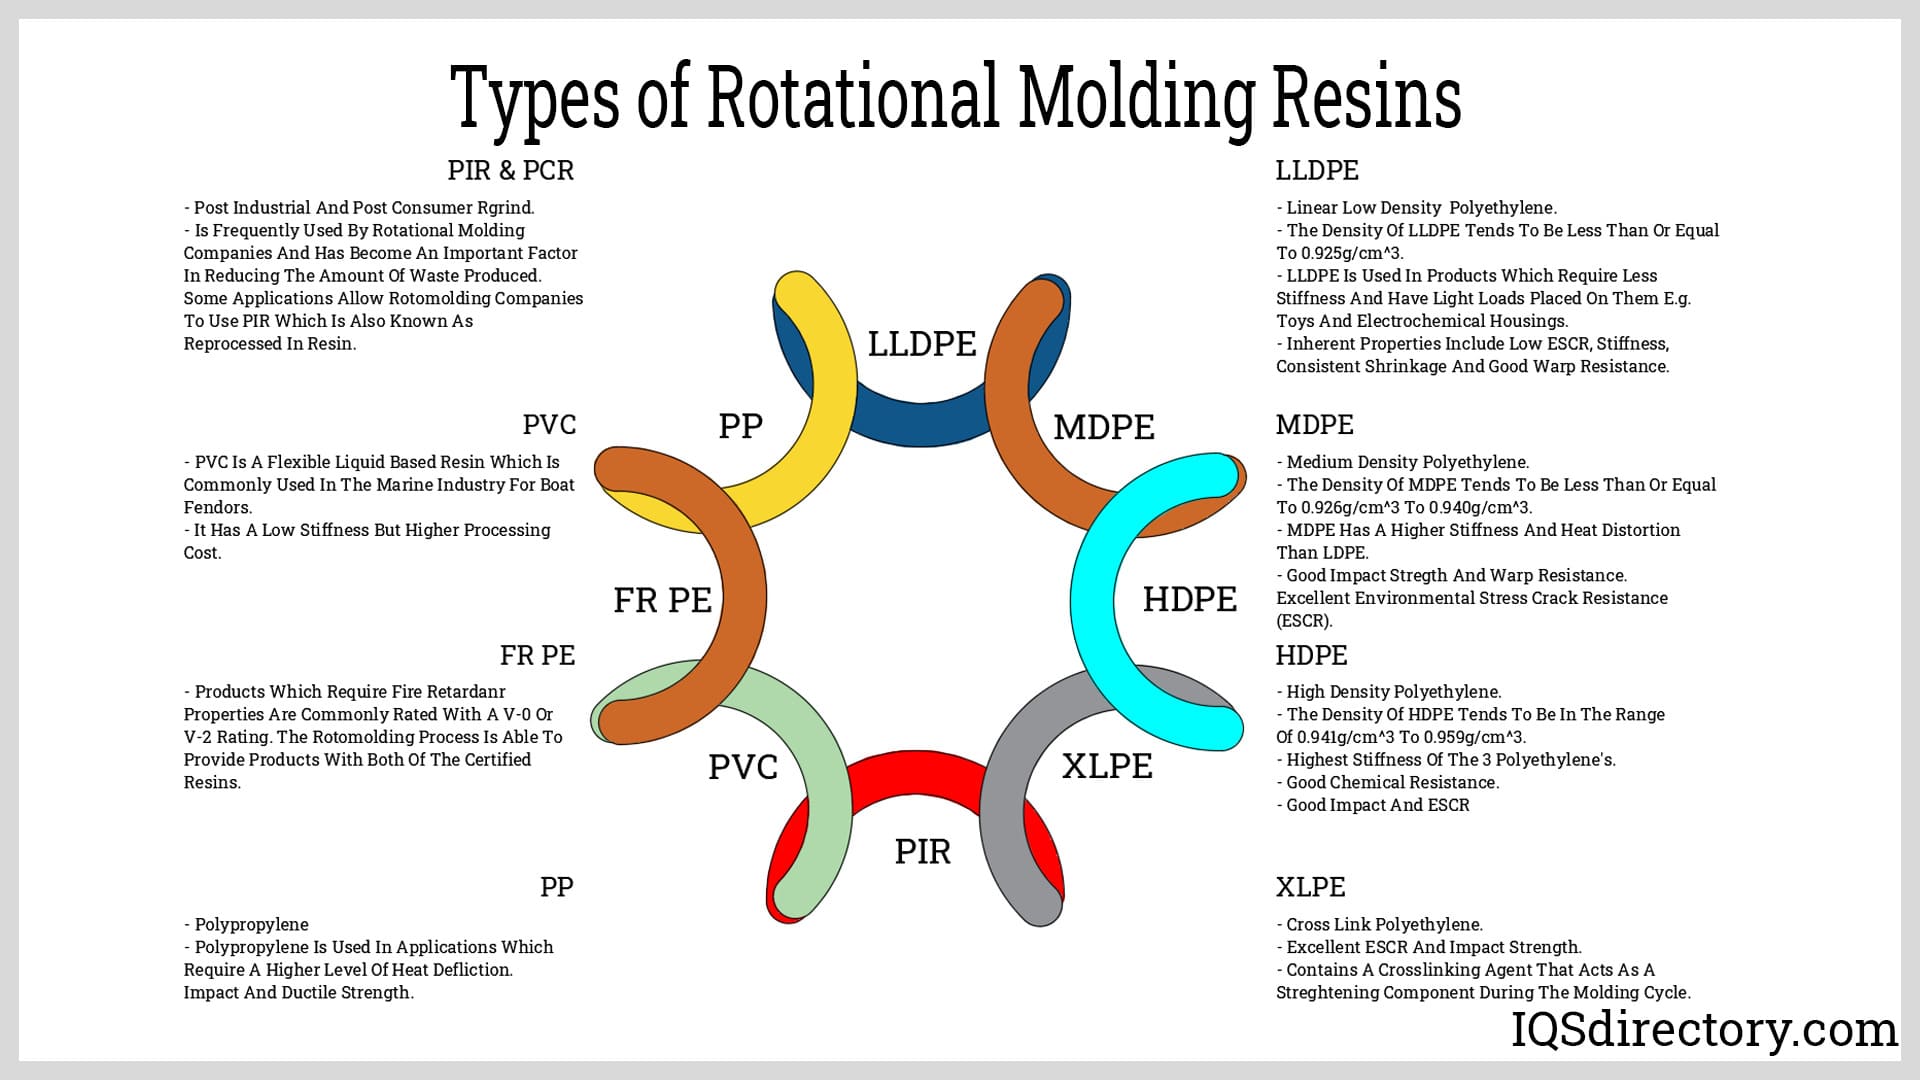
Polyethylene: Polyethylene accounts for over 80% of all materials used in rotational molding, largely due to its cost efficiency, excellent processability, and broad performance range. Supplied in powdered form, polyethylene is easier to grind and distribute evenly inside a rotating mold than many other polymers. It also provides strong chemical resistance, low moisture absorption, and good impact performance, making it ideal for tanks, containers, playground equipment, and industrial housings.
Common polyethylene grades used in rotomolding include high-density polyethylene (HDPE), low-density polyethylene (LDPE), medium-density polyethylene (MDPE), and linear low-density polyethylene (LLDPE), each selected based on stiffness, impact resistance, and environmental exposure requirements.
- Polypropylene: Polypropylene is the second most frequently processed polymer in rotational molding and is valued for its balance of strength, flexibility, and thermal performance. Its properties fall between those of LDPE and HDPE, offering improved heat resistance, chemical stability, and fatigue resistance. Polypropylene is often chosen for applications requiring higher temperature tolerance and repeated mechanical loading.
- Polyvinyl Chloride: Polyvinyl chloride (PVC) is derived from vinyl chloride monomer and is known for its rigidity and structural strength. Through the use of additives and plasticizers, PVC can be modified to achieve a wide range of mechanical characteristics, including flexibility, impact resistance, and flame retardancy. These attributes make it suitable for specialized molded components and protective enclosures.
- Nylon: Nylon belongs to the polyamide family of plastics and, in addition to its common use in fibers and films, can be formulated as a molding compound. It offers excellent toughness, abrasion resistance, and thermal stability, along with good resistance to chemicals. Nylon is typically selected for demanding applications where higher strength and durability are required.
When choosing a polymer for rotational molding, manufacturers must consider several process-specific limitations that influence material selection:
- During molding, the molten polymer is exposed to oxygen at elevated temperatures, which can lead to oxidation and degradation. As a result, the polymer structure must include antioxidant-compatible groups or stabilizing additives.
- The polymer must exhibit strong thermal stability to withstand extended heating cycles without undergoing permanent changes in mechanical or physical properties.
- Because rotational molding relies solely on gravity and rotational movement rather than pressure, the molten polymer must flow easily along the mold walls. Proper melt flow behavior at high temperatures is essential and must be evaluated during process optimization.
Primary additives are commonly incorporated to improve both material performance and processing efficiency. Flow modifiers enhance melt flow for uniform wall thickness, while heat stabilizers protect against thermal degradation. Fillers can be added to increase stiffness, and impact modifiers improve toughness; however, excessive use may reduce surface quality or restrict material flow. Secondary additives contribute additional functional or aesthetic properties, including pigments for color, flame retardants for safety, and anti-static agents for specialized applications.
Chapter 7: Advantages and Disadvantages of Rotational Molding
The concept of rotational molding is straightforward, but achieving high-quality results can be challenging for some manufacturers. Despite its complexities, rotational molding is highly valued for its advantages over other molding methods. With proper design and settings, both manufacturers and end-users can benefit from the following:
- Uniform wall thickness: A consistent wall thickness, on all sides, edges and corners, increase the part's durability. With proper rotational speed and cooling cycles, a uniform wall thickness may be achieved, even on producing thick-walled parts. The corners and edges produced are thicker with rotational molding when compared to blow molding, which stretches the molten material in those areas.
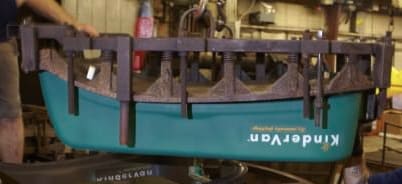
- Ease of producing double-walled parts: Double-walled parts are easily made without the need for secondary processing such as welding and joint fabrication. The parts produced have seamless edges, which eliminates the stress points, resulting in increased durability.
-
Inexpensive tooling: Rotational molding molds do not need to withstand high pressures, allowing them to be manufactured from cost-effective materials like aluminum. This reduces the investment required for tooling, especially beneficial for short production runs.
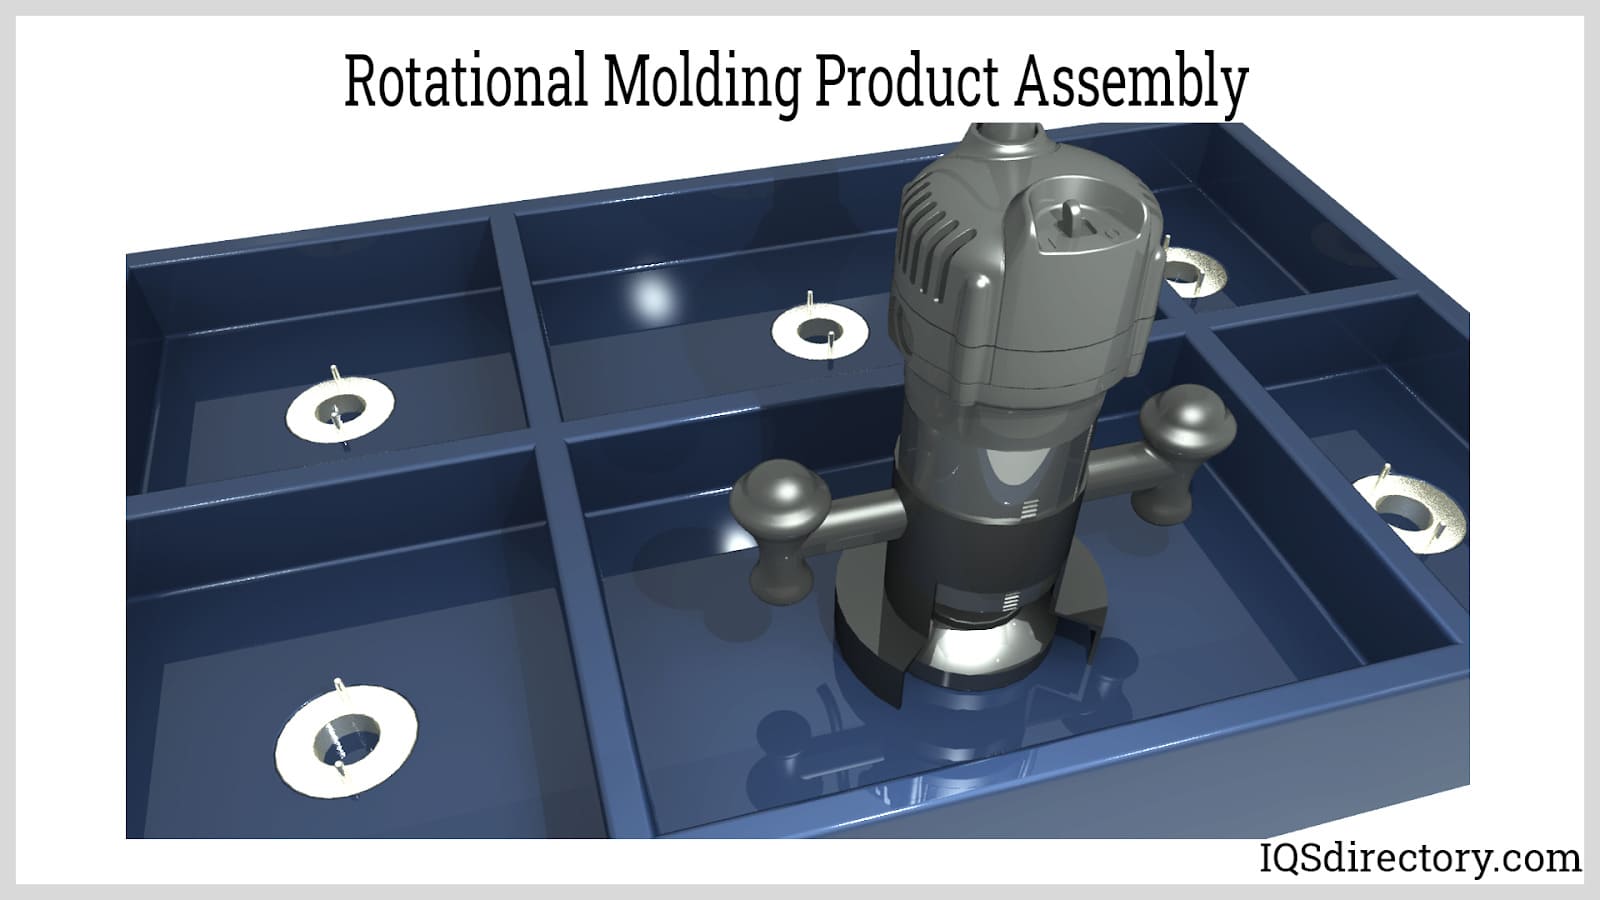
- Flexibility of production: Different parts can be molded in a single machine at the same time. With some rotational molding equipment that has independent arms, it makes tool management easy; one mold may be scheduled for maintenance activities while the other molds are in use.
- Larger parts can be produced: Rotational molding makes the production of large hollow parts possible. The only limitation is the size of the heating and cooling chambers.
- Less downstream processes required and minimal waste in production: The part manufactured in rotational molding is only a single part. Hence, it is not required to undergo trimming or stripping steps. Rotational molding also generates less wastage of polymer resin in the form of runners, sprues, and cut-offs.
-
Ease of Decoration: Designers can effortlessly add textures and symbols to the surface of the tooling, allowing for seamless incorporation of decorative elements.
As rotational molding offers many advantages over other types of molding processes, it does not mean that it is the best for all manufacturers. Here are some disadvantages of this process:
-
High Cycle Times and Costs: Rotational molding can be less suitable for high-volume production due to its lengthy cycle times. The process involves slow rotation during heating to melt the material and a gradual cooling phase for both the part and the mold, which extends the overall molding cycle. While cooling systems like water or air can help, they add to the overall cost.
Finally, the process still requires manual steps, such as demolding, due to the limited automation options available. This necessity for manual intervention increases the overall operational costs.
- Limited material options: Few polymers qualify as the raw material for this process since they require being converted into powdered form to be processed successfully. Polymers other than polyethylene are costly and difficult to grind. Also, this process requires the polymer to have high thermal stability, which limits poly-based resins to be selected.
- Shorter service life of the tool: Since it is only made from thin and soft metal, the tool must be replaced after several mold cycles to ensure the quality of the parts being produced due to a lack of repeatability.
- Some details and designs are difficult to mold: Uniform thickness on a large flat surface is difficult to mold due to the flow of the resin. Also, rotational molding machines are not capable of molding high-tolerance parts and sharp edges; high-pressure molding may be considered.
Chapter 8: Applications of Rotational Molding
Rotational molding is widely used across industrial, commercial, and consumer markets because it enables the production of hollow, seamless, and highly durable plastic components. Its design flexibility, uniform wall thickness, and ability to mold complex shapes make rotomolding ideal for products that must withstand impact, weather exposure, chemicals, or repeated use. Common applications span industries such as manufacturing, automotive, agriculture, healthcare, marine, construction, and recreation. Notable products manufactured using rotational molding include:
-
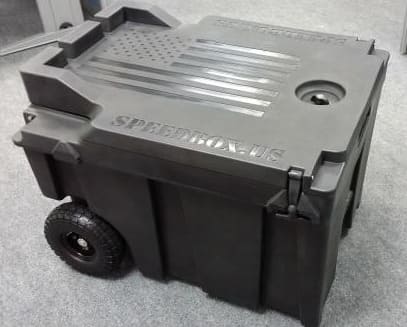
Material handling equipment such as heavy-duty crates, stackable pallets, bulk containers, and insulated storage boxes, which benefit from rotomolding’s strength, impact resistance, and seamless construction
- Plastic storage tanks, gallon drums, and carboys designed to safely contain small to extremely large volumes of water, chemicals, fuels, and industrial liquids
-
Medical and laboratory equipment such as spine boards, oxygen masks, protective housings, and squeeze bulbs that require smooth surfaces, durability, and easy sanitization

- Agricultural and gardening products used in planting and material transport, including pots, troughs, compost bins, planters, and garden carts designed for outdoor exposure and repeated handling
- Sanitation and waste management products such as refuse containers, trash cans, septic tanks, and wastewater components that demand corrosion resistance and long service life
-
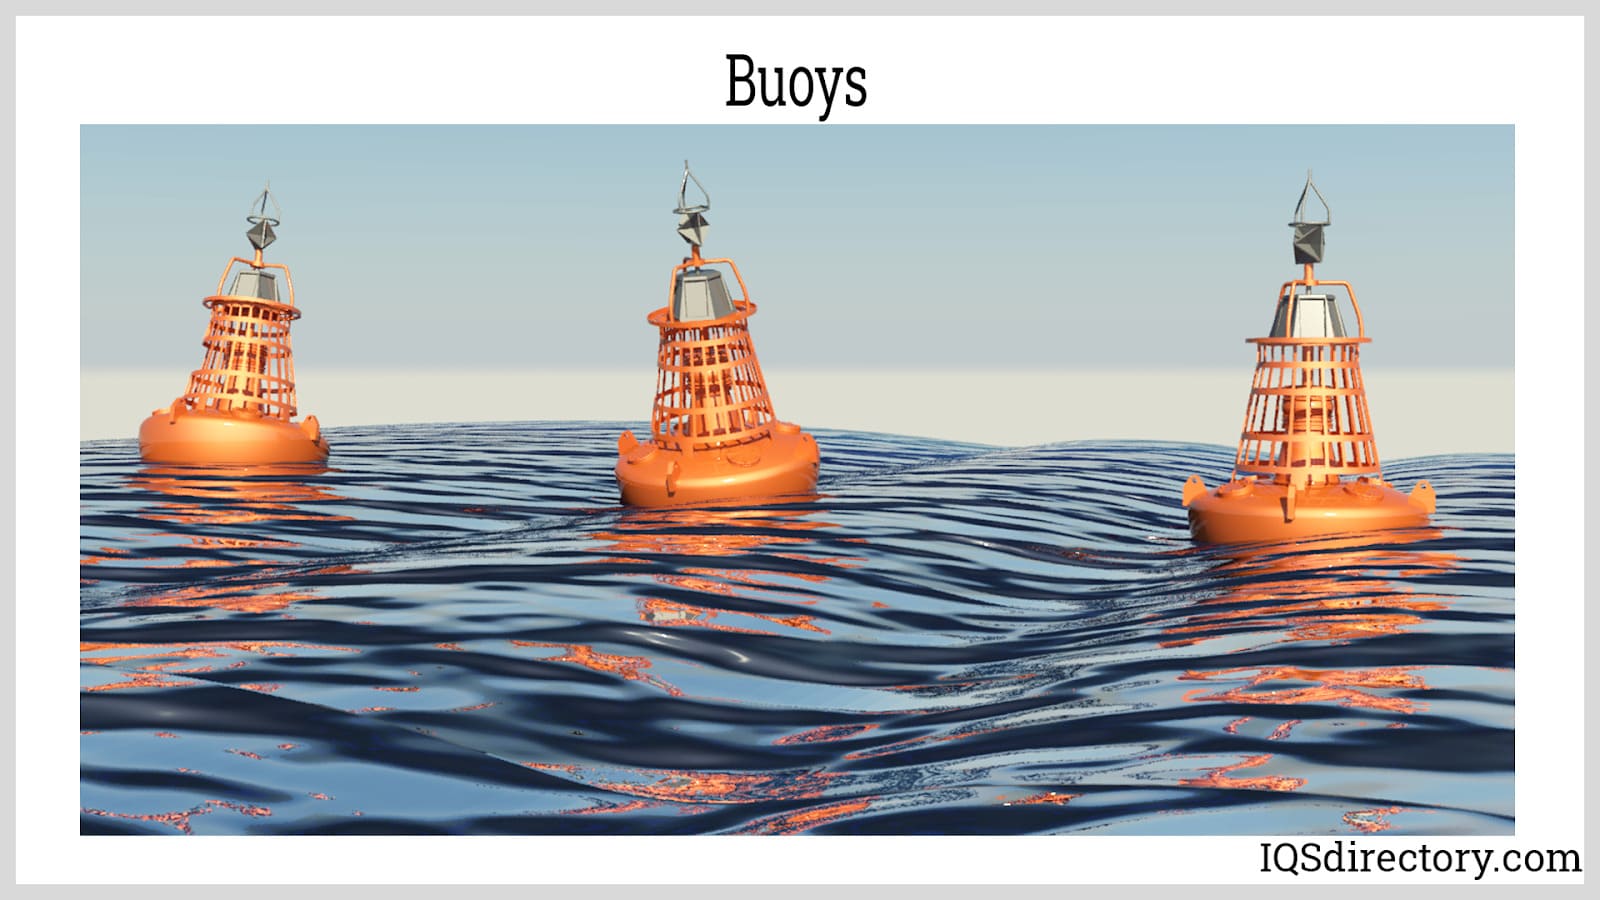
Marine and water recreation equipment such as rowing boats, canoes, buoys, kayaks, and floating devices produced using rock-and-roll rotational molding machines for long, hollow shapes
- Roadway and construction safety products including traffic cones, barricades, barriers, and impact-resistant signage commonly used on highways and job sites
- Toys, playground structures, and sporting equipment such as doll components, playground slides, gym equipment housings, balls, and pool flotation devices
- Small-scale shelters and enclosures, including portable toilets, storm shelters, testing booths, and temporary housing units that require structural integrity and weather resistance
Summary:
- Rotational molding is a plastic casting technique that produces a hollow, seamless, and double-walled part by heating a powdered resin in a hollow mold tool while being slowly rotated and cooled to solidify. This process started hundreds of years ago, was popularized in the mid-20th century, and is still developing. This process has a variety of applications.
- The rotational molding equipment consists of a mold, ovens, and a cooling chamber. The type of rotary molding machine is distinguished by the direction in which the mold travels according to the sequence of the process.
- The types of rotational molding equipment are clamshell machines, turret machines, shuttle machines, vertical wheel machines, rock and roll machines, and open-flame machines.
- Loading is the first step wherein the fine, homogenized, and dried powdered resin is placed in a mold coated with a mold release agent. The resin is heated while being slowly rotated in a bi-axial direction until it is molten and covers the entire tool. The molded part and the entire mold are gradually cooled by convection to room temperature, wherein they can be safely removed.
- Critical parameters of the rotational molding process are heating time, cooling rate, and rotation ratio. These settings determine the mechanical properties and dimensional quality of the parts to be produced.
- The polymer resin must have high thermal stability, flow easily in its molten state, and have antioxidant groups in the molecular structure. The resin must be easily ground to powdered form. Polyethylene is the most commonly used polymer.
- The advantages of rotational molding are the creation of parts with uniform wall thickness, inexpensive tooling, the flexibility of production, less downstream process, and less wastage of the resin. Large and double-walled parts are also easily created.
- The disadvantages of rotational molding are a high cycle time attributed to long heating and cooling cycles, limited material options, short tool life, and difficulty of molding some details.