- 4 leading manufacturers
- 19 additional suppliers
- 15 states and provinces
- 18 related categories
- 11 guide sections
Metal Etching Manufacturers and Companies

IQS Directory provides a detailed list of metal etching companies and suppliers. Find metal etching companies that can provide metal etching services to your specifications. Peruse our website to review and discover top metal etching companies with roll over ads and complete product descriptions. Connect with the metal etching companies through our hassle-free and efficient request for quote form. You are provided company profiles, website links, locations, phone numbers, product videos, and product information. Read reviews and stay informed with product new articles. Whether you are looking for reverse metal etching, roll to roll metal etching, or galvanized metal etching, IQS is the premier source for you.
Suppliers located in CA, MN, IL +12 more states
Contents (6 sections)
Leading Metal Etching Manufacturers
Showing all 4
| Placement No. | Manufacturer | Location | Contact | Actions | |
|---|---|---|---|---|---|
| 1 | MET Manufacturing Group, LLCThe MET Manufacturing Group, LLC process offers many technical & financial advantages in manufacturing various flat metal components. Try this precision etching, non-mechanical process for competitively priced, burr & stress free sheet metal products, up to 62 mil (.062”) thick. Our photo-chemical machining process is also known as photo-fabrication, photo etching, chemical milling & acid etching. | Mishawaka, IN | |||
| 2 | EtchitEtchit is your high-quality solution for custom-manufactured precision metal parts and components. We use photochemical machining to make products for such industries as aerospace, audio, automotive, computer, circuit board, decorative and fastener. Does your product need photo etching processes? | Buffalo, MN | |||
| 3 | VACCO Industries, Inc.VACCO is the industry leader of Photo Chemical Etching of metal & polyimide components and devices. We specialize in Stainless steel, Titanium, and Copper, but work with a variety of different materials. We have over 60 years of experience in Chem Etching, and we offer Micro Laser Cutting & Welding, and Diffusion & Adhesive Bonding services along with an extensive range of value-added services. Whether your application is large or small, VACCO can assist you from prototype to production. | South El Monte, CA | |||
| 4 | Great Lakes Engineering, Inc.Great Lakes Engineering is a trend setting manufacturer of surface mount stencils, precision laser cut parts, and photo chemical etched parts. We work with a wide range of materials, including Stainless Steel, Copper, Brass, Titanium, Nitinol, Nickel, Kovar and many others. We do not work with glass, plastics, or aluminum. Our specialty is working with very thin materials ranging from .001” to .030” thick. We can offer a wide range of capabilities and materials to meet your needs. | Maple Grove, MN |
Claim your Page One Spot
Leading metal etching manufacturers are listed first on this page, each with a website preview and a Request a Quote button on its row.
Additional Metal Etching Companies
The category’s other metal etching companies are listed on their own page, with location, phone and website where each supplier provides them.
View 19 Additional Metal Etching CompaniesDo not see your company listed in Metal Etching?
Engineers and buyers use this page to find metal etching suppliers. Add your company to the Metal Etching listings so they can find you too.
List Your Company- Listed in the Metal Etching directory
- A profile page for your company
- Buyers contact you directly
Metal Etching Industrial Manufacturing Guides
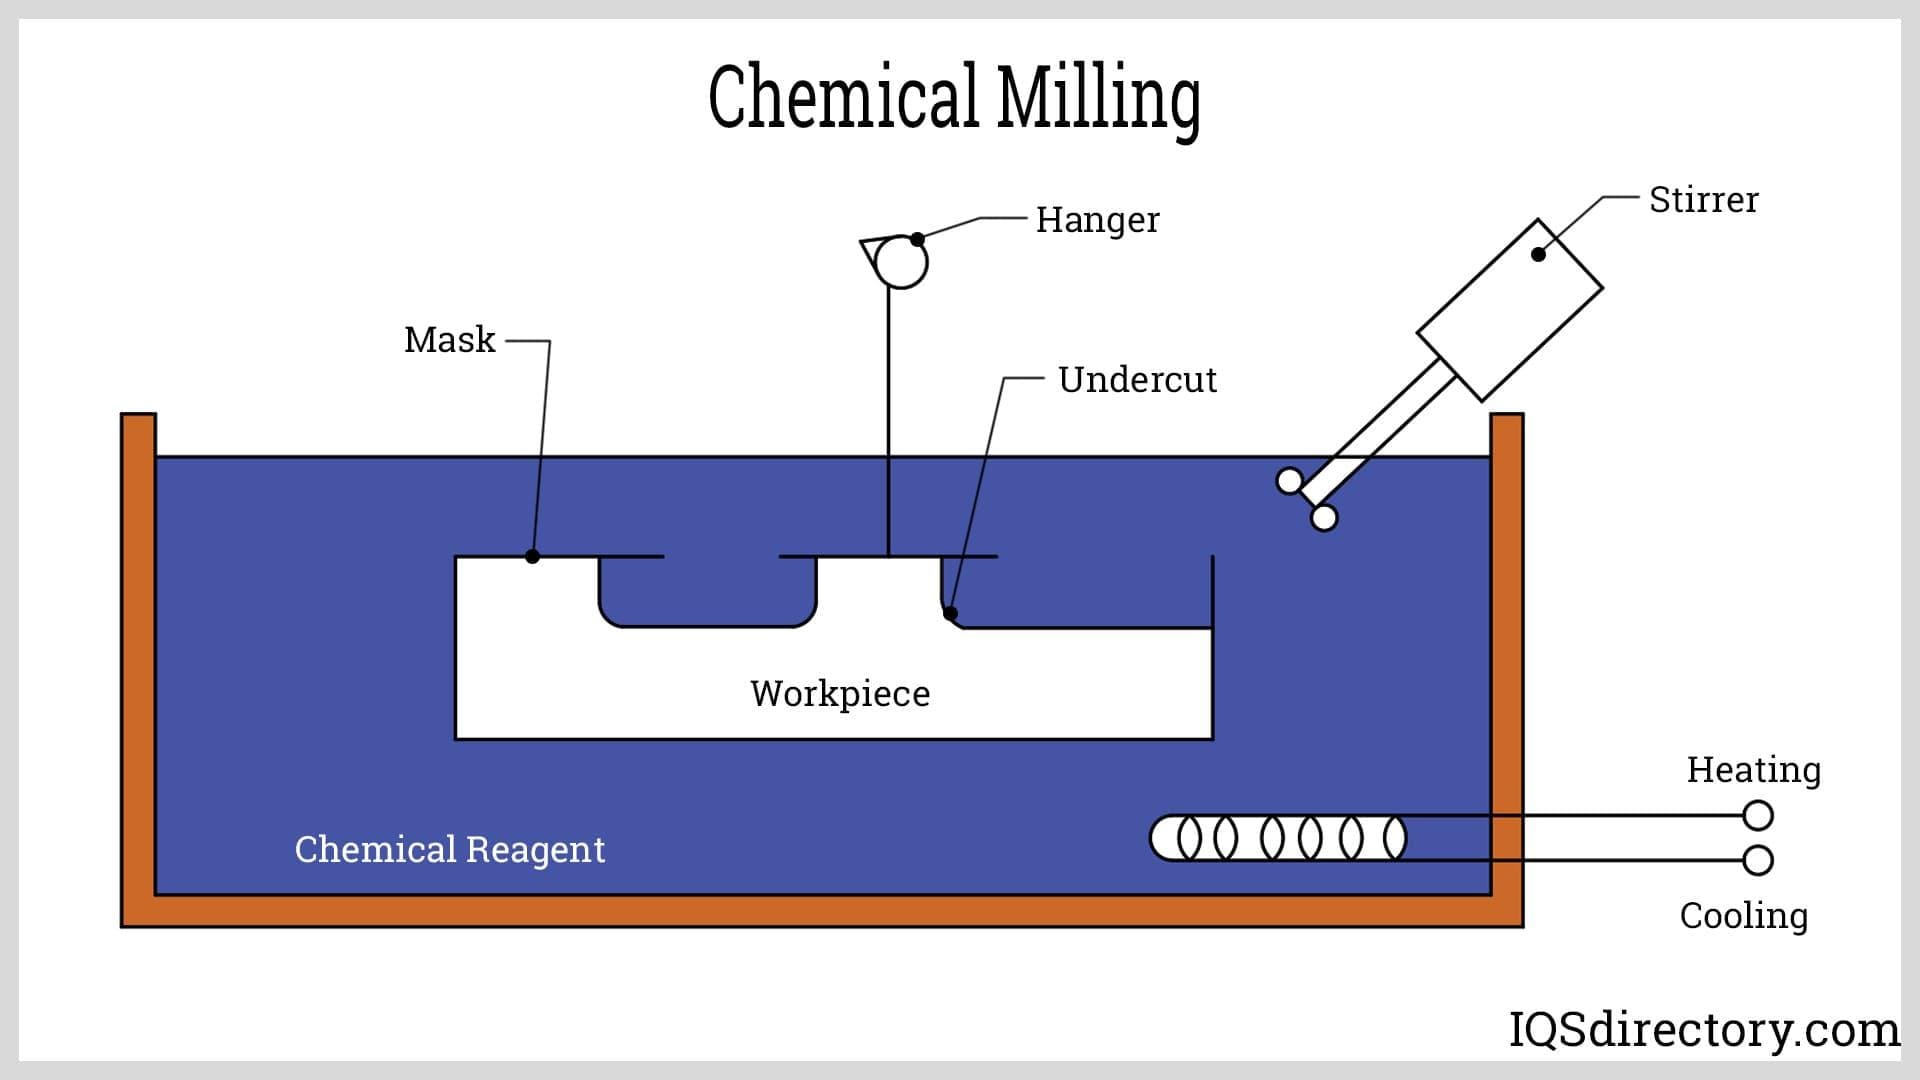
Chemical Milling: Types, Uses and Products
The contents of this article will provide you with everything you need to know about chemical milling and its use. You will learn: What is Chemical Milling?…
7 chapters, the longest in this category
Quick Answers
- How many metal etching manufacturers are listed on IQS Directory?
- 4 leading manufacturers and 19 additional suppliers.
- Where are metal etching manufacturers located?
- The listed suppliers are in 15 states: California (6), Minnesota (3), Illinois (2), Connecticut (1), Florida (1), Indiana (1), Louisiana (1), Massachusetts (1), and 7 more.
- How do I get quotes from metal etching suppliers?
- Select suppliers in the table and choose Request Quotes. IQS reviews your request and forwards it to every supplier you select.
Metal Etching
Metal etching, also known as metal engraving, is the process of creating grooves, fine lines, holes, markings, and detailed patterns on metal sheets and precision components. This manufacturing method supports decorative, industrial, architectural, and identification-related applications, making it valuable for companies that need both appearance and performance. Industries that rely on metal etching include jewelry, furniture, architecture, music, art, healthcare, woodworking, aerospace, electronics, defense, energy, medical device production, and OEM part manufacturing. In decorative work, manufacturers may darken etched lines so logos, nameplates, instrument panels, and branded surfaces stand out more clearly. In industrial settings, metal etching can also help parts meet tight weight, thickness, and tolerance requirements by removing a controlled layer of material through chemical, photochemical, laser, or mechanical methods.
History of Metal Etching
The etching process, with relatively few changes to its core principles over centuries, has been used across industries ranging from micro-electromechanical systems and circuit fabrication to aerospace hardware, printed components, instrument panels, and missile production. While its present-day role in precision manufacturing may appear highly modern, the roots of metal etching go back to ancient artistic and decorative practices.
In its earlier forms, etching was developed for artistic and ornamental purposes, especially on softer metals like copper and zinc, and later on harder metals such as steel with the help of stronger acids. Armor, firearms, plates, cups, ceremonial objects, and tools were often etched to add decorative detailing, patterns, identity marks, and visual depth. Over time, those same techniques opened the door for industrial marking, metal signage, and precision surface treatment.
Progression of Etching By the 16th century, etching had a major influence on printmaking in Germany and other parts of Europe. In that process, a metal plate was coated with an acid-resistant material such as wax. Artists then scratched through the coating with an etching needle to reveal the underlying metal and form a design. The plate was immersed in acid, which cut into the exposed areas to create recessed lines and images. Once inked, these plates could be used repeatedly for printing, helping expand visual communication, technical illustration, and publishing during the rise of the industrial age. During this period, the metal etch process also emerged as an alternative to metal engraving, a widely used method for carving patterns into metal. Chemical etching became popular for marking artillery and cannons with trajectory and identification data because etched markings were long-lasting and readable. Milling and etching were further applied to daggers, shovels, tools, metal panels, and specialty hardware where consistent markings were needed. A major advancement in metal etching took place in the 18th century when Swiss botanist John Senebier observed that certain plant resins hardened after exposure to light and became insoluble in turpentine. This discovery later supported the development of photochemical etching, although it was first explored in photography. A light-sensitive or light-resistant resin could be applied to metal, exposed in selected areas, and then used to create detailed patterns and impressions on metal plates with greater repeatability than purely hand-driven techniques. During the 1900s Modern photochemical machining began in 1927 when Aktiebolaget Separator, a Swedish company, developed and patented a process for producing edge filters. The method saw broader adoption during World War II, when manufacturers needed efficient ways to etch hard metals from both sides and produce thin sheet foil components with tight dimensional control. Later advances in etching chemistry, masking systems, photoresist technology, and process automation helped make micro-fabrication possible, supporting the expansion of the electronics, aerospace, telecommunications, and information technology sectors.Advantages of Metal Etching
Regardless of the method selected, metal etching offers a wide range of advantages when compared to many conventional machining and cutting processes. Whether the goal is to create stencils, metal stamps, identification tags, decorative panels, precision screens, filters, or semiconductor-related components, metal etching remains a versatile solution for manufacturers that need fine detail without heavy tooling.
One of the biggest benefits is its compatibility with a broad selection of materials, including both hard metals and soft plastics in certain marking or surface-finishing applications. The process does not usually introduce the same kind of deformation, internal stress, or burr formation associated with punching, drilling, or aggressive machining. Because of that, etched parts often need less deburring, polishing, or secondary finishing, which can help improve throughput and shorten production cycles.
Metal etching also preserves the original properties of the substrate, including hardness and overall dimensional stability. For engineers and buyers comparing production options, that can make etching attractive for lightweight parts, intricate features, and repeatable fine-detail work. Manufacturers also value the speed of design revisions, the ability to create complex geometries, and the reduced dependence on hard tooling. If your team is comparing metal etching vs. engraving, photo etching vs. stamping, or chemical milling vs. CNC cutting, the answer often depends on tolerance needs, material thickness, order volume, and finish requirements.
Design for Metal Etching
In metal etching, cuts of different depths can be achieved, and the resulting depth is determined by how long the metal remains exposed to the etchant bath or processing medium. The etching rate is commonly measured by comparing target depth to exposure time, but real-world production also depends on chemistry, masking, material response, and part geometry.
Many variables affect etch rate and overall cut quality, including the material type, sheet thickness, bath temperature, agitation, mask quality, and the composition and concentration of the etchant. For that reason, many manufacturers conduct test runs before full production begins. These trials help fine-tune process settings so the desired depth, edge profile, line width, and dimensional accuracy can be achieved with repeatability. Buyers often ask: how deep can a part be etched, what tolerances are possible, and which metals respond best? Those answers are usually tied to design intent and process selection.
The Metal Etching Process
What is a standard metal etching process? In most industrial environments, the process follows a sequence designed to support surface preparation, controlled material removal, and consistent part quality for components, tags, nameplates, thin-gauge parts, and decorative surfaces.
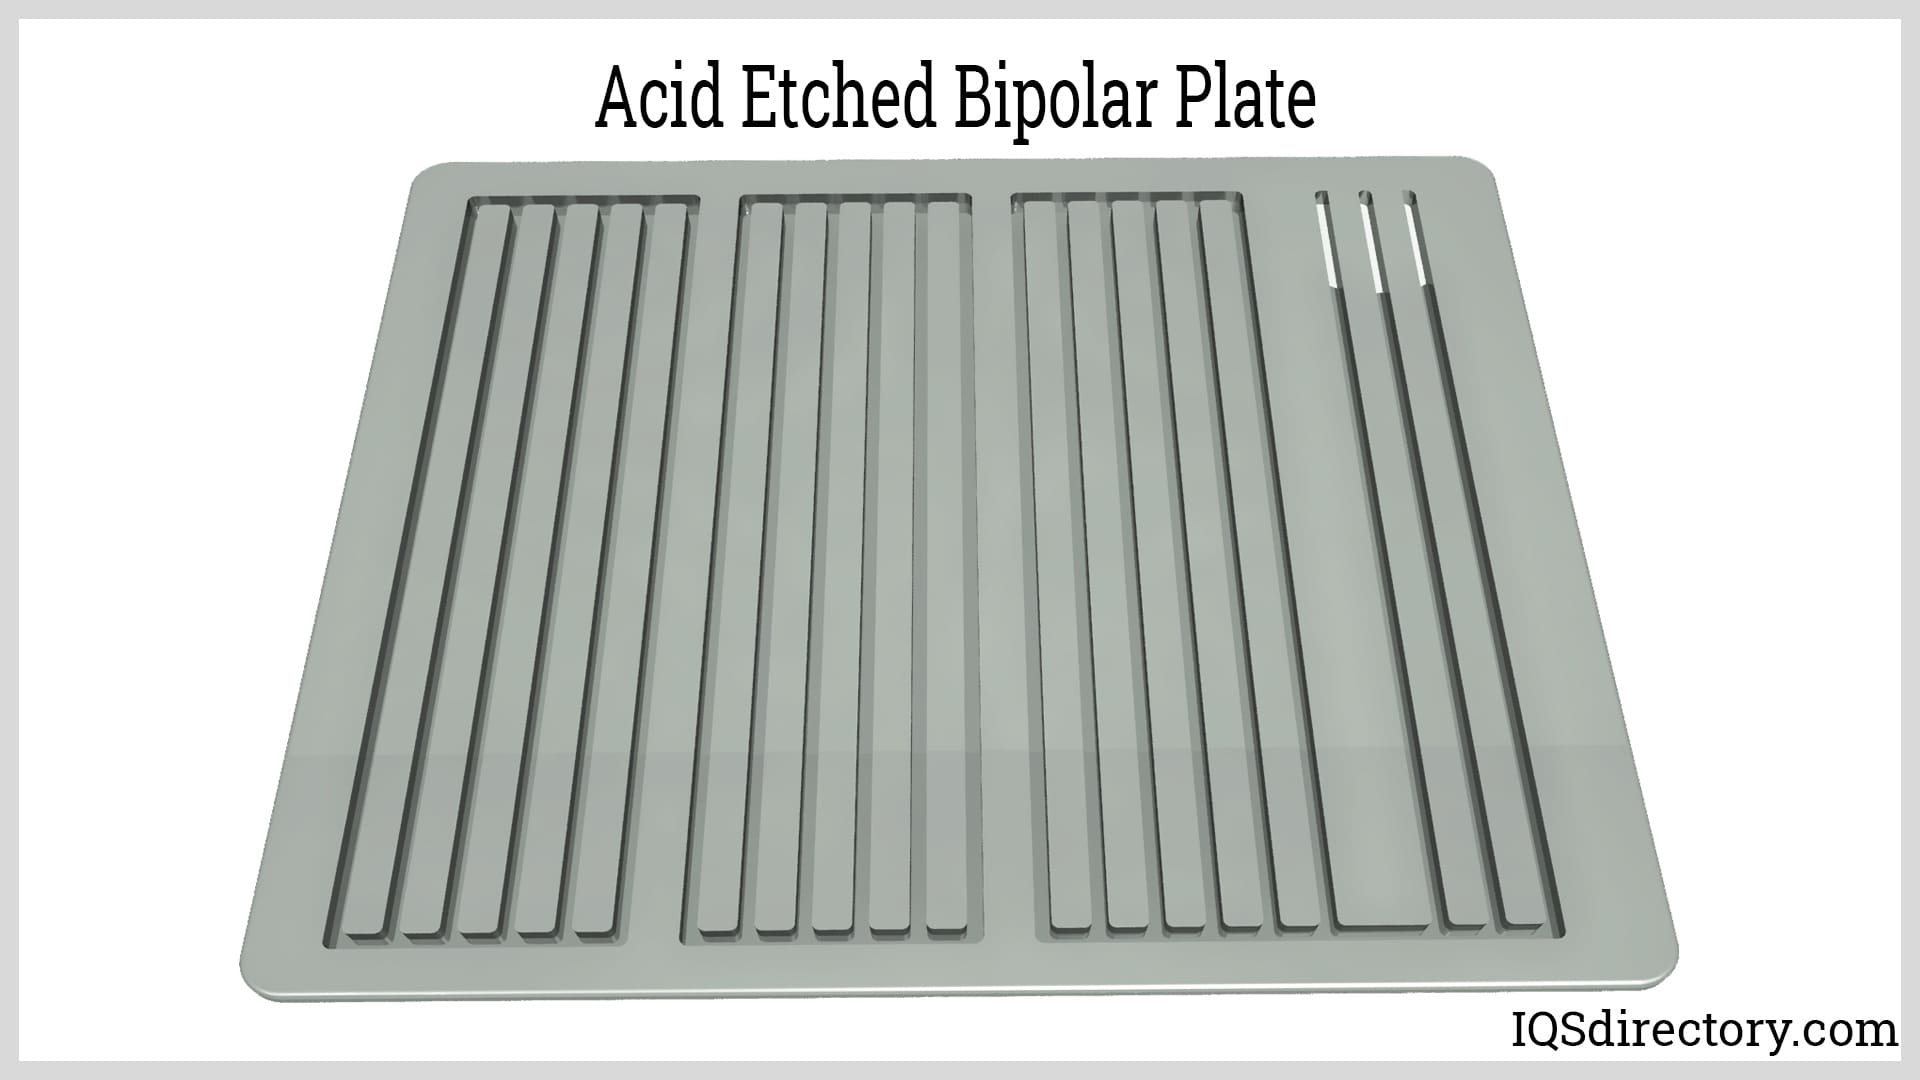
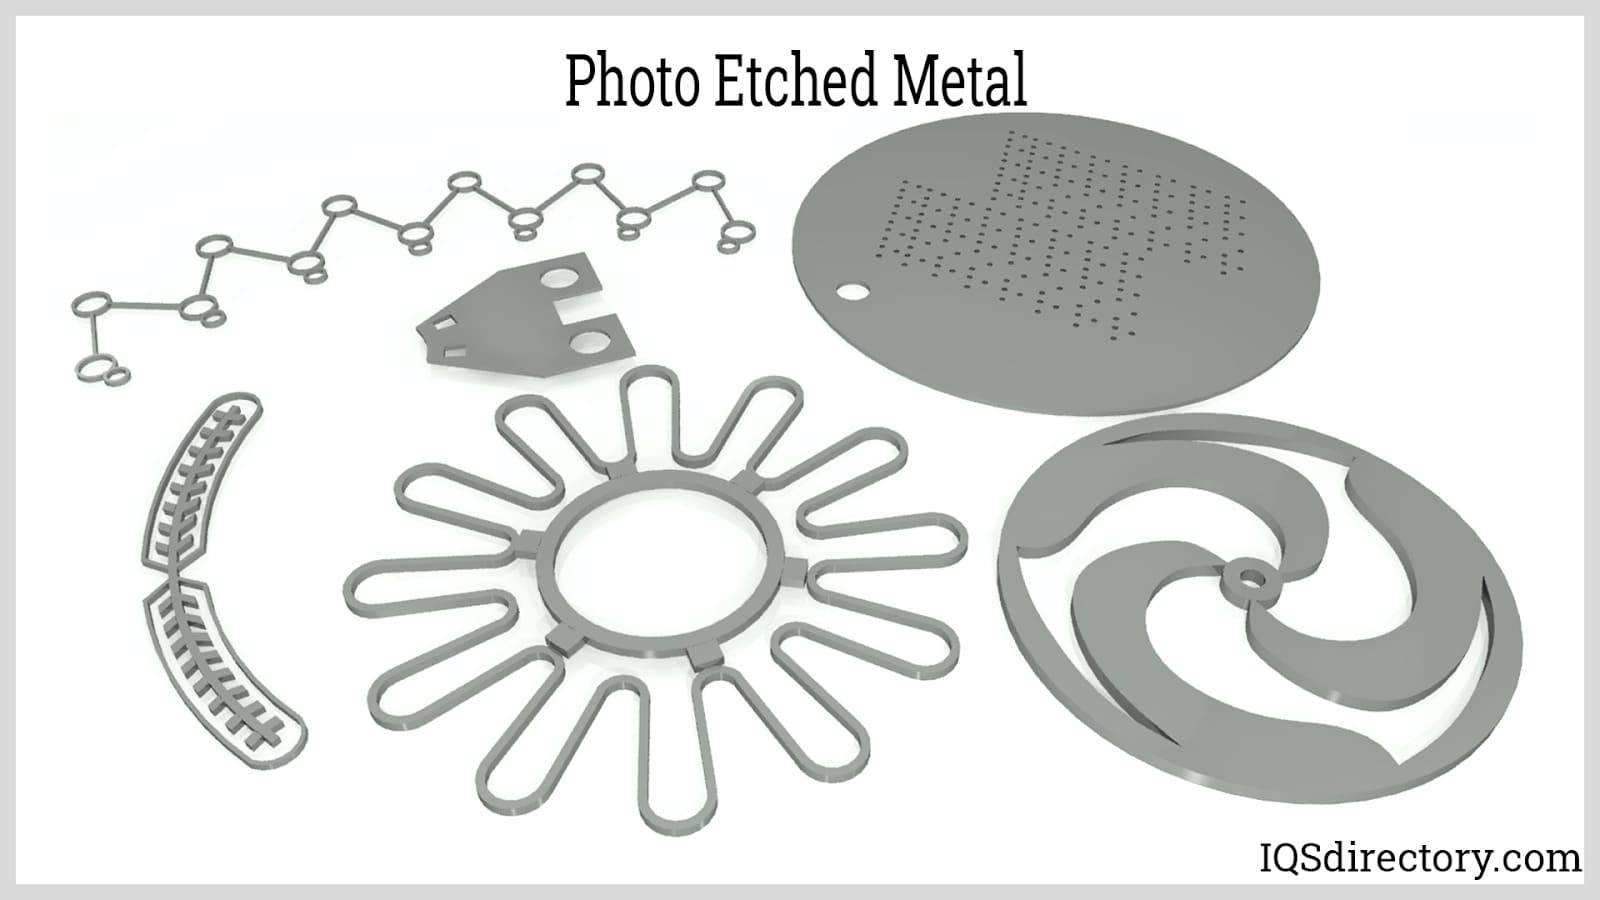
Cleaning Surfaces The process begins with thorough surface cleaning to prepare the metal for etching. All contaminants must be removed because even small traces of residue can interfere with the reaction and create uneven line quality or incomplete etching. Solvents, de-oxidizing compounds, alkaline cleaners, and rinses are commonly used to strip grease, oils, primers, shop soils, ink marks, and handling residues from the substrate. Applying Masking Agent In industrial applications, maskants such as isobutylene-isoprene copolymers, neoprene elastomers, photoresist coatings, films, tapes, or other chemical-resistant materials are used because they can withstand exposure to the etching chemistry. The masking material is patterned onto the metal to define the required design, holes, channels, logo, lettering, or cut area. Depending on the application, masking may be applied by dipping, flow coating, lamination, or photo-imaging. Immersion in Etchant At this stage, the metal etching takes place. The masked metal part is exposed to a chemical solution such as ferric chloride or another selected etchant for a controlled amount of time. Exposure time, solution strength, bath temperature, agitation, and material type all influence width, depth, edge quality, and repeatability. This stage is where manufacturers balance production speed with precision. Removing the Mask In the final stage, often called demasking, the remaining masking compound and reaction by-products are removed to reveal the finished pattern. Cold water rinses, neutralizing steps, and specialized cleaning baths may be used to remove chemical residue. Depending on the process, the mask may be stripped chemically or removed manually, leaving behind the final etched profile ready for inspection, finishing, assembly, or shipment.Metal Etching Images, Diagrams and Visual Concepts
Types of Metal Etching
Materials Used in Metal Etching
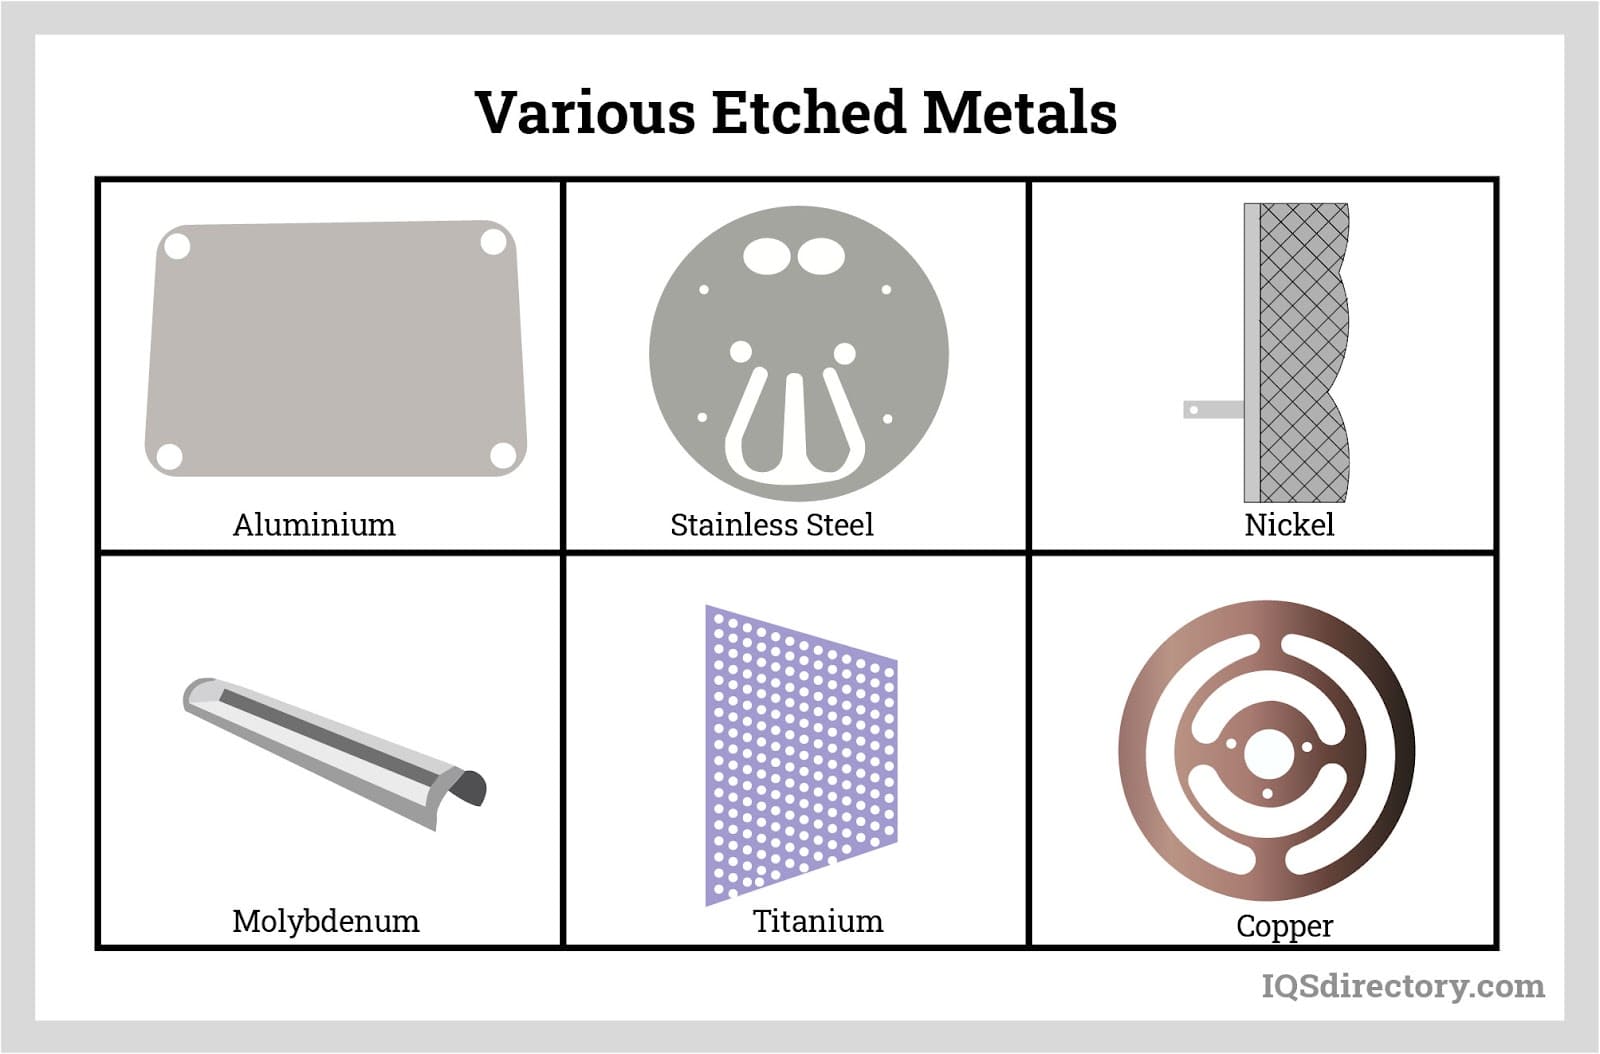
Metal etching is a highly adaptable process, and nearly all metals can be processed using chemical milling, photo engraving, photochemical machining, or mechanical etching. Frequently used materials include aluminum, brass, copper, beryllium copper, nickel, nickel silver, carbon steel, and stainless steel. Material choice often depends on conductivity, corrosion resistance, hardness, weight, appearance, and the required part function.
Frequently used corrosive chemicals, or etchants, include ferric chloride, ferric nitrate, nitric acid, copper sulfate, hydrochloric acid, citric acid, nitroxyl (HNO), and phosphoric acid. The selected etchant depends on the metal, the target surface finish, the required etch depth, and production efficiency. Manufacturers evaluate chemistry carefully because the wrong combination can slow throughput or reduce feature accuracy.
Machinery Used with Etching
Manufacturers use a range of machines and support systems to create accurate cuts, patterns, and markings during metal etching and related finishing processes.
Milling and grinding machines are often used to produce specific etched finishes, especially on larger sheets used in architectural panels, decorative surfaces, signage, and furniture components.
Lathes and CNC machines with fine tips are used to process different material shapes and profiles, including straight surfaces, curved parts, and custom metal forms that require repeatable detail.
For highly detailed or small-scale work, such as jewelry, firearms, musical instruments, identification tags, and specialty decorative components, hand engraving tools are still used where artisan control or one-off customization is preferred.
Modern engraving machines are relatively easy to operate and can process metals, glass, and plastics. These systems often include a stylus or marking tool, a controller, and a stable work surface. Diamond styluses are commonly selected for harder materials. In production settings, automation helps improve consistency, especially when manufacturers need repeatable logos, serial numbers, labels, or fine surface graphics.
Things to Consider When Choosing Metal Etching
If you are deciding whether metal etching is the right solution for your application, compare your part requirements with the capabilities of the process. Consider the level of design precision you need, the allowable tolerance range, the material type, the desired cut depth, your industry standards, and whether you need decorative detail, functional geometry, part marking, or lightweight material removal.
The best way to make an informed decision is to speak with a qualified manufacturer about your production goals, budget, and timeline. Buyers often search phrases like metal etching companies near me, custom metal etching services, photo etched parts, or precision chemical etching manufacturers when evaluating suppliers. Look for companies with relevant experience, process knowledge, strong communication, and the ability to match your design intent. Start by comparing the companies listed above and ask about materials, tolerances, turnaround time, prototyping options, repeat production, and finishing support.
Variations of Metal Etching
Widely used metal etching methods include laser etching, electro discharge machining, chemical milling, chemical machining, acid etching, photochemical etching, mechanical milling, and both wet and dry etching. Manufacturers may also turn to stamping, laser engraving, or water-jet cutting for selected metal parts. These methods are generally faster and more precise than hand engraving, though the best option depends on geometry, production volume, finish, and cost targets.
Laser Etching Able to create very fine, clean lines on surfaces with little need for secondary finishing, making it useful for branding, part marking, and precision decorative work. Electro Discharge Machining (EDM) Another method related to fine metal processing that can achieve close tolerances. During the process, the metal part is exposed to streams of controlled electromagnetic discharge. Any resulting marks or burrs may be smoothed and polished after processing. Chemical Milling/Chemical Machining Manufacturers begin chemical milling by covering a metal sheet in a masking compound. That inert masking protects selected areas from the etchant. The uncovered sections are then exposed to the chemical solution, which reacts with the material and removes it through dissolution. This process is often chosen for thin-gauge parts, lightweight components, and intricate patterns that would be difficult to machine conventionally. Acid Etching Very similar to chemical milling, acid etching is used to create grooves, images, lines, holes, lettering, and patterned surfaces. Manufacturers can achieve precise lines and specific depths when chemistry, exposure time, and masking are controlled correctly. The process begins by stripping the sheet metal of oils, organic matter, and chemical residues using cleaners that prepare the surface without damaging the finish. Next, a maskant is applied to the surface. Depending on the application, manufacturers may use tapes, paints, elastomers, plastics, or photoresist materials. They cut or expose the pattern that defines the area to be etched, then remove the masking from those selected sections before applying the reagent. Finally, after the acid reaches the required depth, manufacturers strip away both the reagent and the remaining maskant to reveal the finished part. The length of chemical exposure depends on the target groove depth, line width, and the strength of the etching chemistry. Photochemical Machining To begin the photochemical machining process, manufacturers print the desired part geometry onto photographic film. They then choose a metal sheet, cut it to size, apply photoresist, place it between film layers, and vacuum seal the assembly. UV light hardens the selected portions of the photoresist. The unhardened resist is washed away, leaving exposed areas ready for the etchant. Once sufficiently etched, the part is neutralized, rinsed, and finished. This method is widely used for detailed, burr-free components in electronics, shielding, filters, medical devices, aerospace, and precision assemblies. Mechanical Milling A common alternative used to metal etch or engrave, mechanical milling relies on a lathe or CNC machine with fine tips capable of processing many materials and dimensions, including straight and curved surfaces. Computer control directs the cutter or laser for accurate pressure, speed, and movement, resulting in precise images and clean lines. This method delivers consistent results, though tooling costs and machine maintenance can be higher than in chemical or photochemical processes.In addition, metal etching processes are generally categorized into wet and dry etching.
Depending on the desired configuration, manufacturers select either wet or dry etching based on the type of etchant, the substrate, and the feature definition required. Chemical etching is similar to chemical milling, though chemical milling is often used when greater depth and higher etch rates are needed.
Etching can be isotropic or anisotropic.
Isotropic When an etchant removes material uniformly in all directions. Anisotropic When an etchant removes material in a more directional, typically vertical pattern.Anisotropic etching may be fully or partially directional. Dry anisotropic etching usually achieves higher aspect ratios and finer resolution than isotropic methods, which is why it is often associated with micro-scale and electronics-related fabrication.
Wet Etching When an etchant is in liquid form, the process is called wet etching. The areas that must be preserved are masked, and the exposed material is removed by the liquid etchant. Lithography is often used before fabrication to define the required pattern and geometry. In wet etching, multiple chemical reactions occur as original reactants are consumed and new by-products are formed during processing. The wet etching process can be simplified in three steps: In the first step, the liquid etchant attaches to the structure that needs to be removed. In the second step, the liquid etchant reacts with the material and the exposed substrate dissolves away. This is often a reduction-oxidation reaction in which the target material is oxidized and then removed. The third step is the diffusion and removal of reaction by-products. When silicon is used to etch anisotropic shapes, common wet etchants include ethylenediamine pyrocatechol (EDP), potassium hydroxide (KOH), and tetramethylammonium hydroxide (TMAH). In isotropic wet etching of silicon, manufacturers may use combinations of acetic acid, nitric acid, and hydrofluoric acid. Etch rate is typically influenced by etchant concentration and process conditions. Dry Etching To achieve a dry metal etch, plasma or gas is used instead of a liquid solution. The material is removed through high-energy particle interaction, chemical reaction, or a combination of both. Dry metal etching is further categorized as physical or chemical. In physical dry etching, the kinetic energy of ions, electrons, or photons removes material from the substrate. In these cases, the particles physically dislodge atoms while the surface material evaporates or is carried away. Chemical dry etching, also called vapor phase etching, uses reactive gases to attack the substrate. Common gases used in dry etch processes include fluorine, tetrafluoro methane, nitrogen trifluoride, sulfur hexafluoride, and chlorine gas. As mentioned earlier, physical and chemical dry etching may also be combined in reactive ion etching. This is one of the most widely used industrial and laboratory techniques because combining both actions allows faster and more controlled etching. The process uses positively charged ions generated from reactive gases. Those ions strike the substrate at high speed and then react chemically with the exposed material.Metal Etching Terms
Common Questions
7 questions
What Industries Commonly Use Metal Etching?
Metal etching is widely used in aerospace, defense, electronics, healthcare, jewelry, architecture, furniture, medical device production, industrial equipment manufacturing, and musical instrument fabrication. It supports both decorative applications and precision part production where accuracy, repeatability, and surface detail matter.
How Does the Metal Etching Process Work?
The process usually starts with cleaning the metal surface, applying a mask or photoresist, exposing selected areas, and then using an etchant to remove unprotected material. After etching, the mask is removed and the part is rinsed and finished, revealing the required grooves, holes, patterns, or markings.
What Are the Main Advantages of Metal Etching?
Metal etching offers precision, speed, clean edge quality, and compatibility with many materials. It avoids burrs, minimizes distortion, preserves hardness, reduces the need for hard tooling, and works well for thin metals, intricate geometries, lightweight parts, and repeat production runs.
What Materials Can Be Processed with Metal Etching?
Common materials include aluminum, brass, copper, stainless steel, nickel, beryllium copper, carbon steel, and nickel silver. Depending on the application, manufacturers may use chemical milling, photochemical etching, or mechanical techniques to process nearly any metal sheet or thin-gauge alloy.
What Are the Main Types of Metal Etching Methods?
Methods include acid etching, chemical milling, photochemical machining, laser etching, electroetching, abrasive blasting, dry etching, reactive ion etching, and vapor phase etching. The best method depends on the substrate, required tolerances, production volume, and whether the part is decorative, structural, or electronic.
What Factors Influence the Depth of a Metal Etch?
Etch depth is influenced by time in the bath, material type, etchant chemistry, temperature, concentration, masking quality, and target geometry. Manufacturers commonly run trials and process checks to dial in the right settings for the desired depth, edge definition, and dimensional consistency.
Why Is Photochemical Machining Important in Modern Manufacturing?
Photochemical machining makes it possible to create burr-free, highly detailed, repeatable parts without adding stress to the metal. It is especially useful for aerospace, electronics, shielding, filters, medical components, and precision nameplates where intricate patterns and tight tolerances are needed.